
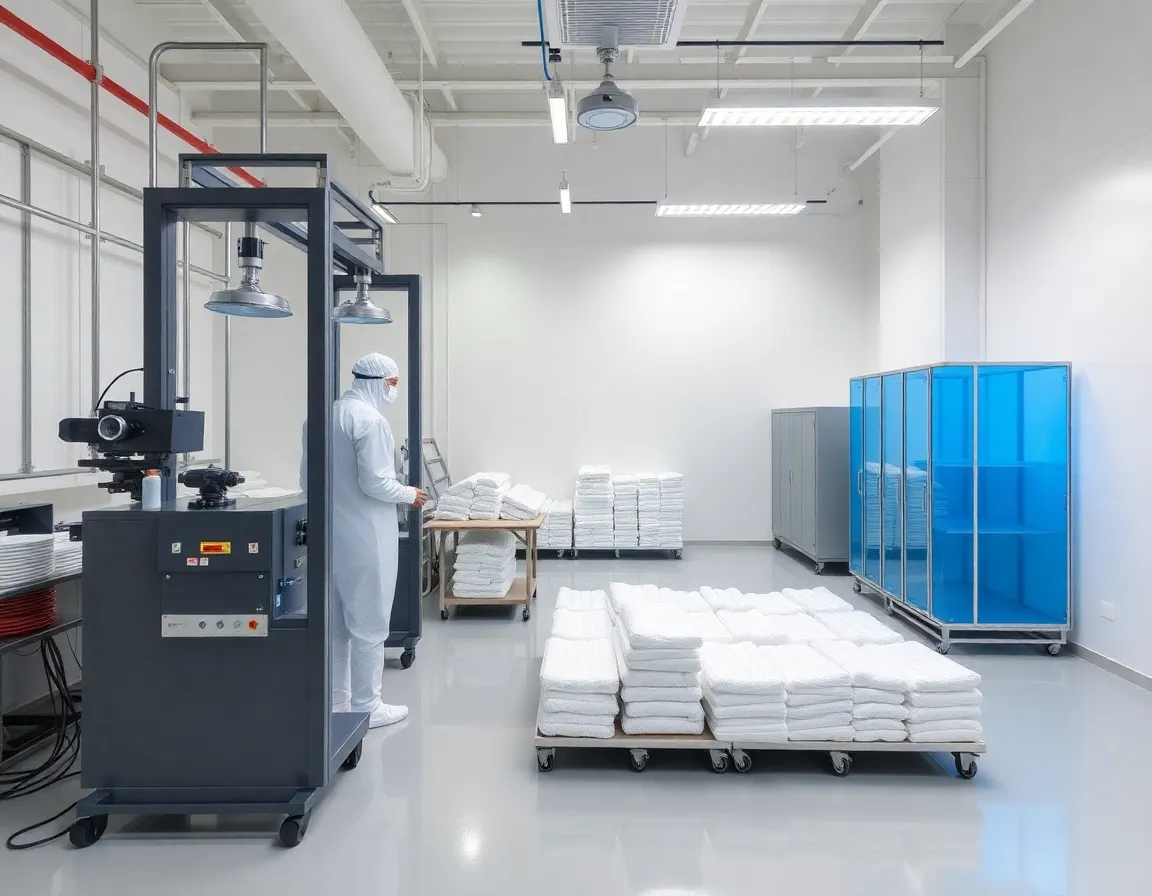
Verständnis der Reinraumformung der Klasse 10000
In der Welt der Präzisionsfertigung wird die Fehlertoleranz in Mikrometern gemessen, und das Vorhandensein einer einzigen mikroskopischen Verunreinigung kann eine gesamte Produktionscharge unbrauchbar machen. Dies ist die Realität für Branchen, die medizinische Geräte, Halbleiterkomponenten und optische Ausrüstung herstellen. Im Herzen dieser strengen Umgebung liegt die Reinraumformung der Klasse 10000, ein spezialisierter Fertigungsprozess, der die Physik des Spritzgießens mit der strengen Disziplin kontrollierter atmosphärischer Bedingungen kombiniert. Aber was bedeutet "Klasse 10000" genau, und warum ist sie zum Goldstandard für die Produktion kritischer Komponenten geworden?
Die Bezeichnung "Klasse 10000" bezieht sich auf die maximal zulässige Anzahl luftgetragener Partikel (0,5 Mikrometer oder größer) pro Kubikfuß Luft. Einfacher ausgedrückt enthält ein Reinraum der Klasse 10000 weniger als 10.000 Partikel aus Staub, Hautschuppen oder anderen Verunreinigungen in jedem Kubikfuß Raum. Zur Einordnung: Eine typische Büroumgebung enthält zwischen 500.000 und 1 Million solcher Partikel pro Kubikfuß. Das Erreichen und Aufrechterhalten dieses Reinheitsgrades erfordert hochentwickelte Luftfiltersysteme (HEPA- und ULPA-Filter), Überdruck, spezielle Reinraumbekleidungsprotokolle und kontinuierliche Umweltüberwachung. Bei der Anwendung auf das Spritzgießen verwandelt dieser Reinheitsgrad einen Standardfertigungsprozess in ein hochkontrolliertes wissenschaftliches Verfahren.
Die Wissenschaft der Reinheit: Warum Kontamination der stille Killer ist
Um zu verstehen, warum Reinheit beim Reinraumspritzgießen so wichtig ist, muss man sich zunächst der Verletzlichkeit der hergestellten Produkte bewusst sein. Bei medizinischen Anwendungen beispielsweise muss ein gespritzter Katheter oder ein implantierbarer Sensor eine makellose Oberfläche aufweisen. Jedes Partikel, das während des Spritzgießprozesses in das Polymer eingebettet wird, kann als Keimzentrum für Bakterienwachstum dienen. Ähnlich kann in der Halbleiterfertigung ein einzelnes Staubpartikel, das in einem spritzgegossenen Steckverbinder eingeschlossen ist, elektrische Kurzschlüsse verursachen und zu katastrophalen Geräteausfällen führen. Die Folgen von Kontamination sind nicht nur kosmetischer Natur; sie sind funktional, sicherheitskritisch und finanziell verheerend.
Die Quellen der Kontamination beim herkömmlichen Spritzgießen
Kontamination in Standard-Spritzgießanlagen stammt aus mehreren Quellen. Die offensichtlichste ist luftgetragener Partikel—Staub, Fasern aus Kleidung und Hautzellen, die von Bedienern abgegeben werden. Weniger offensichtliche Quellen sind jedoch Maschinenschmierung (Hydrauliköle und -fette, die auf die Formoberfläche migrieren können), Rohstoffhandhabung (Polymerpellets, die statische Aufladung sammeln und Staub anziehen) und Sekundäroperationen (Entgraten oder Verpacken, das Partikel einbringt). In einer Umgebung der Klasse 10000 wird jede dieser Quellen systematisch neutralisiert. Luft wird kontinuierlich durch HEPA-Filter umgewälzt, Bediener tragen vollständige Reinraumanzüge (Overall, Haube, Handschuhe und Überschuhe), und Maschinen sind mit abgedichteten Schmiersystemen und glatten, nicht abgebenden Oberflächen konstruiert.
Darüber hinaus ist die Form selbst is a critical factor. In a standard environment, mold surfaces can develop micro-pitting or oxidation over time, which traps contaminants and transfers them to each subsequent part. In a Class 10000 cleanroom, molds are constructed from specialized stainless steels or hardened tool steels, polished to a mirror finish, and subjected to rigorous cleaning protocols between runs. This attention to mold surface integrity ensures that the part’s surface replicates the mold’s pristine condition, not the accumulated grime of production.
How Class 10000 Cleanroom Molding Works: A Step-by-Step Process
The process begins long before the molten polymer enters the mold. It starts with the material preparation. Polymer resins are stored in sealed containers within the cleanroom or in adjacent staging areas with desiccant dryers that remove moisture. Moisture is a hidden contaminant—when polymer pellets absorb water vapor, the water turns to steam during injection, creating surface defects called splay or silver streaks. In a Class 10000 environment, material handling is automated where possible, reducing human contact and the associated risk of contamination.
Machine and Tooling Considerations
The injection molding machine itself must be cleanroom-compatible. This means the machine's clamping unit, injection unit, and robot systems are enclosed or shielded to prevent particulate generation. Hydraulic systems are replaced with electric servo-driven machines where feasible, as electric machines produce zero hydraulic oil mist, a common source of airborne contamination. The machine's exterior is made of stainless steel or electro-polished aluminum, and all exposed surfaces are angled to prevent dust accumulation. The mold is fitted with a purge system that uses clean, dry air or nitrogen to blow away any loose particles before the mold closes.
Process Control and Environmental Monitoring
Once production begins, the environment is continuously monitored. Particle counters sample the air at regular intervals, and alarms trigger if particle counts approach the Class 10000 limit. Temperature and humidity are tightly controlled—typically 68-72°F (20-22°C) and 40-50% relative humidity—because fluctuations can affect polymer viscosity and dimensional stability. Operators follow strict gowning procedures, passing through air showers and sticky mats to remove loose particles from their clothing. Even the tools used for part removal are made of anti-static, non-shedding materials.
The molding parameters themselves—melt temperature, injection pressure, cooling time—are monitored via a Statistische Prozesskontrolle (SPC) system. This data is used to detect any drift in the process that could correlate with contamination. For example, an unexpected rise in injection pressure might indicate a blocked gate or a build-up of degraded polymer, both of which can introduce contaminants into the part. By catching these anomalies early, the cleanroom molding process ensures that purity is not just an environmental condition but a process outcome.
Critical Applications: Where Class 10000 Molding is Non-Negotiable
The demand for Class 10000 cleanroom molding has surged across several high-stakes industries. Understanding these applications illuminates why the investment in such facilities is justified.
- Medical Devices and Implants: From insulin pump components to orthopedic screws, these parts must be biocompatible and free from pyrogens (fever-inducing substances). A Class 10000 environment minimizes the risk of endotoxin contamination from bacterial debris.
- Pharmaceutical Packaging: Pre-filled syringes, vial stoppers, and inhaler mouthpieces require a sterile or high-purity surface to prevent drug-product interaction. Molding these in a cleanroom prevents particulate-induced degradation of the medication.
- Semiconductor and Electronics: Connectors, chip carriers, and sensor housings must be free of ionic contaminants that can corrode delicate circuitry. Even a single human hair (which is about 70 microns wide) can bridge circuit traces and cause a short.
- Aerospace and Defense: Optical components, valve bodies, and guide tubes for precision instruments must withstand extreme conditions without failing due to embedded impurities.
- Food and Beverage Processing: While not sterile, components like pump impellers and valve seals for food processing must be molded in a controlled environment to prevent bacterial harborage points.
Benefits Beyond Basic Cleanliness
The advantages of Class 10000 cleanroom molding extend beyond just meeting regulatory standards. First, it offers consistency. Because the environment is stable, the molding process itself is more repeatable. Manufacturers see fewer defects, lower scrap rates, and reduced downtime for re-cleaning. Second, it provides a competitive advantage. Companies that can certify their molding process to Class 10000 standards can bid on premium contracts that are inaccessible to standard molders. Third, it enables design innovation. Engineers can design more complex, tighter-tolerance parts knowing that the manufacturing environment will not introduce unpredictable variables.
Best Practices for Operating a Class 10000 Cleanroom Molding Facility
Achieving Class 10000 certification is not a one-time event; it is a continuous operational discipline. Adherence to best practices is essential for maintaining the integrity of the cleanroom and the quality of the molded parts.
Personnel Training and Gowning Protocol
People are the largest source of contamination, generating up to 10 million particles per minute while moving. Therefore, rigorous training is paramount. Operators must understand not just how to wear a cleanroom suit, but why. The gowning sequence must be followed precisely: hairnet, beard cover, jumpsuit, booties, and gloves. The suit must be made of a low-shedding material like polyester or a static-dissipative fabric. Movement inside the cleanroom should be slow and deliberate; rapid movements create air currents that can stir up settled particles. Eating, drinking, and wearing cosmetics are strictly prohibited.
Routine Cleaning and Validation
The cleanroom must be cleaned on a strict schedule using non-shedding, low-particulate wipes and sterile or filtered cleaning solutions. Floors are mopped daily, and surfaces are wiped down after each shift. However, cleaning itself can be a source of contamination if not done correctly. Therefore, cleaning is performed in a specific direction (from the cleanest area to the dirtiest) and with tools that are dedicated to the cleanroom. Additionally, the facility must undergo periodic certification—typically every 6 to 12 months—by an independent third-party that tests airborne particle counts, airflow velocity, and filter integrity. This certification is not just a formality; it is a legal requirement for many regulated industries, such as medical devices under ISO 13485 or pharmaceuticals under GMP guidelines.
Material and Tooling Management
Raw materials should be inspected upon arrival for packaging integrity. Incoming polymer pellets should be passed through a de-dusting or de-ionizing system before entering the cleanroom. The molds themselves should have a dedicated storage area within the cleanroom environment, protected by covers. When a mold is not in use, it should be stored under a nitrogen purge or in a sealed bag to prevent oxidation. The mold maintenance schedule must be strictly adhered to, with more frequent inspections for pitting, wear, or residue build-up than in a standard facility.
The Future of Cleanroom Molding: Trends and Innovations
As technology advances, the standards for cleanroom molding are becoming even more stringent. The industry is seeing a shift toward Class 1000 and even Class 100 cleanrooms for the most critical applications, particularly in next-generation semiconductor packaging and implantable drug-delivery devices. This is driven by the miniaturization of electronics and the growing complexity of combination products (drug-device hybrids).
Another trend is the integration of Industrie 4.0 technologies. Smart sensors embedded in the molding machine now provide real-time data on particle counts, temperature gradients, and humidity levels, feeding into a central AI system that can predictively adjust the molding parameters to maintain purity. Furthermore, the development of bio-based and biodegradable polymers that are inherently more sensitive to contamination is pushing cleanroom facilities to adopt even more advanced air purification technologies, such as photocatalytic oxidation (PCO), which destroys organic contaminants at a molecular level.
In conclusion, Class 10000 cleanroom molding is far more than a manufacturing niche; it is a critical enabler of modern technology and medicine. The purity it provides is not a luxury but a fundamental requirement for safety, functionality, and reliability. For manufacturers willing to invest in this discipline, the rewards are substantial: higher yields, premium market positioning, and the assurance that their products can be trusted in the most demanding environments. As the global demand for precision components continues to rise, the importance of cleanroom molding—and the purity it guarantees—will only grow.