
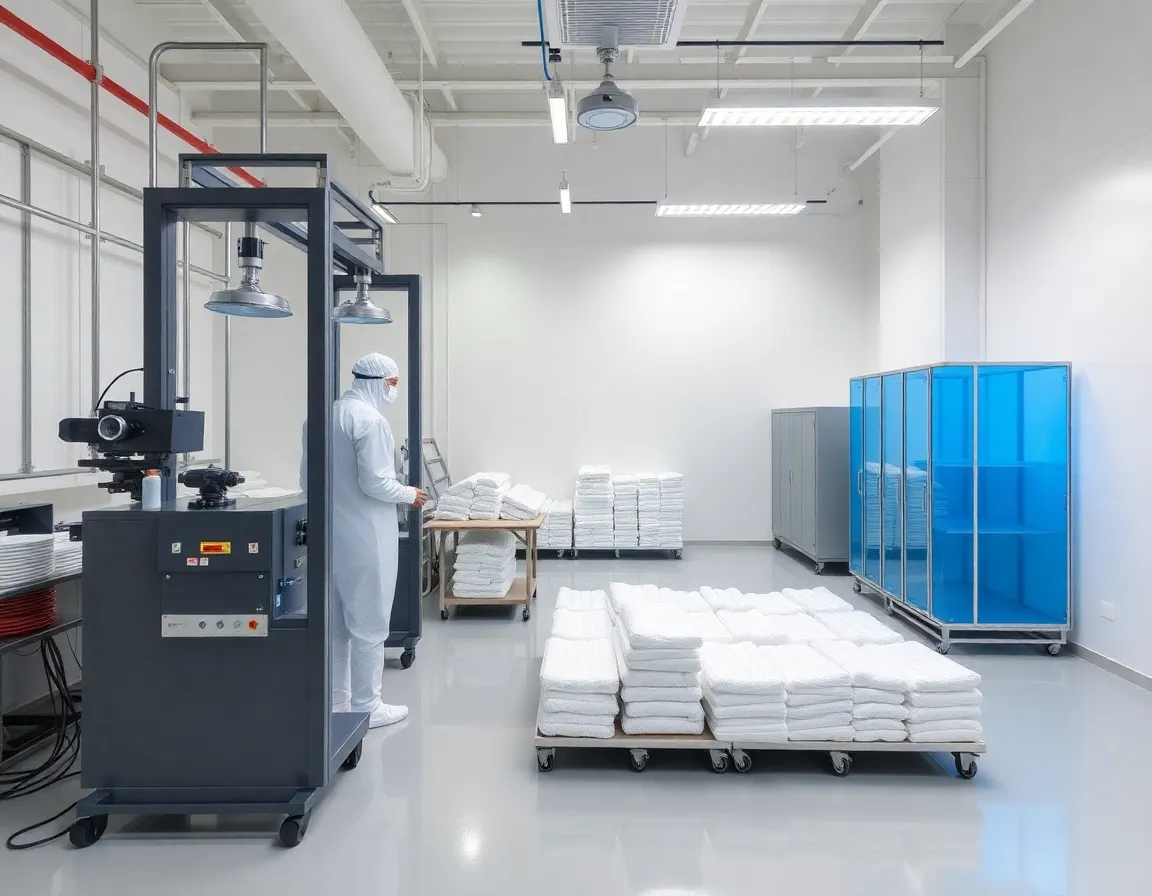
Comprendere lo stampaggio in camera bianca Classe 10000
Nel mondo della produzione di precisione, il margine di errore è misurato in micron e la presenza di un singolo contaminante microscopico può rendere inutile un intero lotto di produzione. Questa è la realtà per i settori che producono dispositivi medici, componenti a semiconduttore e apparecchiature ottiche. Al centro di questo ambiente rigoroso si trova lo Stampaggio in camera bianca Classe 10000, un processo di produzione specializzato che combina la fisica dello stampaggio a iniezione con la disciplina rigorosa di condizioni atmosferiche controllate. Ma cosa significa esattamente "Classe 10000" e perché è diventato lo standard di riferimento per la produzione di componenti critici?
La designazione "Classe 10000" si riferisce al numero massimo consentito di particelle aerodisperse (0,5 micrometri o più grandi) per piede cubo d'aria. In termini più semplici, una camera bianca di Classe 10000 contiene meno di 10.000 particelle di polvere, scaglie di pelle o altri inquinanti in ogni piede cubo di spazio. Per mettere questo in prospettiva, un tipico ambiente d'ufficio contiene tra 500.000 e 1 milione di tali particelle per piede cubo. Raggiungere e mantenere questo livello di pulizia richiede sofisticati sistemi di filtrazione dell'aria (filtri HEPA e ULPA), pressione dell'aria positiva, protocolli specializzati di vestizione e monitoraggio ambientale continuo. Quando applicato allo stampaggio a iniezione, questo livello di purezza trasforma un processo di produzione standard in una procedura scientifica altamente controllata.
La Scienza della Purezza: Perché la Contaminazione è il Killer Silenzioso
Per capire perché la purezza sia così importante nello stampaggio in camera bianca, bisogna prima apprezzare la vulnerabilità dei prodotti realizzati. Nelle applicazioni mediche, ad esempio, un catetere stampato o un sensore impiantabile deve avere una superficie immacolata. Qualsiasi particella che si incorpora nel polimero durante il processo di stampaggio può agire come sito di nucleazione per la crescita batterica. Allo stesso modo, nella produzione di semiconduttori, una singola particella di polvere intrappolata in un connettore stampato a iniezione può causare cortocircuiti elettrici, portando a guasti catastrofici del dispositivo. Le conseguenze della contaminazione non sono meramente estetiche; sono funzionali, critiche per la sicurezza e finanziariamente devastanti.
Le Fonti di Contaminazione nello Stampaggio Tradizionale
La contaminazione negli impianti di stampaggio standard proviene da molteplici vettori. Il più ovvio è la particolato aerodisperso—polvere, fibre dai vestiti e cellule della pelle rilasciate dagli operatori. Tuttavia, fonti meno ovvie includono la lubrificazione della macchina (oli idraulici e grassi che possono migrare sulla superficie dello stampo), la, gestione delle materie prime (granuli di polimero che accumulano carica statica e attirano la polvere) e le operazioni secondarie (sbavatura o imballaggio che introducono particolato). In un ambiente di Classe 10000, ciascuno di questi vettori viene sistematicamente neutralizzato. L'aria viene continuamente ricircolata attraverso filtri HEPA, gli operatori indossano tute complete per camera bianca (tute intere, cuffie, guanti e soprascarpe), e le macchine sono progettate con sistemi di lubrificazione sigillati e superfici lisce e non rilascianti.
Inoltre, lo stampo stesso is a critical factor. In a standard environment, mold surfaces can develop micro-pitting or oxidation over time, which traps contaminants and transfers them to each subsequent part. In a Class 10000 cleanroom, molds are constructed from specialized stainless steels or hardened tool steels, polished to a mirror finish, and subjected to rigorous cleaning protocols between runs. This attention to mold surface integrity ensures that the part’s surface replicates the mold’s pristine condition, not the accumulated grime of production.
How Class 10000 Cleanroom Molding Works: A Step-by-Step Process
The process begins long before the molten polymer enters the mold. It starts with the material preparation. Polymer resins are stored in sealed containers within the cleanroom or in adjacent staging areas with desiccant dryers that remove moisture. Moisture is a hidden contaminant—when polymer pellets absorb water vapor, the water turns to steam during injection, creating surface defects called splay or silver streaks. In a Class 10000 environment, material handling is automated where possible, reducing human contact and the associated risk of contamination.
Machine and Tooling Considerations
The injection molding machine itself must be cleanroom-compatible. This means the machine's clamping unit, injection unit, and robot systems are enclosed or shielded to prevent particulate generation. Hydraulic systems are replaced with electric servo-driven machines where feasible, as electric machines produce zero hydraulic oil mist, a common source of airborne contamination. The machine's exterior is made of stainless steel or electro-polished aluminum, and all exposed surfaces are angled to prevent dust accumulation. The mold is fitted with a purge system that uses clean, dry air or nitrogen to blow away any loose particles before the mold closes.
Process Control and Environmental Monitoring
Once production begins, the environment is continuously monitored. Particle counters sample the air at regular intervals, and alarms trigger if particle counts approach the Class 10000 limit. Temperature and humidity are tightly controlled—typically 68-72°F (20-22°C) and 40-50% relative humidity—because fluctuations can affect polymer viscosity and dimensional stability. Operators follow strict gowning procedures, passing through air showers and sticky mats to remove loose particles from their clothing. Even the tools used for part removal are made of anti-static, non-shedding materials.
The molding parameters themselves—melt temperature, injection pressure, cooling time—are monitored via a Controllo Statistico di Processo (SPC) system. This data is used to detect any drift in the process that could correlate with contamination. For example, an unexpected rise in injection pressure might indicate a blocked gate or a build-up of degraded polymer, both of which can introduce contaminants into the part. By catching these anomalies early, the cleanroom molding process ensures that purity is not just an environmental condition but a process outcome.
Critical Applications: Where Class 10000 Molding is Non-Negotiable
The demand for Class 10000 cleanroom molding has surged across several high-stakes industries. Understanding these applications illuminates why the investment in such facilities is justified.
- Medical Devices and Implants: From insulin pump components to orthopedic screws, these parts must be biocompatible and free from pyrogens (fever-inducing substances). A Class 10000 environment minimizes the risk of endotoxin contamination from bacterial debris.
- Pharmaceutical Packaging: Pre-filled syringes, vial stoppers, and inhaler mouthpieces require a sterile or high-purity surface to prevent drug-product interaction. Molding these in a cleanroom prevents particulate-induced degradation of the medication.
- Semiconductor and Electronics: Connectors, chip carriers, and sensor housings must be free of ionic contaminants that can corrode delicate circuitry. Even a single human hair (which is about 70 microns wide) can bridge circuit traces and cause a short.
- Aerospace and Defense: Optical components, valve bodies, and guide tubes for precision instruments must withstand extreme conditions without failing due to embedded impurities.
- Food and Beverage Processing: While not sterile, components like pump impellers and valve seals for food processing must be molded in a controlled environment to prevent bacterial harborage points.
Benefits Beyond Basic Cleanliness
The advantages of Class 10000 cleanroom molding extend beyond just meeting regulatory standards. First, it offers consistency. Because the environment is stable, the molding process itself is more repeatable. Manufacturers see fewer defects, lower scrap rates, and reduced downtime for re-cleaning. Second, it provides a competitive advantage. Companies that can certify their molding process to Class 10000 standards can bid on premium contracts that are inaccessible to standard molders. Third, it enables design innovation. Engineers can design more complex, tighter-tolerance parts knowing that the manufacturing environment will not introduce unpredictable variables.
Best Practices for Operating a Class 10000 Cleanroom Molding Facility
Achieving Class 10000 certification is not a one-time event; it is a continuous operational discipline. Adherence to best practices is essential for maintaining the integrity of the cleanroom and the quality of the molded parts.
Personnel Training and Gowning Protocol
People are the largest source of contamination, generating up to 10 million particles per minute while moving. Therefore, rigorous training is paramount. Operators must understand not just how to wear a cleanroom suit, but why. The gowning sequence must be followed precisely: hairnet, beard cover, jumpsuit, booties, and gloves. The suit must be made of a low-shedding material like polyester or a static-dissipative fabric. Movement inside the cleanroom should be slow and deliberate; rapid movements create air currents that can stir up settled particles. Eating, drinking, and wearing cosmetics are strictly prohibited.
Routine Cleaning and Validation
The cleanroom must be cleaned on a strict schedule using non-shedding, low-particulate wipes and sterile or filtered cleaning solutions. Floors are mopped daily, and surfaces are wiped down after each shift. However, cleaning itself can be a source of contamination if not done correctly. Therefore, cleaning is performed in a specific direction (from the cleanest area to the dirtiest) and with tools that are dedicated to the cleanroom. Additionally, the facility must undergo periodic certification—typically every 6 to 12 months—by an independent third-party that tests airborne particle counts, airflow velocity, and filter integrity. This certification is not just a formality; it is a legal requirement for many regulated industries, such as medical devices under ISO 13485 or pharmaceuticals under GMP guidelines.
Material and Tooling Management
Raw materials should be inspected upon arrival for packaging integrity. Incoming polymer pellets should be passed through a de-dusting or de-ionizing system before entering the cleanroom. The molds themselves should have a dedicated storage area within the cleanroom environment, protected by covers. When a mold is not in use, it should be stored under a nitrogen purge or in a sealed bag to prevent oxidation. The mold maintenance schedule must be strictly adhered to, with more frequent inspections for pitting, wear, or residue build-up than in a standard facility.
The Future of Cleanroom Molding: Trends and Innovations
As technology advances, the standards for cleanroom molding are becoming even more stringent. The industry is seeing a shift toward Class 1000 and even Class 100 cleanrooms for the most critical applications, particularly in next-generation semiconductor packaging and implantable drug-delivery devices. This is driven by the miniaturization of electronics and the growing complexity of combination products (drug-device hybrids).
Another trend is the integration of Industry 4.0 technologies. Smart sensors embedded in the molding machine now provide real-time data on particle counts, temperature gradients, and humidity levels, feeding into a central AI system that can predictively adjust the molding parameters to maintain purity. Furthermore, the development of bio-based and biodegradable polymers that are inherently more sensitive to contamination is pushing cleanroom facilities to adopt even more advanced air purification technologies, such as photocatalytic oxidation (PCO), which destroys organic contaminants at a molecular level.
In conclusion, Class 10000 cleanroom molding is far more than a manufacturing niche; it is a critical enabler of modern technology and medicine. The purity it provides is not a luxury but a fundamental requirement for safety, functionality, and reliability. For manufacturers willing to invest in this discipline, the rewards are substantial: higher yields, premium market positioning, and the assurance that their products can be trusted in the most demanding environments. As the global demand for precision components continues to rise, the importance of cleanroom molding—and the purity it guarantees—will only grow.