
Budgeting for multi-material polymer manufacturing requires balancing upfront tooling investments against piece-part production economics. Estimating the average cost of overmold tooling and production parts requires evaluating substrate mold complexity, elastomer selection, and automation levels. Procurement managers frequently encounter unexpected cost variations when transitioning from single-material injection molding to multi-shot encapsulation.
Unplanned tooling NRE expenses, secondary manual labor costs, and specialized elastomeric resin pricing can inflate total project budgets. This technical financial guide breaks down primary tooling expense drivers, material price variations, automation payback thresholds, and practical DfM cost-reduction strategies.
Core Cost Components: Dual Molds vs. Single 2K Rotary Tooling
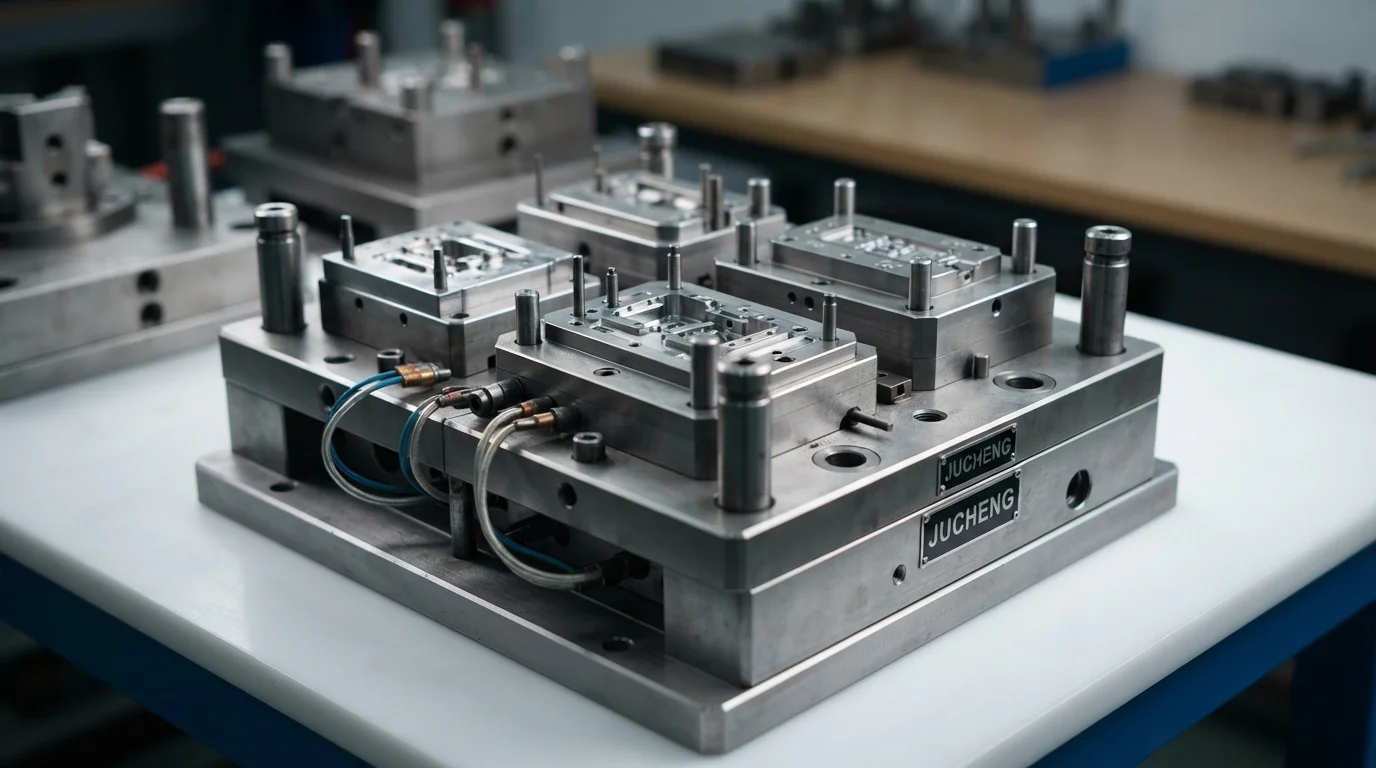
다중 재료 몰딩에서 금형 비용은 가장 큰 초기 재정적 투자를 차지합니다. 제조 팀은 두 가지 주요 금형 툴링 경로 중에서 선택합니다: 2단계 이중 캐비티 트랜스퍼 금형 또는 단일 프레스 회전식 2K 금형 툴링. 2단계 이송 금형 툴링은 두 개의 별도 금형 베이스를 활용하며, 강성 기판은 1차 프레스에서 성형되고 수동 또는 로봇으로 2차 오버몰드 캐비티로 이송됩니다. 이송 금형 툴링은 초기 금형 개발 자본을 40~60% 절감하여 프로토타입 제작 및 저~중량 생산에 매우 경제적입니다.
회전식 2K 금형 툴링은 두 개의 서로 다른 캐비티와 자동 180도 인덱싱 플래튼을 단일 복합 금형 베이스에 통합합니다. 회전식 툴링은 초기 자본이 상당히 높지만, 부품의 2차 핸들링을 제거하고 사이클 타임을 단축하여 50,000개 이상의 대량 생산 프로그램에서 최저 단가를 제공합니다. 아래 표 1은 주요 오버몰딩 아키텍처별 금형 및 부품 단가 내역을 요약합니다:
| 금형 아키텍처 | 초기 금형 NRE (USD) | 부품 단가 (USD) | 최적 생산 수량 | 주요 재정적 트레이드오프 |
|---|---|---|---|---|
| 래피드 브리지 이송 금형 툴링 | $4,500 – $9,500 | $2.50 – $6.00 | 1,000 ~ 5,000개 | 가장 낮은 초기 자본; 높은 사이클 인건비 |
| 양산 2단계 스틸 금형 툴링 | $12,000 – $25,000 | $1.20 – $3.00 | 5,000 ~ 50,000개 부품 | 균형 잡힌 금형 비용; 중간 수준의 자동화 처리량 |
| 통합 2K 로터리 플래튼 툴링 | $35,000 – $75,000+ | $0.55 – $1.50 | 50,000 ~ 500,000개 이상 부품 | 최고의 초기 자본; 최저 단위 부품 비용 |
개별 부품 변동 비용: 수지 가격, 기계 시간당 요금 및 사이클 인건비
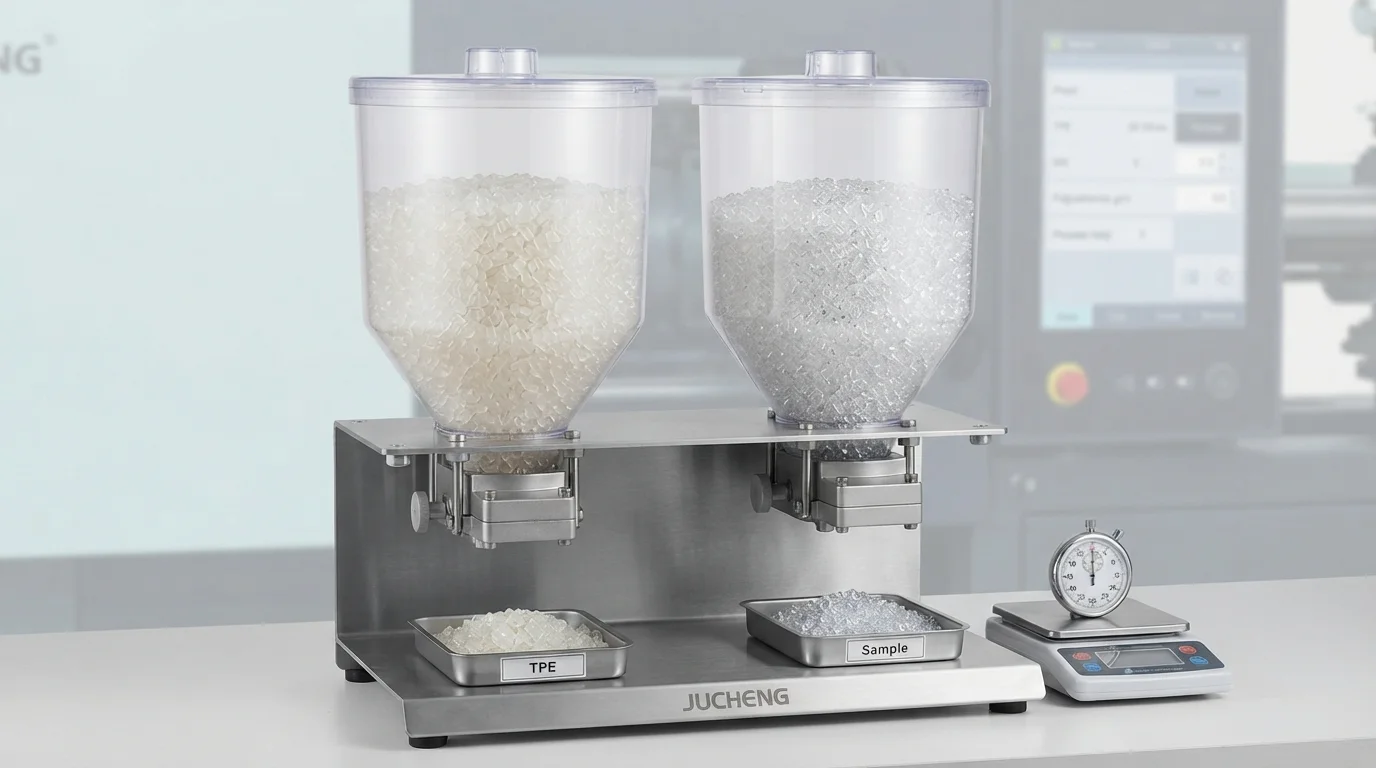
원료 수지 선택은 개별 부품 재료 비용에 직접적인 영향을 미칩니다. 다음과 같은 특수 엘라스토머 수지는 TPE, TPU, 또는 의료용 등급 화합물은 범용 기재 수지인 ABS 또는 폴리카보네이트(PC). 엘라스토머 부피는 미관상 과도한 두께에 불필요한 재료 사용을 방지하기 위해 CAD 모델에서 최적화되어야 합니다.
기계 시간당 운영 요금은 필요한 클램핑 포스 톤수와 사이클 시간에 따라 달라집니다. 오버몰딩은 두 번의 연속 사출 및 냉각 단계를 필요로 하므로, 총 사이클 시간은 샷당 35~65초로 단일 재료 부품의 20초와 비교됩니다. 벽 두께를 최소화하고 냉각 채널 배치를 최적화하면 냉각 지연이 줄어들어 기계 시간당 운영 비용이 절감됩니다.
자동 로봇 로딩 vs. 수동 이송: 상각 임계값
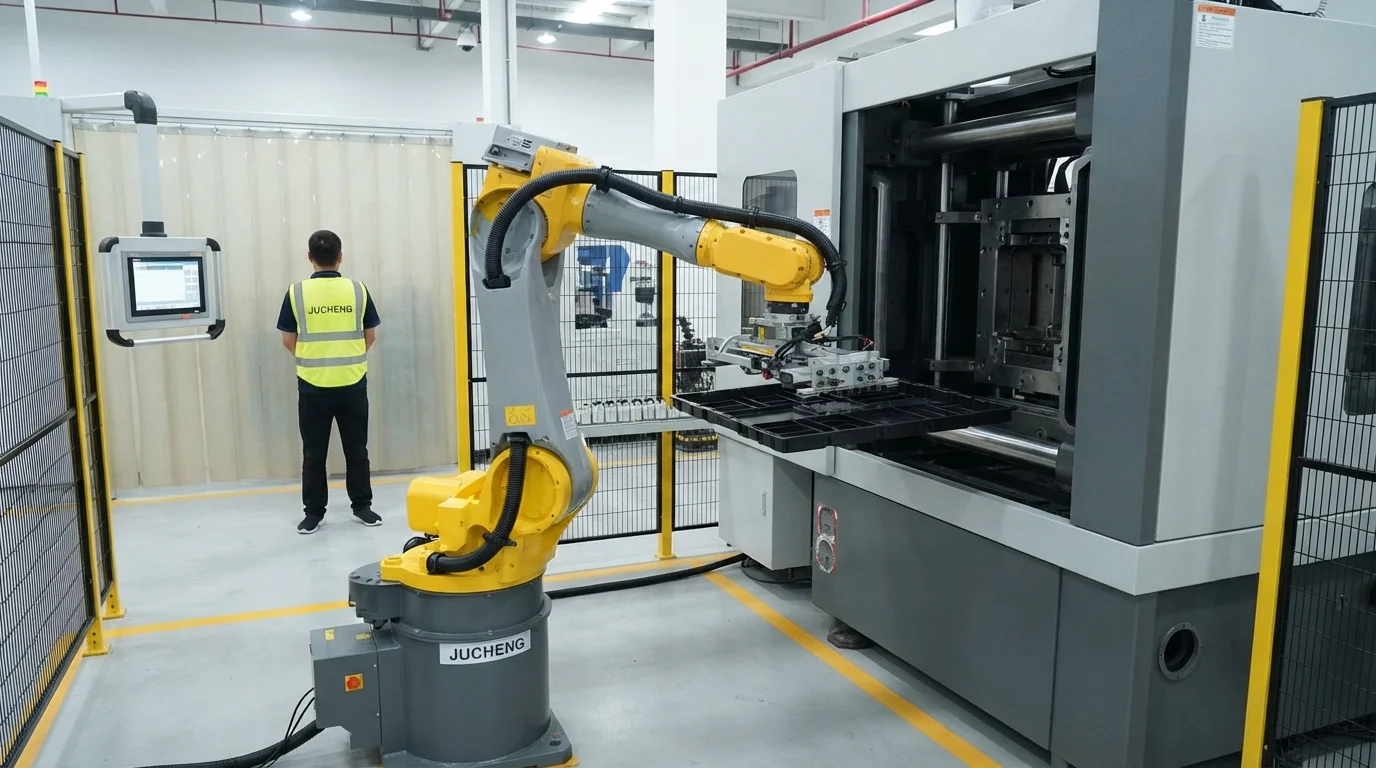
인건비는 2단계 오버몰딩 작업에서 주요 변동 비용 요인입니다. 수동 작업자 이송은 기판을 2차 캐비티에 배치하기 위해 전담 기술자가 필요하며, 작업자 피로와 사이클 시간 변동을 초래합니다. 부품 이송 자동화에는 6축 다관절 로봇 및 맞춤형 로봇식 엔드 오브 암 툴링.
재무적 손익분기점을 계산하면 자동화가 연간 20,000개 이상의 생산량에서 빠르게 투자 비용을 회수한다는 것을 알 수 있습니다. 로봇식 로딩은 부품 배치 오류를 제거하고, 셧오프 강철 파손을 방지하며, 시간당 생산 수율을 안정화합니다.
자동화 ROI 평가 매개변수는 다음과 같습니다:
- 볼륨 임계값 평가—연간 수요를 평가하여 수동 로딩과 로봇 자동화 중 어느 것이 가장 낮은 총 비용을 제공하는지 결정합니다.
- 사이클 타임 단축—기판 로딩 자동화는 샷당 최대 8초의 트랜스퍼 지연을 줄입니다.
- 수율 안정화—로봇식 위치 결정은 인서트 정렬 불량을 제거하여 스크랩률을 0.5% 미만으로 낮춥니다.
- 인건비 절감—프레스 셀 자동화는 다교대 생산 운영에서 직접 기계 운영자 노동을 줄입니다.
오버몰딩 금형 및 부품 비용 절감을 위한 엔지니어링 전략
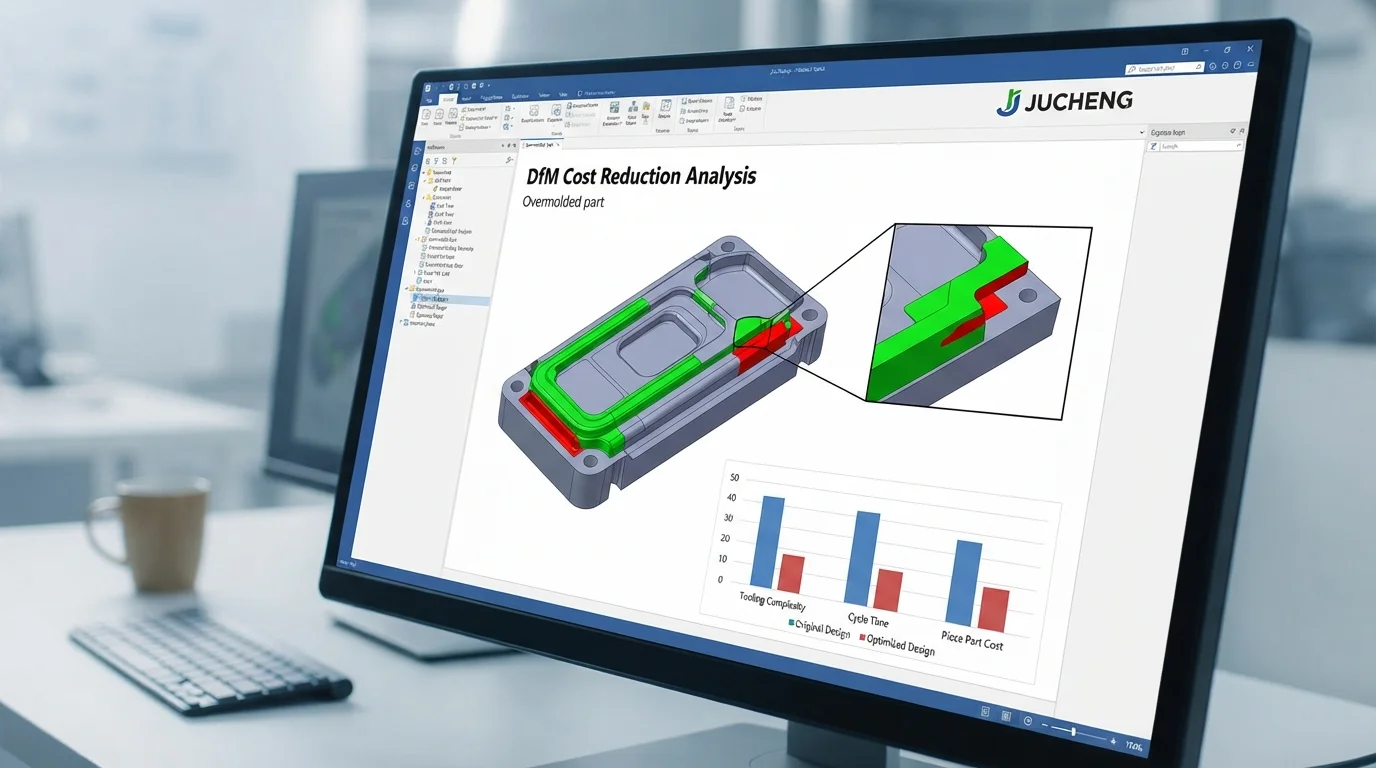
Deploying proactive DfM engineering guidelines before cutting mold steel delivers substantial cost savings. Simplifying shut-off lands by designing flat, 90-degree sealing shoulders avoids expensive 3D contoured shut-off machining. Incorporating line-of-draw pass-through shut-offs eliminates complex side-action sliders and mechanical lifters, reducing mold complexity by 25%.
Maintaining uniform elastomer wall thicknesses between 1.5 mm and 2.5 mm avoids cosmetic sink marks and shortens cooling times. Partnering with an experienced contract manufacturer for 오버몰딩 사출 성형 projects ensures that part geometries, mold architectures, and material choices are optimized for maximum commercial ROI.
자주 묻는 질문 (FAQ)
What is the typical average cost of overmold tooling for prototypes?
Average cost of overmold tooling for quick-turn prototypes typically ranges from $4,500 to $9,500 for a two-piece modular transfer mold set. Rapid aluminum or soft steel tooling allows product teams to validate multi-material parts in low volumes without committing to expensive production steel tooling.
Why is overmolding more expensive than single-material injection molding?
Overmolding requires either two separate mold tools or a complex 2K rotary tool, which roughly doubles initial tooling expenditure. Longer cycle times and higher raw material costs for elastomeric resins (TPE, TPU, TPV) also increase piece-part unit pricing.
How many parts are needed to justify the cost of 2K rotary platen tooling?
Annual production volumes exceeding 50,000 units typically justify the higher upfront investment of 2K rotary platen tooling. Lower unit cycle times and zero manual transfer labor quickly offset the higher initial mold cost over high-volume series production.
How does part geometry impact overmolding mold costs?
Complex 3D parting lines, deep undercuts, and intricate side-action shut-offs increase mold machining time and NRE costs. Designing flat 90-degree shut-off lands and line-of-draw features keeps mold construction simple and economical.
Can using regrind resin lower overmolding production expenses?
Regrind resin can be blended into rigid substrate materials like ABS or PP to reduce raw material costs by 10% to 20%. However, elastomeric overmold resins (TPE/TPU) should utilize virgin material to ensure maximum chemical bonding and prevent surface splay.
Why is an early 24-hour DfM review crucial for controlling overmolding budgets?
Conducting an early DfM review detects uneven wall thicknesses, sharp corners, and shut-off interference while the CAD model is still digital. Identifying these issues early eliminates expensive mold rework, tooling modifications, and project launch delays.