
In thin-wall molding, the gate is not just an inlet; it determines how far the melt must travel, where flow fronts meet, and which surfaces carry gate evidence. A useful thin wall injection molding gate design balances a short, stable flow path with acceptable vestige, packing access, and part appearance. The right location depends on the part’s wall map, resin, geometry, and tool constraints—not on a universal gate style.
Map the flow path before selecting a gate
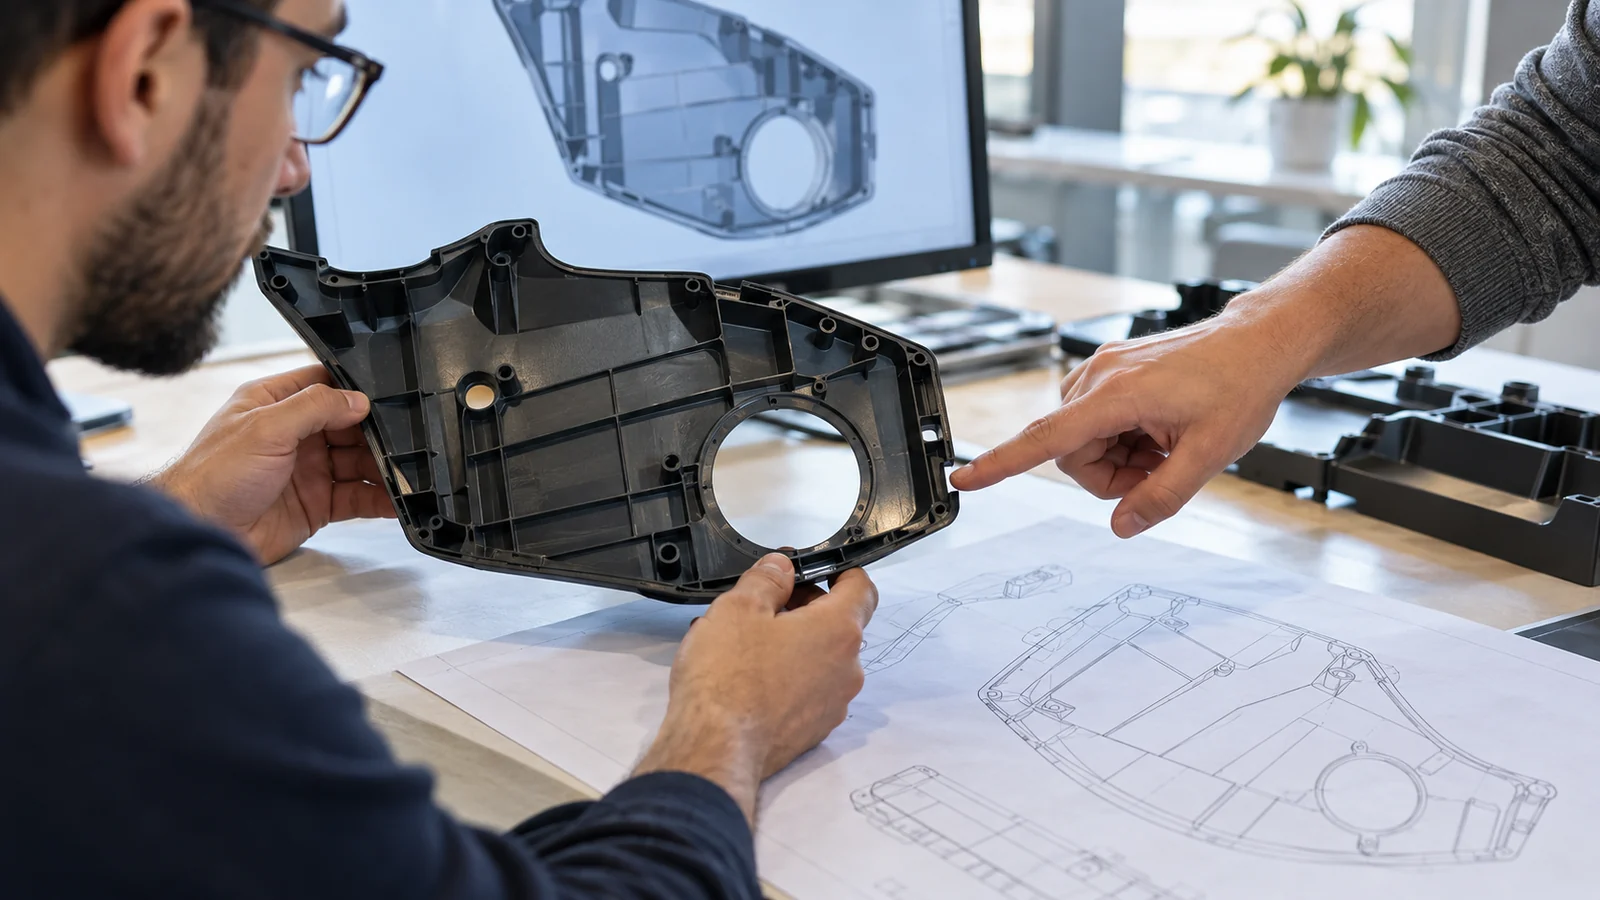
Start with the thinnest sections, longest flow distance, ribs, bosses, windows, and transitions. In a thin section, the melt can lose heat quickly against the mold steel; a long path or abrupt restriction can make filling harder and increase sensitivity to process variation. The gate should support a flow path that reaches remote regions without forcing the front to split and reunite in a structurally or visually critical location.
Review the complete cavity, not just a single 2D silhouette. A gate that appears central in plan view may feed a deep feature unevenly or create an unbalanced flow around an opening. Flow analysis can compare candidate locations and flag potential weld-line or pressure concerns, but the model depends on material, boundary conditions, and assumptions. It is a decision aid—not a substitute for a molding trial.
Choose location by function and appearance
Gate placement should begin with part function. Keep the gate and its vestige away from sealing surfaces, sliding interfaces, snap features, optical or show surfaces, and dimensions that are difficult to rework. If the gate must sit on a visible face, align that choice with the appearance specification and finishing plan before the tool is released.
Then examine how the gate feeds the cavity. The location affects flow length, pressure loss, packing access, weld-line positions, and the direction in which the material fills around holes and ribs. A gate moved merely to hide a mark can create an undesirable weld line or leave a remote thin wall difficult to fill. The design review should record which tradeoff is being accepted and how it will be evaluated.
For a thin-wall project, connect gate decisions with the broader thin-wall injection molding requirements: wall consistency, resin selection, mold support, venting, and process validation interact. Changing only the gate may not resolve a problem caused by a thickness jump or trapped air.
Match gate type to the part, not the trend

Edge, tab, fan, direct, and other gate arrangements each create different flow and vestige conditions. A wider entry may distribute flow across a broad region; a small gate may be easier to trim but can restrict flow and complicate packing. Gate type also affects tool complexity and the amount of finishing needed after molding.
| Decision question | Why it matters | Evidence to review |
|---|---|---|
| Where can a vestige be accepted? | Controls feasible gate faces and trimming | Cosmetic zones and assembly interfaces |
| How long is the flow path? | Long paths can raise fill difficulty in thin areas | Wall map, flow simulation, short-shot study |
| Where will fronts meet? | Weld lines may affect appearance or function | Flow pattern and critical load directions |
| Can the gate be packed consistently? | Affects local shrinkage and repeatability | Gate geometry, process window, part measurements |
The site’s gate-type guide provides a broader comparison. For thin walls, use it as a shortlist and then screen each candidate against the actual cavity, resin, vestige limits, and tool layout.
Read the warning signs in a trial
Short shots, burn marks, hesitation, visible weld lines, gate blush, and inconsistent dimensions can each point to different causes. A short shot does not automatically mean the gate is too small; restricted venting, a cold flow path, an unfavorable wall transition, or a process limit can produce a similar symptom. Record where the defect begins and how it changes with controlled adjustments.
Look at the part by cavity and location. A repeatable defect near one flow endpoint may call for a gate or vent review. A defect that moves with process conditions may indicate a different control issue. Preserve the approved process window and compare one controlled change at a time so the trial can distinguish cause from coincidence.
A design review that prevents late gate changes
- Mark constraints: show show surfaces, sealing features, load paths, and acceptable vestige zones.
- Compare candidate locations: assess flow length, balance, weld-line placement, and tool access.
- Check interactions: review wall transitions, vents, cooling, ejectors, and trimming access together.
- Define acceptance: state how appearance, fill, dimensions, and gate removal will be checked.
- Keep options traceable: save the chosen gate rationale and trial observations with the tool documentation.
This is especially important when appearance and filling goals conflict. A slightly less convenient gate position may be the better engineering decision if it protects a functional surface and produces a more stable flow pattern.
Frequently asked questions
Is a larger gate always better for a thin-wall part?
No. A larger entry may reduce restriction, but it can also increase vestige, require more trimming, or place evidence on an unacceptable surface. Evaluate flow, packing, appearance, and tool constraints together.
Should the gate be placed at the thickest area?
That can be a useful starting hypothesis, but it is not a universal rule. The best location depends on the full geometry, flow path, weld-line risk, resin, and the surfaces that must remain clean or functional.
Can simulation decide the final gate position?
Simulation can compare candidate locations and highlight likely flow behavior. Final selection should also consider actual tool construction, molded-part appearance, dimensions, and trial evidence.
Before releasing a thin-wall tool, make the gate location an explicit design decision with documented functional limits and a practical validation plan.