
Short answer: A plastic part can be electroplated reliably only when the substrate grade, molded surface and part geometry are compatible with the selected plating system. Favor smooth, accessible surfaces, gradual transitions, uniform walls and controlled molded-in stress; then validate appearance and adhesion on production-intent molded parts. Plating is not a cosmetic layer that can hide an unstable substrate.
These plastic electroplating design guidelines focus on what a product designer can control before tool release. A plating supplier can define its chemistry and process window, but the part designer still determines whether the surface is reachable, whether geometry creates local stress, and whether the drawing describes what must pass inspection.
For the finishing route itself, see our plastic electroplating service and related surface finishing options. Entec Polymers’ technical note on injection molding thermoplastics for electroplating is a useful reference for the interaction among design, molding and plate adhesion.
In this article:
- Start with the finish and substrate
- Design geometry for even coverage
- Control the molded surface before plating
- Write a useful qualification plan
- Frequently asked questions
Start With the Finish and Substrate
Before choosing a resin, define the function of the plated surface. Is it a decorative bright finish, a conductive layer, a wear surface, or a combination? Identify the zones that require plating, the appearance standard, the expected handling and exposure, and whether the coating must meet an electrical or mechanical requirement. Different goals can call for different layer systems, substrate grades and validation tests.
Not every injection-molding resin is suitable for every plating process. Many plastic plating systems rely on a substrate and pretreatment route developed for that purpose; the resin’s chemistry, filler package, pigment, recycled content and surface condition may all matter. Do not specify a generic resin family and assume every grade in that family will plate the same way. Confirm the exact commercial grade and plating sequence with both material and finishing suppliers before freezing the design.
Also define the interfaces between plated and unplated areas. Masking lines, contact points, edges and hidden surfaces should be shown on the drawing or a controlled model. If only one face is cosmetic, review how the part will be racked and handled without damaging the show surface. If conductivity is required, state where it is measured and what electrical performance is needed; a metallic appearance alone does not establish electrical function.
Design Geometry for Even Coverage
Electroplating adds material through a wet process, and local current distribution and solution access can vary with shape. Deep recesses, narrow gaps, sharp corners and abrupt protrusions can be difficult to plate uniformly or inspect consistently. Where the design allows, use generous radii, open transitions and accessible surfaces. Avoid narrow slots or hidden pockets in critical plated zones unless the finishing supplier confirms a workable method.
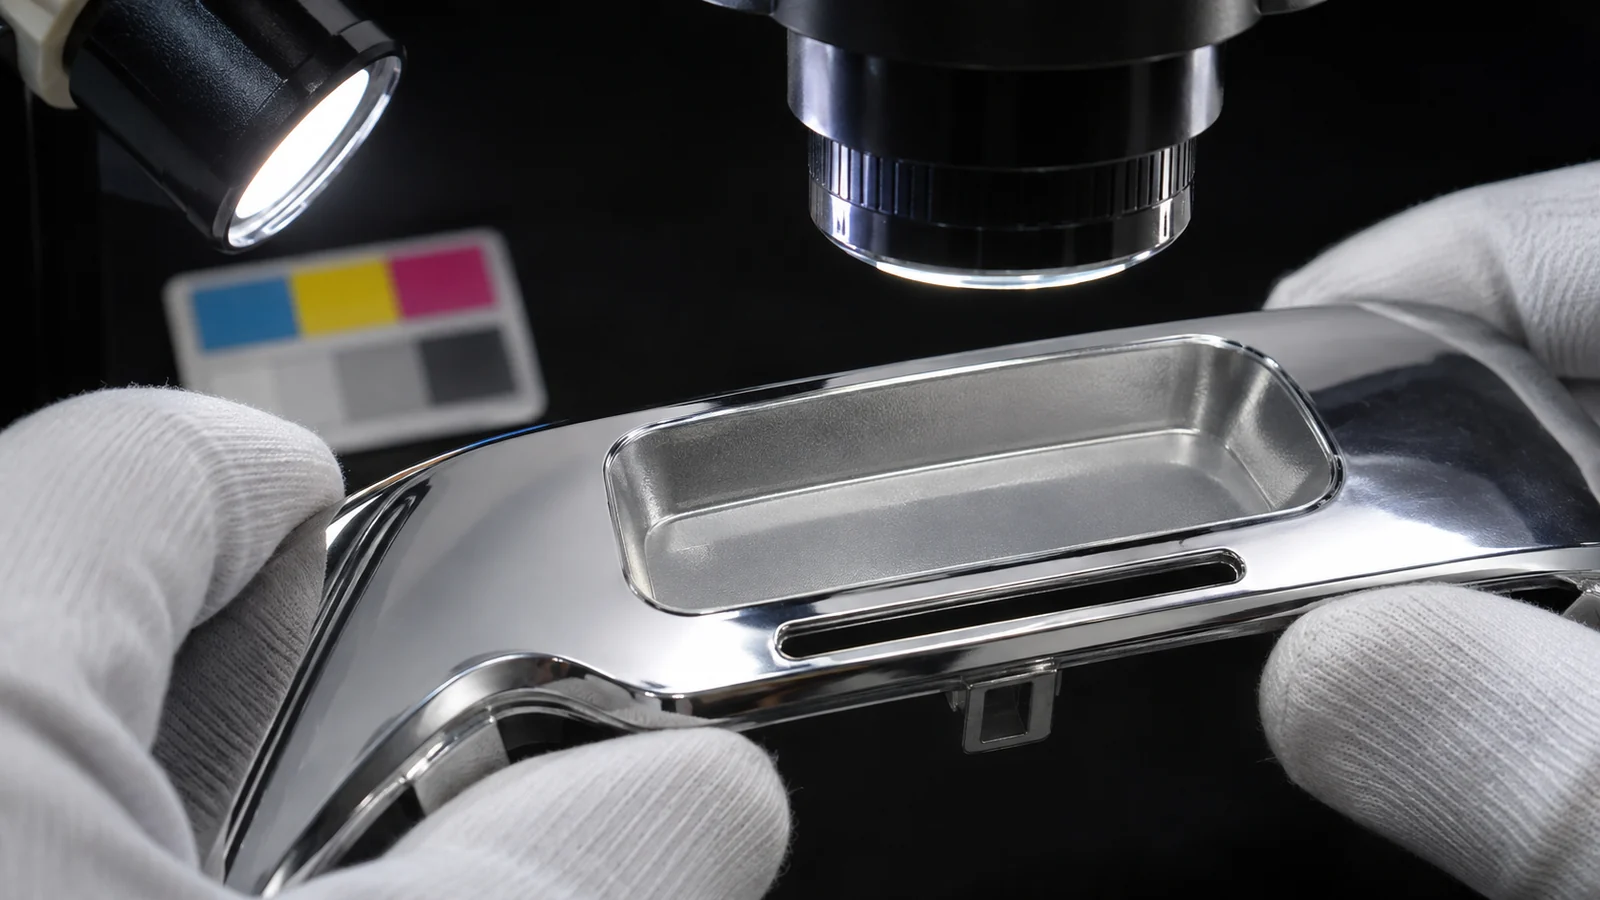
Keep wall thickness as uniform as practical and avoid abrupt thick-to-thin transitions. This is sound molding practice, but it is especially important when a premium plated surface will reveal distortion, sink, flow lines or residual stress that may be less visible on bare plastic. Place ribs and bosses away from the show surface where feasible, and use smooth transitions rather than sharp internal corners. The exact geometry should be assessed with the selected resin and mold concept, not a universal rule of thumb.
Gate placement is a joint design decision. A gate directly on a show surface may leave a vestige that is difficult to conceal, while a gate at the wrong location can promote visible flow patterns or uneven packing. Put the gate where the molder can fill and pack the part while protecting cosmetic zones, then review the expected flow path and any weld lines against the plated area.
| Feature to review | Potential concern after plating | Design response |
|---|---|---|
| Sharp corners and edges | Stress concentration or visually inconsistent coating at transitions | Use radii and evaluate edge coverage with the finisher |
| Deep pockets and narrow gaps | Limited access, variable deposition or trapped process solution | Open the feature or confirm process access before release |
| Thick sections and nearby bosses | Sink, warpage or stress showing through a reflective finish | Maintain practical wall transitions and isolate structure from show zones |
| Gate on a visible face | Vestige or flow-related appearance variation | Relocate or define an acceptable gate zone and inspection boundary |
Control the Molded Surface Before Plating
Plating quality begins with the molded part. A surface that carries stress, contamination, inconsistent texture or a flow defect may respond differently during pretreatment and plating. Keep the mold surface specification consistent across the critical area, avoid unnecessary tool texture changes, and identify weld lines or knit lines that must not cross the primary show zone if the flow analysis and part geometry allow an alternative.
Process stability matters because changes in melt temperature, fill speed, packing, cooling or resin drying can alter surface condition and molded-in stress. The finishing supplier should evaluate representative molded pieces, not only polished prototype samples made by a different process. If parts are stored between molding and plating, agree how they are protected from fingerprints, release agents, dust and abrasion.
Do not assume that a thicker metal layer will cover a molding defect. A reflective finish can make small surface irregularities more noticeable. Agree the acceptable substrate condition and plated appearance separately, and define whether the supplier may rework parts or whether rework is prohibited on cosmetic areas.
Write a Useful Qualification Plan
- Freeze the material and process route. Record the exact resin grade, colorant or filler, molding condition range, pretreatment and plating stack. Any proposed substitution should trigger a documented review.
- Mark critical surfaces. Show plated zones, masked areas, contact points, boundaries and visual grades directly on the drawing or controlled model.
- Choose measurable acceptance criteria. Define appearance under agreed lighting and viewing conditions, coating coverage, adhesion method, thickness locations if applicable, and any conductivity or corrosion requirements.
- Trial representative geometry. Use the intended molded substrate and include features that challenge coverage: edges, recesses, bosses, openings and transitions.
- Review failure location, not just pass/fail. If adhesion or appearance varies, trace whether the cause is substrate grade, molded stress, contamination, geometry, pretreatment or plating setup before changing the coating thickness.
The drawing should distinguish an appearance expectation from a functional requirement. A bright finish can be acceptable visually but fail a conductivity or durability need; a functional coating can meet its specification while showing cosmetic variation. Name the required outcome, method and inspection zone so the team does not have to infer which one matters most.
Frequently Asked Questions
Which plastic is easiest to electroplate?
There is no universal answer because suitability depends on the exact grade and plating chemistry. Use a grade that the selected finishing supplier has qualified for the required system, and validate it with the intended color, filler and molding process rather than relying on a broad resin-family label.
Should the gate be kept off the plated surface?
When practical, keep the gate vestige outside the most critical show zone. The final position must still support mold filling, packing and part quality. Review the vestige, expected flow pattern and plating boundary together before the tool layout is finalized.
Can plating hide sink marks or flow lines?
Do not design on that assumption. Reflective or metallic finishes can make substrate irregularities more visible. Correct the molding or geometry cause where possible, then qualify the plated part using production-intent molded samples and defined appearance criteria.