
The Imperative of Contamination Control in Modern Electronics
In the microcosmic world of semiconductor fabrication, medical devices, and advanced optics, the presence of a single dust particle—invisible to the naked eye—can render a product utterly useless. As electronic components shrink to nanoscale dimensions and become increasingly sensitive, the environment in which they are manufactured must be controlled with military-grade precision. This is where electronic cleanroom molding emerges as a critical, non-negotiable discipline. It is not merely about manufacturing in a clean room; it is about the synergistic integration of specialized molding processes, material science, and facility design to produce components with zero tolerance for particulate, ionic, or molecular contamination.
Electronic cleanroom molding refers to the injection molding, compression molding, or transfer molding of plastic and elastomeric components within a controlled environment that meets specific ISO cleanliness classifications. Unlike standard injection molding, which tolerates airborne particulates, moisture, and outgassing, cleanroom molding demands a holistic approach. Every element—from the resin pellets to the mold steel, from the robotic handling equipment to the operator’s gown—must be vetted to prevent contamination. The goal is not just dimensional accuracy but chemical and physical purity, ensuring that the final part does not introduce defects into the sensitive electronic assembly it protects or houses.
This guide serves as a comprehensive manual for engineers, quality managers, and procurement specialists looking to navigate the complexities of this specialized manufacturing niche. We will dissect the methodology, explore the material constraints, outline the operational protocols, and highlight the transformative benefits that precision molding in a cleanroom environment brings to the electronics supply chain.
Understanding the ISO Classifications and Airflow Dynamics
Before a single shot of plastic is injected, the manufacturing environment must be engineered to meet rigorous international standards. The primary framework is defined by ISO 14644-1, which classifies cleanrooms based on the number and size of particles permitted per cubic meter of air. For electronic molding, the most common classifications are ISO Class 7 (formerly Class 10,000) and ISO Class 8 (formerly Class 100,000), though advanced microelectronics increasingly demand ISO Class 5 or better in critical zones.
The Role of Laminar Airflow and Positive Pressure
The physical layout of a cleanroom molding facility is designed around the principle of unidirectional airflow. High-efficiency particulate air (HEPA) and ultra-low penetration air (ULPA) filters are strategically placed in the ceiling, pushing clean air downward in a laminar, non-turbulent stream. This airflow acts as an invisible conveyor belt, sweeping away any particles generated by the molding machine’s moving parts or the operator. Additionally, the cleanroom is kept under positive pressure relative to adjacent non-clean areas. This ensures that when doors are opened, air flows outward, preventing unfiltered external air from rushing in and compromising the environment. The molding machine itself is often enclosed in a secondary mini-environment or "tunnel" with its own dedicated filtration, creating a clean-in-clean-out (CICO) zone around the mold cavity.
Material Handling and Drying Systems
Contamination does not only come from the air; it originates in the raw material. Standard polymer pellets are hygroscopic, absorbing atmospheric moisture and static charge that attracts dust. In an electronic cleanroom molding setup, resin is not simply dumped into a hopper. Instead, it is transferred through a closed-loop vacuum conveying system that prevents exposure to ambient air. The material is then dried using desiccant dryers with dew points of -40°C or lower. This is crucial because any residual moisture can cause hydrolysis of the polymer chain, leading to outgassing or "splay" on the part surface—a catastrophic defect for optical or electrical components. The drying process is followed by filtration of the melt within the barrel, using specialized nozzle filters to trap any decomposed or "burned" resin particles before they enter the mold.
Material Selection: The Chemistry of Purity
Not all plastics are suitable for cleanroom molding. The material must possess inherent properties that align with the stringent demands of electronic applications. The most critical parameter is low outgassing, measured by ASTM E595. Outgassing refers to the release of volatile compounds from the polymer when exposed to heat or vacuum. In enclosed electronic assemblies, these volatiles can condense on optical lenses or corrode metal contacts.
Commonly used materials include Liquid Crystal Polymer (LCP), Polyphenylene Sulfide (PPS), and high-temperature Nylons (PPA). These materials offer exceptional dimensional stability and inherent low ionic contamination. For elastomeric seals and gaskets, liquid silicone rubber (LSR) is the gold standard. LSR is unique because it is a two-part, low-viscosity system that cures at high temperatures. Unlike solid silicone, LSR does not require the addition of volatile organic solvents or peroxides, making it exceptionally clean. The molding of LSR in a cleanroom environment is a delicate dance of precise metering, mixing, and injection under controlled pressure, ensuring that no air bubbles or unreacted byproducts remain.
Avoiding Additives and Lubricants
In standard molding, external mold release agents (spray-on lubricants) are common to facilitate part ejection. In cleanroom molding, these are strictly forbidden. The spray releases aerosolized particles and leaves a chemical residue. Instead, the mold steel must be polished to a mirror finish (typically below 8 microinches Ra) and engineered with optimal draft angles. The polymer itself may contain internal lubricants, but these must be carefully selected to be non-migratory and non-ionic. The choice of colorants also matters; heavy metal-based pigments are replaced with organic or ceramic-based pigments that do not leach out during the part’s service life.
Process Engineering and Automation
The mechanical act of molding inside a cleanroom requires specialized presses and automation that minimize human intervention. The injection molding machine itself is typically a servo-hydraulic or all-electric model. All-electric presses are preferred because they have zero hydraulic oil leakage risk and offer superior repeatability in shot size and pressure, which is essential for maintaining consistent packing of the polymer without flashing (excess material bleeding out of the mold).
Robotics and In-Process Inspection
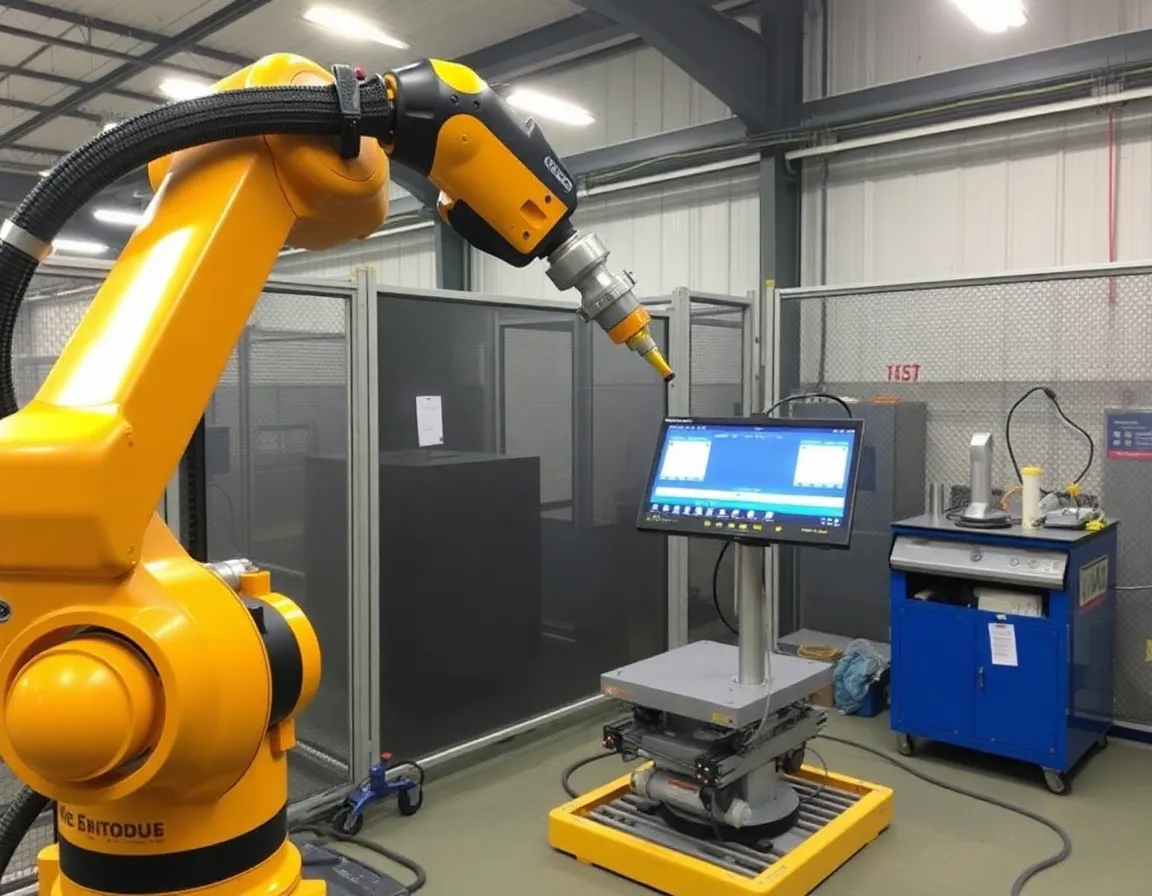
Human operators are the largest source of contamination in any cleanroom, shedding thousands of skin cells per minute. Therefore, the extraction of the molded part from the mold must be performed by a six-axis robotic arm located within the clean zone. The robot places the part directly onto a conveyor that leads to a vision inspection system. This system uses high-resolution cameras and AI-based algorithms to detect surface defects, flash, or contamination in real-time. If a part fails inspection, it is automatically rejected and diverted to a scrap bin without human contact. This closed-loop automation not only ensures purity but also dramatically increases throughput and yield, reducing the cost per unit despite the high capital expenditure.
Post-Molding Operations
Even after ejection, the part is not safe. In many cases, electronic components require secondary operations like deflashing (removing thin plastic remnants) or ultrasonic welding. These operations must also be performed in the cleanroom or in a connected clean annex. For critical applications, the molded parts are subjected to ultrasonic washing with deionized water to remove any ionic residues left from the molding process, followed by vacuum drying and packaging in anti-static, hermetically sealed bags. The packaging step is vital; the bag itself must be certified to be free of amines and silicones that could contaminate the part during storage.
Benefits, Applications, and Best Practices
The investment in electronic cleanroom molding is substantial, but the return on investment is measured in reliability, safety, and brand reputation.
Critical Applications Driving Demand
This technology is not a luxury; it is a necessity for life-saving and high-performance devices.
- Medical Implantable Electronics: Housings for pacemakers, neurostimulators, and hearing aids. These parts must be biocompatible and free from any pyrogens or particulate matter that could cause an immune response.
- Semiconductor Manufacturing Equipment: Wafer carriers, chip trays, and connectors used inside lithography machines. These parts must not outgas hydrocarbons that could fog the precision optics.
- Automotive ADAS Sensors: Housings for LiDAR and radar units. Any contamination on the lens or internal circuitry can cause sensor failure, leading to accidents.
- Optical Transceivers: Precision ferrules and lens holders for fiber-optic communication. Sub-micron dimensional accuracy and zero surface defects are mandatory for signal integrity.
Best Practices for Implementation and Maintenance
To maintain the integrity of the cleanroom and the molding process, consider the following operational protocols:
- Rigorous Gowning Protocol: Operators must wear full cleanroom suits, hoods, boots, and double-gloved. A "sticky mat" and air shower must be passed before entry.
- Preventive Maintenance Scheduling: Molds must be pulled, cleaned, and inspected on a strict schedule. Using an ultrasonic cleaner with a validated detergent is essential to remove carbonized polymer residue from venting slots.
- Environmental Monitoring: Implementing a Particle Measuring System (PMS) that continuously logs airborne particle counts and alerts management to any spikes is non-negotiable. This data must be archived for traceability.
- Raw Material Vetting: Ensure that your resin supplier provides a Certificate of Analysis (CoA) specifically stating ionic cleanliness and outgassing properties. Never accept generic "off-the-shelf" resin.
Conclusion: The Future of High-Stakes Manufacturing
Electronic cleanroom molding is far more than a manufacturing process; it is a philosophy of meticulous control. As the world moves toward smaller, faster, and more integrated devices—from 5G infrastructure to implantable bio-sensors—the margin for error becomes negligible. The companies that master this craft do not simply mold plastic; they engineer absolute purity. By understanding the environmental controls, selecting the correct materials, and embracing automation, manufacturers can deliver components that function flawlessly in the harshest conditions. The guide above provides the foundational knowledge required to approach cleanroom molding with the seriousness it deserves, ensuring that the precision inside the part matches the precision of the environment in which it was born.