Polyetheretherketone (PEEK)

Polyetheretherketone (PEEK) is a premier semi-crystalline high-performance polymer renowned for its metal-like mechanical strength, extreme chemical resistance, and high continuous service temperature (up to 260°C). Jucheng Precision, holding ISO 9001, ISO 13485, and IATF 16949 certifications, specializes in high-temperature PEEK injection molding (including carbon/glass-filled and medical implant grades). With 35+ advanced molding presses (50-650T) equipped with high-temperature barrels and oil-heated tooling controllers, we ensure optimal material crystallization. We offer free DFM analysis within 24 hours to optimize thermal profiles, delivering zero-defect implant and aerospace parts verified by Zeiss CMM inspection.

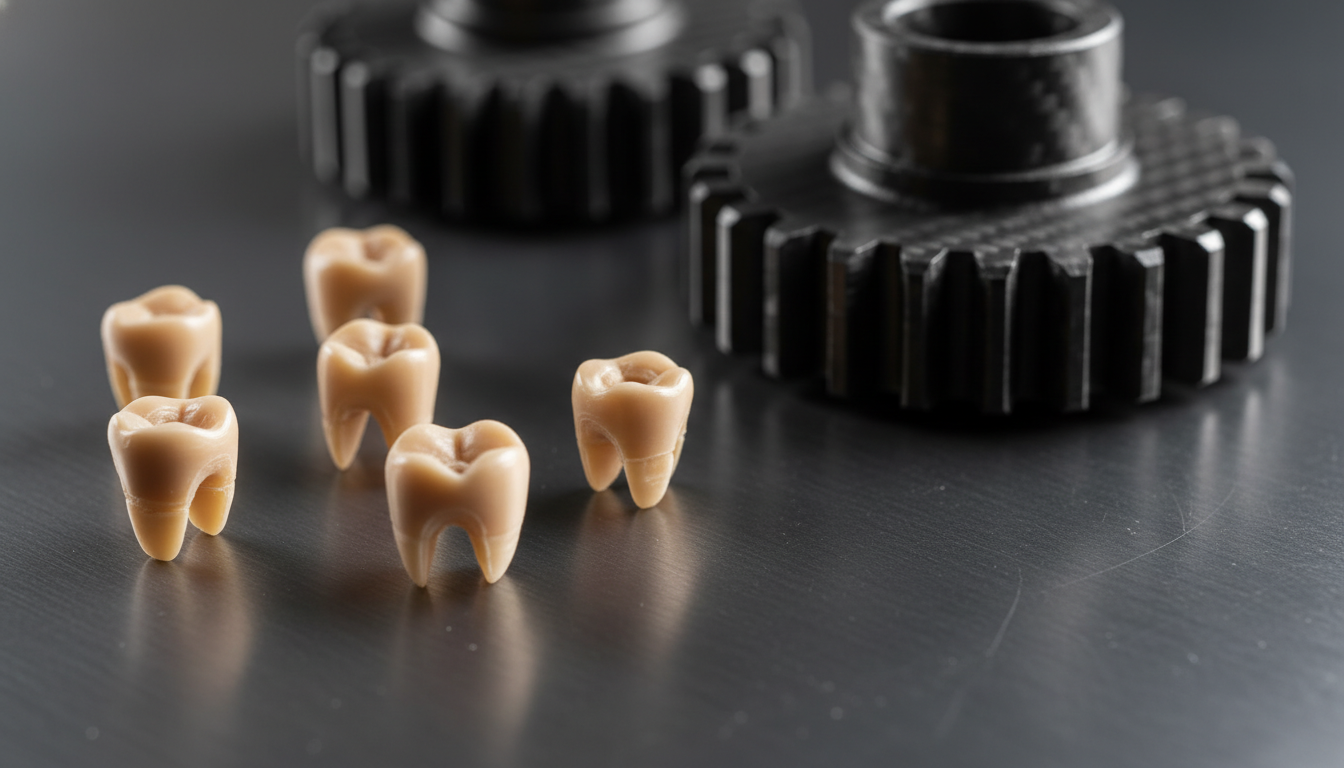
Precision-injection-molded-beige-medical-PEEK-implants-and-dark-grey-carbon-filled-PEEK-aerospace-components-1

Our available materials

PEEK-Evonik Vestakeep i4G

Evonik VESTAKEEP i4 G is a natural-colored, high-viscosity PEEK resin developed for medical applications. Review the manufacturer product information, base-resin property references and processing guidance below. Finished-part suitability and the required manufacturing and quality records must be confirmed for the specific project.

READ MORE

PEEK-Solvay KetaSpire KT-820

Sustaining dynamic load-bearing fatigue and chemical insolubility inside aggressive deep-well downhole or clinical sterilization environments demands an ultra-stiff, high-viscosity polymer, which Syensqo’s KetaSpire KT-820 delivers through its unreinforced, low-flow polyetheretherketone matrix. Boasting a density of 1.30 g/cm³ and a melt flow rate of 3.0 g/10 min, this highly crystalline grade provides outstanding creep resistance and best-in-class fatigue life compared to high-flow PEEK grades. Jucheng Precision, operating under ISO 13485 and IATF 16949 certified frameworks, specializes in high-temperature molding of KetaSpire KT-820. Supported by high-temperature ceramic heater bands and oil-heated tooling controllers, we ensure complete semi-crystalline phase alignment, delivering structural components verified by Zeiss CMM.

READ MORE

PEEK-Victrex PEEK 150G

Achieving high mechanical integrity and chemical resistance in complex, thin-walled geometries requiring long flow lengths demands an ultra-flow super-polymer, which Victrex’s PEEK 150G delivers through its unreinforced, low-viscosity polyetheretherketone matrix. Boasting a melt viscosity of 130 Pa·s at 400°C and a melting point of 343°C, this easy-flow grade is designed to fill sub-millimeter profiles without sacrificing the high tensile strength (105 MPa) of pure PEEK. Jucheng Precision, under ISO 13485 and IATF 16949 medical and automotive frameworks, specializes in molding Victrex 150G. Using S136 stainless steel molds, we control its high crystallization variables to deliver flash-free micro-gears and thin-wall connectors verified by Zeiss CMM.

READ MORE

PEEK-Victrex PEEK 450CA30

Replacing aerospace-grade titanium and high-strength aluminum alloys in severe, load-bearing dynamic mechanisms without adding weight requires a polymer of unmatched specific stiffness, which Victrex’s PEEK 450CA30 delivers through its 30% carbon fiber reinforced, semi-crystalline polyetheretherketone matrix. Boasting a density of 1.40 g/cm³ and an extreme heat deflection temperature (HDT) of 335°C, this high-performance composite provides a massive flexural modulus of 21,000 MPa alongside inherent electrostatic dissipation (ESD) and near-zero wear. Jucheng Precision, operating under IATF 16949 and ISO 13485 certified frameworks, specializes in molding PEEK 450CA30. Supported by ceramic heater bands and pressurized oil mold heating controllers, we control its anisotropic shrink variables to prevent warpage, delivering structurally flawless parts verified by Zeiss CMM.

READ MORE

PEEK-Victrex PEEK 450G

Victrex PEEK 450G is an unreinforced, semi-crystalline PEEK grade for injection molding and extrusion. Review its March 2026 manufacturer data, property-specific temperature ratings and processing conditions below. Part suitability, size and inspection requirements are confirmed against the drawing and application.

READ MORE

PEEK-Victrex PEEK 450GL30

Victrex PEEK 450GL30 is a 30% glass-fiber-reinforced PEEK for applications where stiffness and dimensional behavior matter. This page connects the manufacturer datasheet to molding decisions: directional shrinkage, mold temperature, drying and part-level validation. HDT is a test result, not a continuous service-temperature guarantee. Send the drawing, operating conditions and quantity for a molding review.

READ MORE

Comprehensive PEEK Grades We Process

We process extreme-performance PEEK resins from globally recognized compounders, specialized for severe aerospace, medical implant, and automotive wear environments:

PEEK Material Class Typical Brand & Grade Key Characteristics & Advantages
Unreinforced PEEK • Victrex PEEK 450G / 150G
• Solvay KetaSpire KT-820 / KT-880 NT
• Evonik Vestakeep 4000G
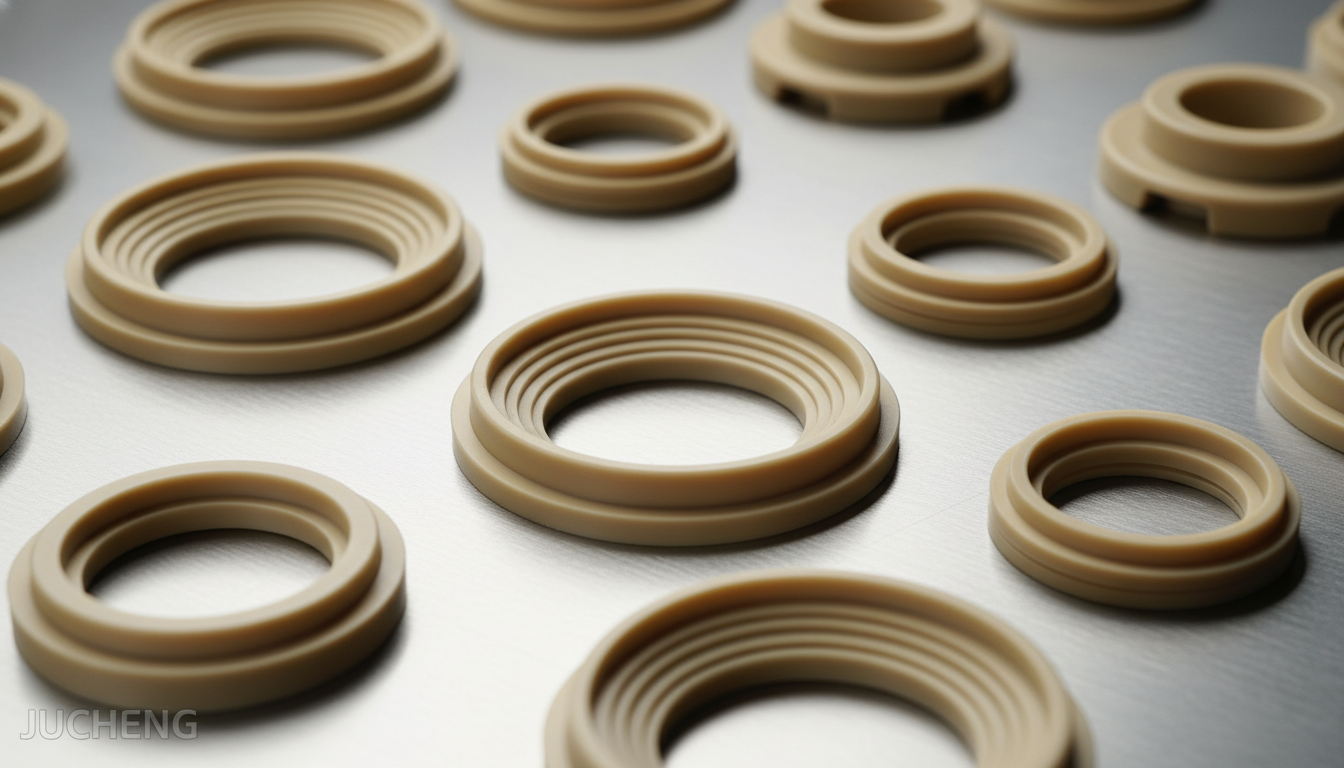
Standard and high-flow grades offering exceptional ductility, chemical resistance, and natural flame retardancy (UL 94 V-0). Applied in seal rings, fluid manifolds, and semiconductor wafer carriers.
Fiber Reinforced (GF/CF) • Victrex PEEK 450GL30 (30% GF) / 450CA30 (30% CF)
• Solvay KetaSpire KT-820 GF30 / KT-820 CF30
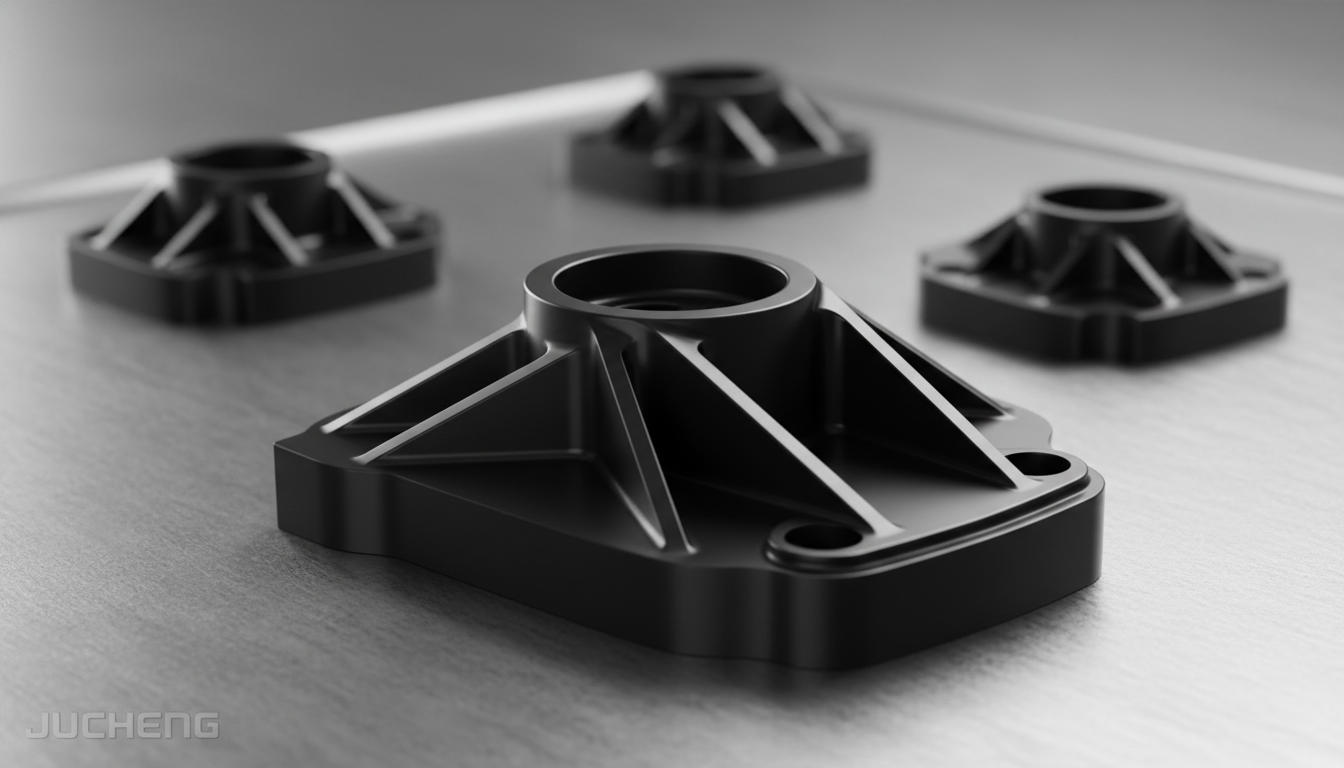
Reinforced with glass or carbon fibers to achieve metal-like stiffness, extremely low thermal expansion, and a Heat Deflection Temperature (HDT) up to 315°C. Crucial for aerospace brackets and structural gears.
Biocompatible / Implant • Evonik Vestakeep M2G / M4G
• Evonik Vestakeep i4G (Implant Grade)
• Solvay Zeniva PEEK
Specifically formulated and purified for long-term implantable medical devices. Highly biocompatible, bone-mimicking modulus, and completely transparent to X-rays. Used in spinal cages and dental implants.

Applicable Molding Processes for Polyetheretherketone (PEEK)

PEEK’s extreme melt temperature and high thermal load require specialized, industrial-grade process architectures:

Molding Process Process Suitability & Application
Standard Injection Molding Excellent. Configured with high-temperature oil controllers to mold aerospace thrust washers, semiconductor carriers, and chemical pump gears.
Micro Injection Molding Excellent. Highly optimized for manufacturing sub-millimeter dental healing caps, surgical spinal components, and micro-scale aerospace connectors.
Insert Molding Good. Allows precision encapsulation of specialized high-temperature metal alloy bushings or threaded terminals directly inside structural PEEK frames.

Polyetheretherketone (PEEK) Manufacturing & Tooling Guide

PEEK is processed at extreme temperatures near 400°C. Inadequate heating controls will freeze the melt instantly, leading to incomplete crystallization, internal stresses, and mechanical weakness:

  • Pre-Drying: PEEK must be thoroughly dried to prevent hydrolytic splay. We dry the raw polymer in desiccant hopper dryers at 150°C (302°F) for 3–4 hours, keeping internal moisture levels strictly below 0.02%.
  • Extreme Melt Temperature: Melting requires specialized machines with ceramic heater bands. Processing temperatures are strictly managed between 360°C and 400°C (680°F to 752°F).
  • Critical Mold Temperature: To secure proper semi-crystalline alignment (which gives PEEK its beige opaque look and strength), mold temperatures must be continuously maintained at 160°C–200°C (320°F to 392°F) using pressurized oil-heating controllers. Cold molds cause the material to freeze amorphous, turning translucent brown and structurally weak.
  • Specialized Tool Steel: Due to extreme injection pressures and thermal loads, Jucheng’s tooling division uses hardened tool steel (H13 or S136) designed with robust draft angles (minimum 1.5° to 2.0°) and reinforced ejector layouts.

Key Application Industries for Molded PEEK Parts

  • Medical & Dental Devices (ISO 13485 Certified): Spine fusion cages, dental healing caps, surgical trial implants, orthopedic targeting blocks, and analytical chromatography connectors.
  • Aerospace & Semiconductor: Wafer carriers, chemical etching rings, vacuum chamber connectors, lightweight engine brackets, and cable clamps.
  • Automotive Powertrains (IATF 16949 Certified): High-wear thrust washers, automatic transmission seal rings, steering column gears, and specialized sensor housings.
  • Oil & Gas Exploration: Subsea electrical connectors, deep-well pump vanes, chemical-resistant seal rings, and specialized structural packer elements.

Material Properties

Density (Unreinforced) 1.30 - 1.32 g/cm³
Density (30% CF) 1.40 - 1.44 g/cm³
Tensile Strength at Yield (Unreinforced) 95 - 110 MPa
Tensile Strength at Yield (30% CF) 190 - 240 MPa
Elongation at Break 10 - 45 %
Flexural Modulus (Unreinforced) 3,700 - 4,200 MPa
Flexural Modulus (30% CF) 11,000 - 14,000 MPa
Izod Impact Strength (Notched, 23°C) 50 - 90 J/m
Melting Temperature 343 °C
Heat Deflection Temperature (HDT @ 0.45 MPa) 160 - 315 °C
Linear Mold Shrinkage 0.1 - 1.5 %
Dielectric Strength 20 - 24 kV/mm
Volume Resistivity 1.0E+16 Ohm·cm
Maximum Part Size 800 x 600 mm
Minimum Part Size 0.5 x 0.5 mm