
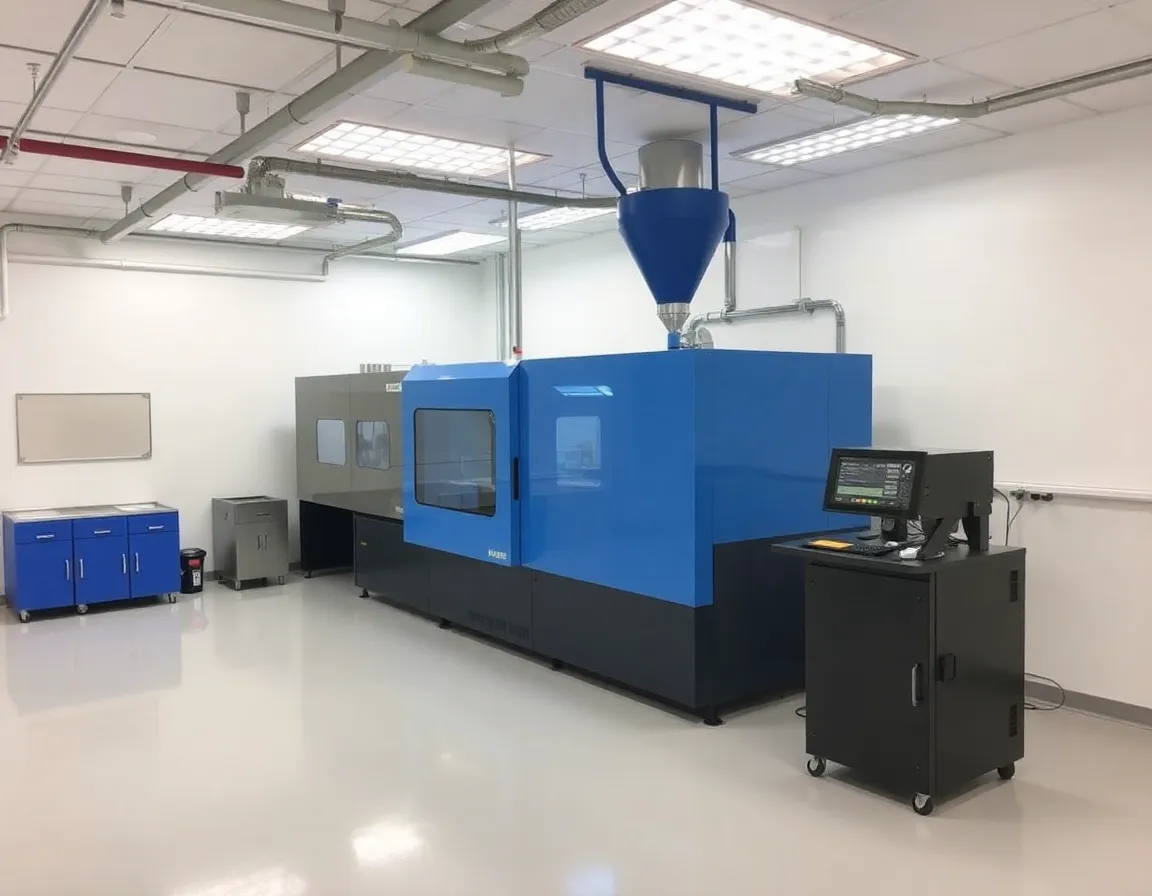
정밀성과 순수성의 중요한 교차점
현대 의학의 영역에서 장치가 조립되는 환경은 장치 자체만큼이나 중요합니다. 단 하나의 미세한 먼지 입자, 우발적인 생물학적 포자, 또는 정전기 방전이 임플란트를 손상시키거나 무균 배치를 무효화하거나 진단 도구를 부정확하게 만들 수 있습니다. 의료용 클린룸 조립 은 단순한 제조 단계가 아니라 공학, 미생물학, 인간 행동 과학을 결합하여 의료 혁신을 위한 통제된 성역을 만드는 정교한 학문입니다. 이 기사는 세계적 수준의 클린룸 운영을 평범한 운영과 차별화하는 7가지 전문 비결을 공개하여 생명을 구하는 제품이 가능한 가장 엄격한 조건에서 제작되도록 보장합니다.
Unlike standard industrial assembly, medical cleanroom assembly operates under a strict regulatory framework, primarily governed by ISO 14644 standards and Good Manufacturing Practices (GMP). The goal is to control airborne particulate concentration and, in many cases, biological contaminants. However, the true mastery lies not just in the hardware—the HEPA filters and airlocks—but in the nuanced protocols that govern every action inside the white-walled environment. Here, we decode the seven non-negotiable secrets that drive successful medical device assembly.
Secret #1: Mastering Airflow Dynamics (The Unseen Architecture)
The most common misconception about a cleanroom is that "clean" means "sterile." In reality, it means controlled contamination. The first secret to successful assembly is understanding that air is the primary vehicle for contamination. Professionals don’t just rely on air filters; they engineer the airflow to push particles away from the product.
Unidirectional Flow vs. Turbulent Flow
For critical medical assembly, unidirectional (laminar) airflow is paramount. Air moves in parallel lines at a constant velocity, typically 0.45 m/s ± 20%, sweeping contaminants away from the work zone. The secret is in the positioning: the assembly work must occur "upstream" of the operator, meaning the operator’s breath and body particles are carried away, not over the product. In contrast, turbulent flow rooms (ISO 7 and below) rely on dilution, which is acceptable for less sensitive components but risky for implantable devices.
Professionals also know that airflow is disrupted by physical obstructions. A single monitor, a misplaced stool, or a stack of documents can create eddies that trap particles. Therefore, the assembly layout is designed around the airflow path, not the convenience of the worker. Every table is perforated, every light fixture is flush, and every utility line is sealed to prevent air from bypassing the filtration system.
Secret #2: The Human Factor – Gowning as a Ritual, Not a Routine
Humans are, by far, the largest source of contamination in a cleanroom. A sedentary person sheds approximately 100,000 particles per minute. The second secret is treating the gowning procedure as a sacred, choreographed ritual. It is not about wearing a "bunny suit"; it is about creating a physical barrier that contains the human micro-environment.
Sequential Gowning Protocol
Master assemblers follow a strict sequence that minimizes particle generation. The process usually involves:
- Pre-cleaning: Removing all cosmetics, jewelry, and personal electronics before entering the change room.
- Air Shower: A high-velocity jet that removes loose particles from the undergarments.
- Bottom-to-Top Dressing: Donning the coverall, then the boots, then the hood, and finally the gloves and goggles. The critical rule is to avoid touching the outside of the suit with bare hands.
- Final Rinse: A second air shower and a visual check using a mirror to ensure no skin is exposed.
The secret here is glove hygiene. Gloves are sterilized with 70% IPA (isopropyl alcohol) immediately before handling any product. This is not just for chemical cleanliness; the friction of wiping creates a static charge that actually attracts particles to the glove surface, preventing them from falling onto the device.
Secret #3: Material Science and Outgassing Control
Not all materials are created equal inside a cleanroom. The third secret involves a deep understanding of outgassing and particle shedding. Many plastics, adhesives, and lubricants release volatile organic compounds (VOCs) that can condense on sensitive optical surfaces or alter the chemical composition of a drug-eluting coating.
Choosing Low-Particulate Materials
Medical assembly professionals exclusively specify materials that are inherently low-shedding. For example:
- Silicone-free lubricants are used to prevent surface contamination that can cause delamination.
- Wipe materials are made of knitted polyester or non-woven cellulose, never cotton, as cotton fibers are long and abrasive.
- Pen and paper are forbidden; instead, laser-etched metal tags and solvent-resistant labels are used.
The true secret is pre-conditioning. In high-end facilities, components are "baked out" in a vacuum oven prior to assembly to drive off absorbed moisture and VOCs. This pre-treatment ensures that the final product does not release contaminants over its lifetime, which is critical for hermetically sealed implants.
Secret #4: Electrostatic Discharge (ESD) – The Silent Killer
While particles are visible under a microscope, electrostatic discharge is invisible until it destroys a microchip. In medical devices, which increasingly contain complex electronics (e.g., insulin pumps, neurostimulators), ESD can cause latent failures that manifest months after implantation. The fourth secret is total ESD control, which goes beyond just wearing a wrist strap.
Conductive Work Surfaces and Ionization
All work surfaces in a medical cleanroom assembly station must be conductive (typically dissipative laminate) and grounded to a common point. However, the master secret is the use of ionizers. Because cleanrooms have low humidity (often below 40% RH) to reduce bacterial growth, static charges build up rapidly. Ionizers flood the air with positive and negative ions that neutralize the charge on insulators (like the plastic housing of a device).
Professionals also know that ESD safety is about speed and contact. Assemblers are trained to handle components by their edges, never touching conductive pins. They use vacuum pick-up tools with conductive tips, and all packaging materials must be static-shielding bags, not just anti-static bags. This level of discipline prevents the "sudden death" of electronics that would otherwise pass initial testing but fail in the field.
Secret #5: Real-Time Environmental Monitoring (Data over Guesswork)
The fifth secret is a shift from reactive to predictive contamination control. Traditional methods involved taking settle plates and swabbing surfaces at the end of a shift. Master facilities use continuous, real-time particle counters (both airborne and in liquids) that feed data into a central SCADA system. This provides immediate feedback—if a particle spike occurs at 10:32 AM, the system alerts the supervisor instantly, allowing for a root-cause analysis before the batch is ruined.
Trending and Alert Limits
The secret is not just having sensors but knowing how to interpret the data. Professionals establish three levels of limits:
- Action Limit: If particle count exceeds this, the assembly must stop immediately, and the product is quarantined.
- Alert Limit: A warning that the environment is trending toward the action limit, prompting a check of HEPA filters or a review of operator behavior.
- Baseline Trend: Analyzing weekly data to identify slow degradation in air handling units before they fail.
This data-driven approach allows for proactive maintenance, such as pre-filter replacement, rather than waiting for a regulatory audit to fail. It also provides the documentation required for regulatory submissions, proving that the environment was consistently within specification throughout the entire production run.
Secret #6: Process Isolation and Single-Piece Flow
Batch production is the enemy of cleanliness. The sixth secret is to design the assembly line for single-piece flow with physical barriers between process steps. Instead of moving a tray of 100 devices from station to station (which allows contamination to accumulate on the tray), each device is assembled in a dedicated, isolated module.
The Use of Isolators and RABS
For high-risk products (e.g., prefilled syringes or ophthalmic solutions), master assembly uses Restricted Access Barrier Systems (RABS) or full isolators. These are glove-box-like enclosures that provide a physical barrier between the operator and the product. The interior is continuously flushed with sterile air or nitrogen, and the operator interacts via long-sleeved gloves sealed to the wall. This reduces the human contamination factor by 99%.
Even for less critical devices, the secret is minimizing product travel. The assembly line is organized in a U-shape or a straight line where the product never touches a non-clean surface. Conveyor belts are avoided because they grind and create particles; instead, gravity-fed slides or manual hand-off using sterile tweezers are preferred.
Secret #7: Validation and Human Training (The Psychological Edge)
The final secret is arguably the most overlooked: the human mind. A cleanroom is a stressful environment—restrictive, cold, and monotonous. The seventh secret is investing heavily in behavioral training and psychological conditioning. It is not enough to tell a technician what to do; they must understand why they do it.
Simulation and Error-Proofing (Poka-Yoke)
Master facilities use virtual reality (VR) simulators to train assemblers on the exact motions required before they ever step inside the real cleanroom. This reduces the "learning curve" contamination events. Additionally, they implement Poka-Yoke (mistake-proofing) mechanisms:
- Smart tools: Torque wrenches that log data and lock out if the correct torque is not achieved.
- Vision systems: Cameras that automatically inspect for missing components or flipped O-rings.
- Color-coded zoning: Floors and walls are painted in different shades to signal transition zones, preventing accidental cross-contamination.
Furthermore, the secret is in ergonomic design. If a technician has to stretch or bend uncomfortably, they will sweat, shed more particles, and make mistakes. Adjustable workstations, anti-fatigue mats, and scheduled micro-breaks (outside the cleanroom) are essential to maintaining the high level of focus required for precision assembly.
Applications and Benefits of Master-Level Assembly
Implementing these seven secrets yields tangible benefits across the medical field. The most obvious application is in the production of implantable devices (orthopedics, pacemakers), where a single particle can cause inflammation or rejection. It is also critical for combination products (drug-device hybrids) like auto-injectors, where the drug must remain free of leachables from the device materials. Finally, it is vital for diagnostic consumables, such as microfluidic chips, where a dust particle can clog a channel and produce a false negative result.
The benefits are clear: higher yield (fewer rejected batches), lower liability (reduced risk of patient harm), and faster regulatory approval (because the data proves consistent quality). Moreover, a well-designed cleanroom assembly process reduces operator fatigue, leading to lower turnover rates and a more experienced workforce.
Conclusion: The Pursuit of Invisible Perfection
Mastering medical cleanroom assembly is not about buying the most expensive filters or the largest room. It is about a holistic philosophy that respects the invisible threats—air movement, human shedding, static charge, and material chemistry. By implementing the seven secrets outlined above—airflow mastery, ritualized gowning, material selection, ESD control, real-time monitoring, process isolation, and human psychological training—manufacturers can achieve a level of precision that borders on art.
In an industry where the margin for error is zero, these secrets are not optional enhancements; they are the baseline for survival. The devices that emerge from these controlled environments carry the silent promise of safety, born from the relentless pursuit of invisible perfection. As technology advances towards nano-scale medicine, the importance of these cleanroom disciplines will only grow, solidifying their role as the unsung heroes of modern healthcare.