
電気自動車(EV)のバッテリーパックには、堅牢な熱管理、電気絶縁、耐衝撃性のある構造が求められます。.
重い金属製エンクロージャから高強度エンジニアリングプラスチックへの移行は、自動車パック設計における大きな進化を表しています。.
この技術ガイドでは、信頼性の高いエンクロージャを製造するために不可欠な金型設計、DfM(設計製造性)の考慮事項、および高度なポリマー加工技術について詳しく説明します。.
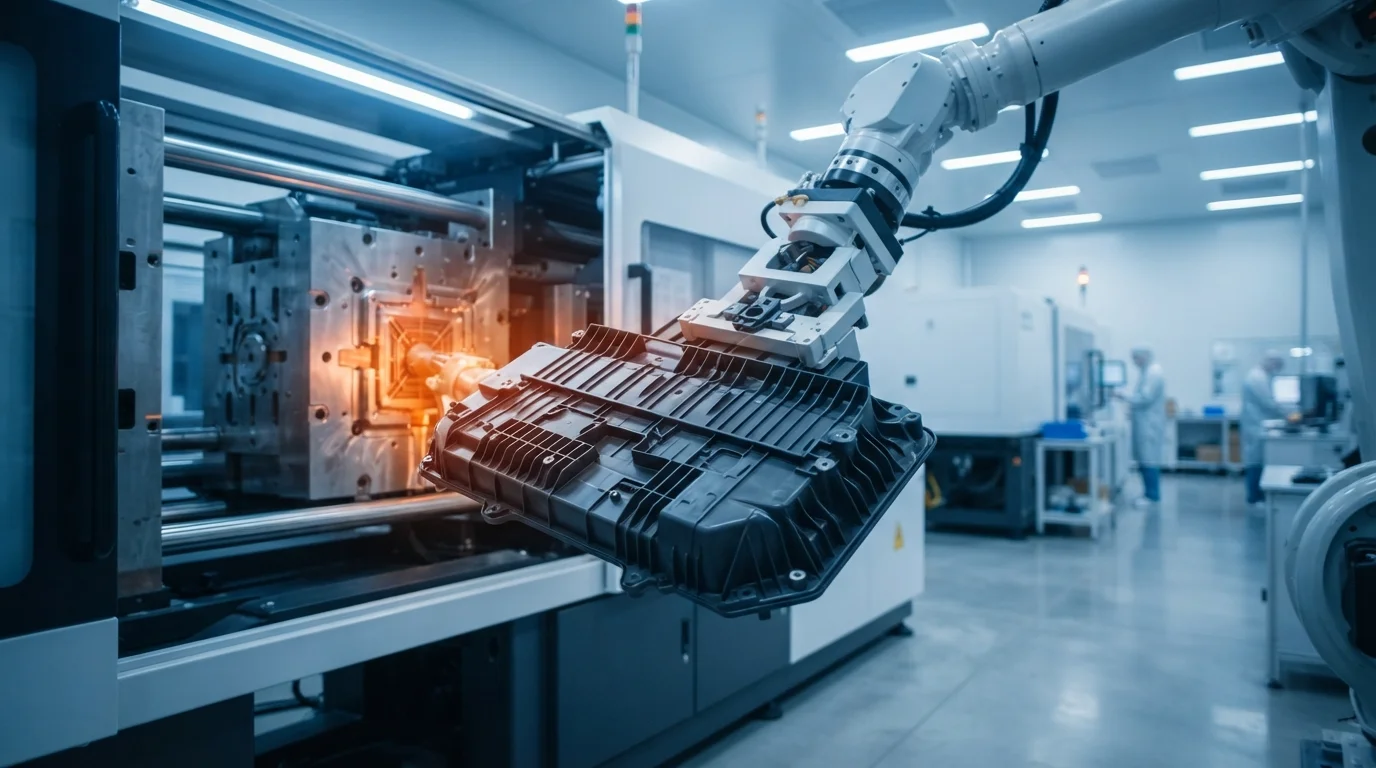
JUCHENG射出成形は、カスタム金型と精密プラスチック成形を専門とする高級カスタム受託製造施設として運営されています。.
当社は標準品や既製のバッテリーボックスを小売りしておりません。すべてのコンポーネントは、お客様から提供された3D CADモデルから設計され、厳しい性能仕様を満たすように作られています。.
試作段階から多キャビティの量産への移行まで、当施設はIATF 16949およびISO 13485認証に裏打ちされたカスタマイズされた製造サポートを提供します。.
目次
EVバッテリーエンクロージャにカスタム射出成形が重要な理由
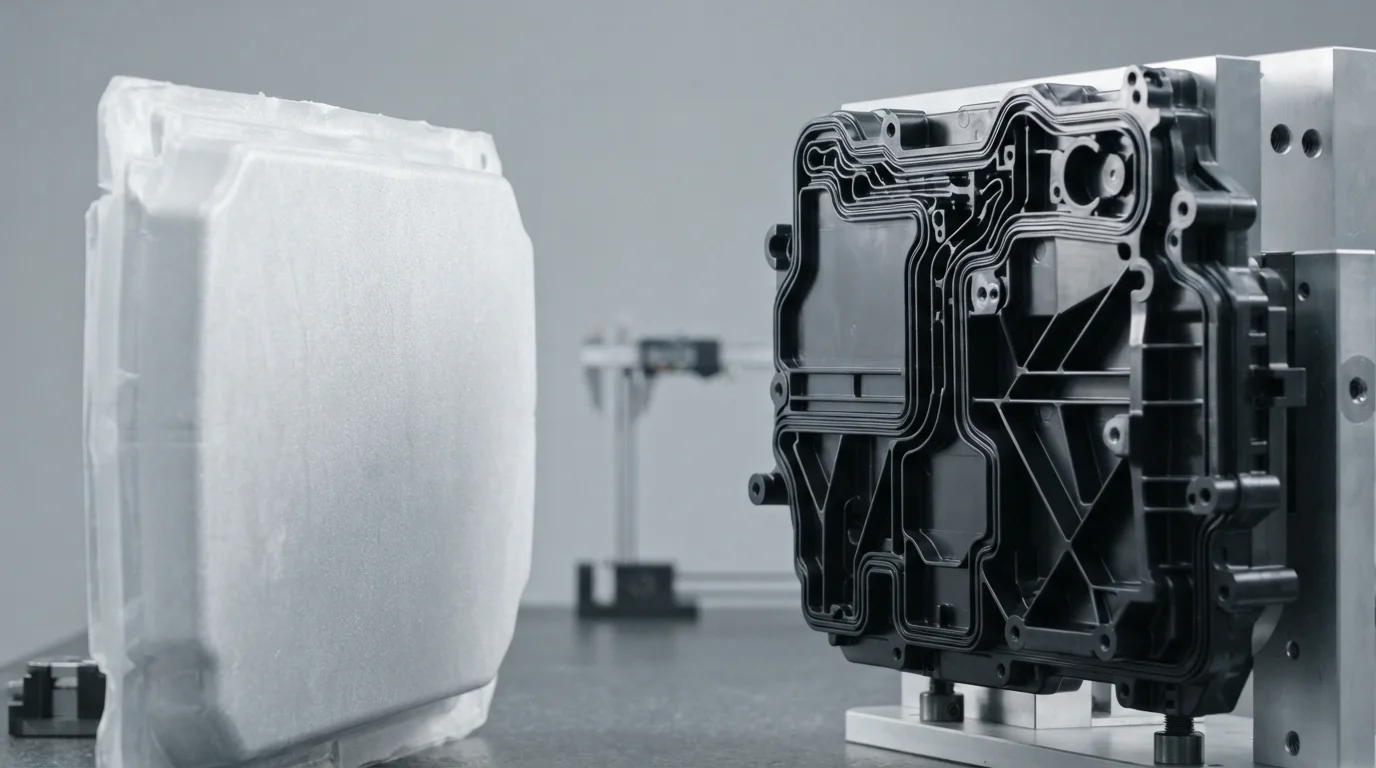
堅牢なエンジニアリング カスタムEV用プラスチックバッテリーハウジング requires an understanding of structural integration and tight tolerance control.
Traditional metallic casings are heavy and require secondary insulation liners to prevent short circuits.
By utilizing high-performance polymers, engineers can mold complex geometries, internal features, and functional mounts directly into a single unified part.
Consolidating components in this manner reduces bill-of-materials costs, eliminates secondary assembly steps, and shaves critical weight off the vehicle chassis.
Integrating internal components is crucial for protecting individual lithium-ion cells from thermal runaway propagation.
Seamless integration of 電気自動車バッテリーセルホルダー directly within the structural walls of the main housing prevents vibrational wear on cell terminals.
Furthermore, incorporating thin, high-insulation 電気自動車バッテリースペーサー prevents thermal runaway from leaping between pouch or prismatic cell modules.
Such configurations optimize space utilization inside the battery pack, allowing higher energy density while maintaining structural integrity during mechanical impacts.
Compared to alternative processing methods like sheet metal stamping or thermoforming, injection molding provides superior repeatability and dimensional accuracy.
High-pressure injection molding forces molten plastic into precision-machined cavities, producing parts with zero draft variations and highly consolidated molecular structures.
This is especially crucial for molding elastomeric sealing channels and perimeter tongue-and-groove joints that prevent moisture and dust from breaching the battery module.
経験豊富な製造専門家と提携することで、カスタム部品が厳格な自動車安全基準に適合することが保証されます。.
材料と難燃性基準(UL94 V-0)
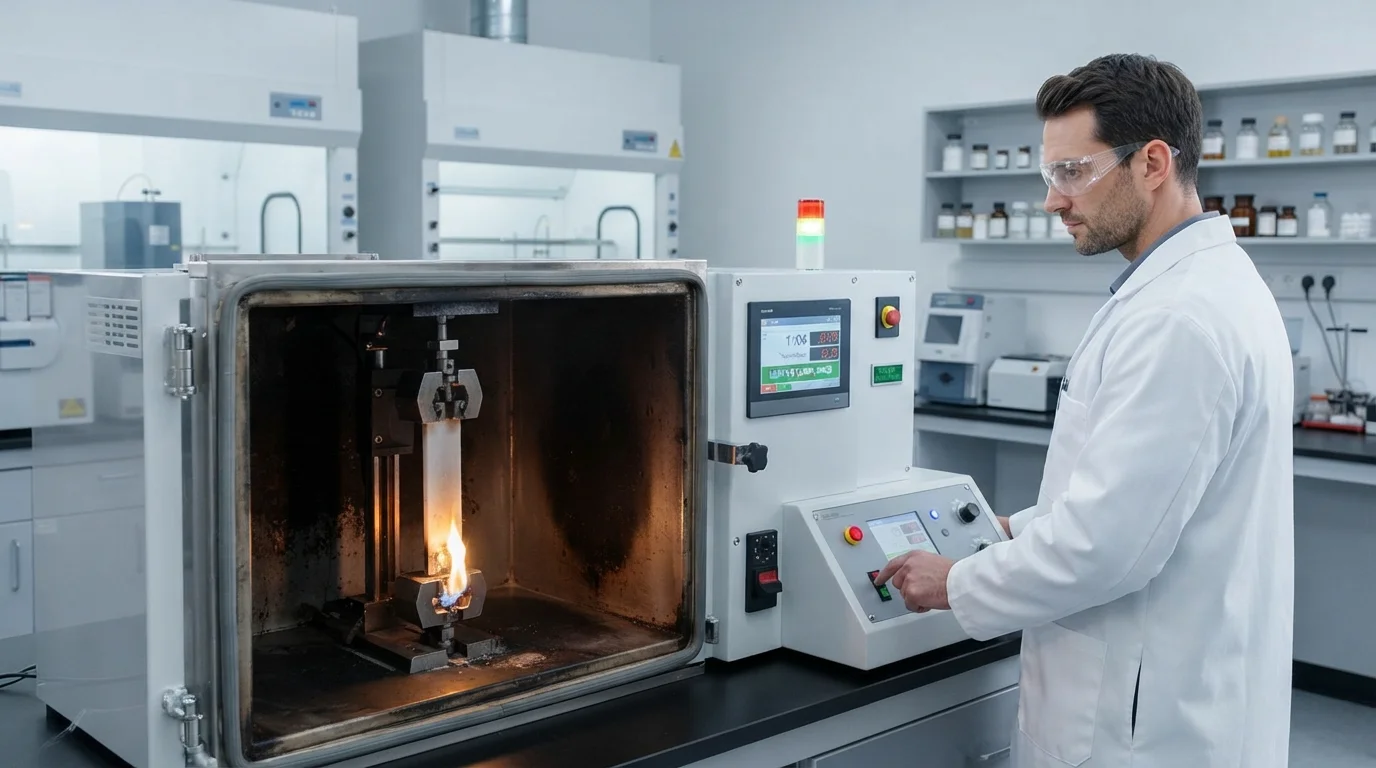
特殊な開発 カスタムEV用プラスチックバッテリーハウジング 高性能熱可塑性プラスチックに依存しています。.
エンジニアは、衝撃強度、バッテリー電解液に対する耐薬品性、熱変形温度、長期クリープ耐性のバランスを取る必要があります。.
したがって、 EVバッテリーモジュール用の射出成形Bayblend FR3010 を使用することで、-30°Cまでの優れた衝撃性能を確保し、1.5mm厚でUL94 V-0難燃性定格を達成します。.
この非晶性ポリカーボネートとアクリロニトリル・ブタジエン・スチレンのブレンドは、予測可能な収縮率特性を提供し、平坦で反りのないカバーの製造を容易にします。.
高電圧バッテリーエンクロージャのコア材料性能要件には以下が含まれます:
- 熱安定性—エンジニアリングプラスチックは、100°Cを超える連続動作温度下で構造的完全性を維持する必要があります。.
- 難燃性—厳格なUL94 V-0定格を達成することで、火災の伝播を防ぎ、プラスチック部品を数秒以内に自己消火させます。.
- 絶縁耐力—High volume resistivity prevents electrical arcing between battery cells and the outer chassis.
- 耐衝撃性—Robust physical properties safeguard the delicate lithium cell matrix from debris puncture during dynamic driving.
Similarly, manufacturing 難燃性PC ABSバッテリー筐体 ensures structural rigidity while providing reliable electrical insulation.
When high mechanical rigidity is required to withstand extreme drop tests, glass-fiber reinforced polymers represent the optimal choice.
For instance, choosing 射出成形Lexan 940Aバッテリーフレーム offers exceptional flame retardancy coupled with the dimensional stability required for interlocking prismatic cell matrices.
This polycarbonate resin maintains its physical properties under constant thermal loads, preventing cell migration during rapid charging and discharging cycles.
Safety compliance remains non-negotiable for all high-voltage automotive components.
Therefore, specifying UL94 V-0 flame retardant plastic cell carrier injection molding guarantees that the polymer will self-extinguish within 10 seconds of a flame application, preventing catastrophic thermal fire propagation.
Structural trays also demand extreme load-bearing capabilities.
Indeed, handling ガラス繊維強化ポリアミド製バッテリートレイの製造 presents challenges with warpage due to the differential shrinkage between the transverse and parallel glass fiber orientations.
Our mold design team overcomes this by optimizing gate locations and using balanced hot runner systems to distribute fiber alignment evenly across the mold cavity.
| 材料グレード | ポリマータイプ | 引張強さ (MPa) | HDT @ 1.82 MPa(°C) | 難燃性等級 |
|---|---|---|---|---|
| Bayblend FR3010 | PC + ABS ブレンド | 60 | 110 | UL94 V-0 |
| Lexan 940A | ポリカーボネート(PC) | 65 | 125 | UL94 V-0 |
| PA66-GF30 (FR) | ポリアミド66 + 30% GF | 150 | 240 | UL94 V-0 |
| TPV (70A-40D) | 熱可塑性加硫ゴム | 8 – 15 | 該当なし (エラストマー) | UL94 HB / V-0 |
複雑なバッテリー形状に対応する高度な金型加工能力
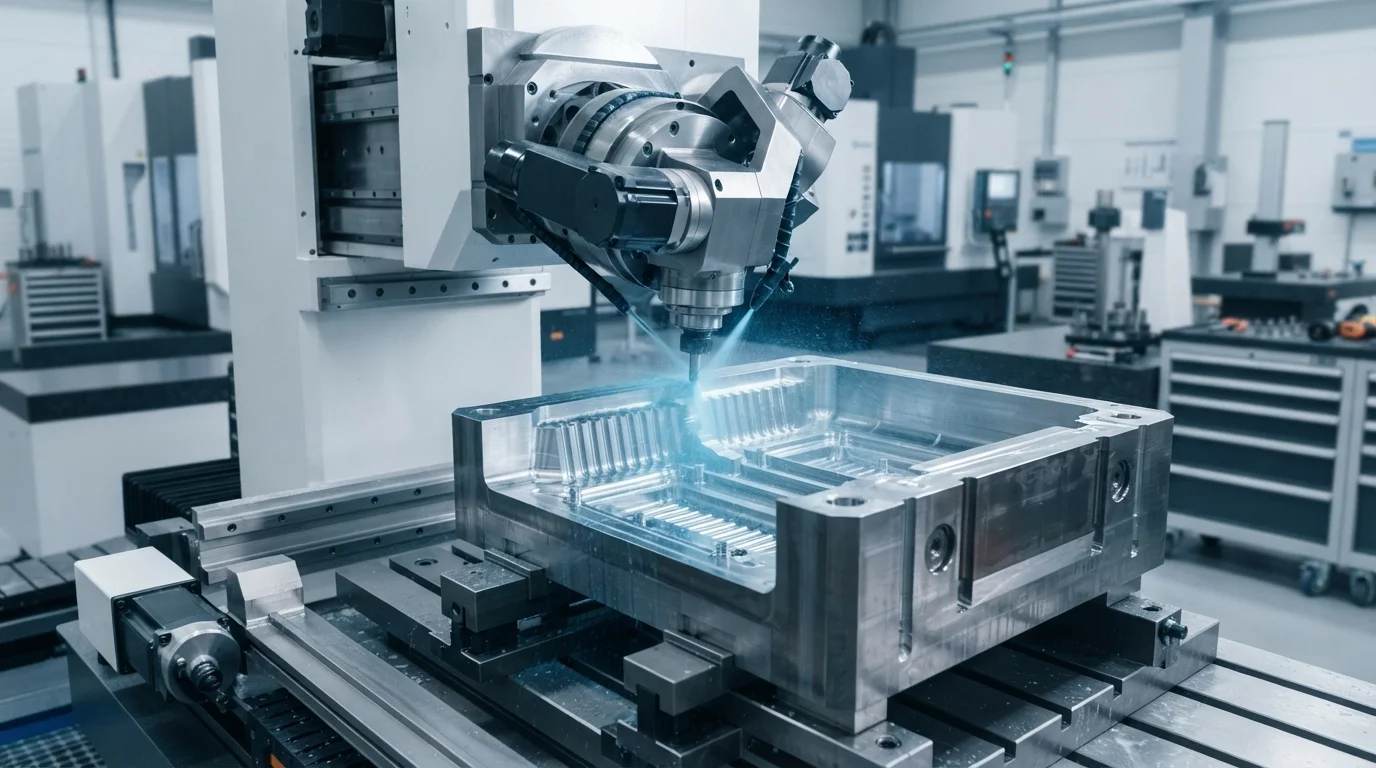
金型設計は、カスタム部品の長期的な品質、平坦度、および構造的信頼性に直接影響を与えます。.
当社の二重認証施設では、社内の5軸CNC工作機械25台以上を活用し、焼入れされたH13またはS136工具鋼から精密な金型コアを切削加工します。.
焼入れ鋼は、腐食性の高い難燃剤や研磨性の高いガラス繊維を扱う際に、ピッチングや急速な寸法摩耗を起こさずに対応するために必須です。.
成形プロセス中、金型鋼に統合された最適化されたコンフォーマル冷却チャネルにより、サイクルタイムを最大30%短縮し、均一な放熱を確保して、成形後の反りを防ぎます。.
One prominent technique involves overmolding high-voltage conductive elements directly inside the structural shell.
Specifically, employing insert molding busbars in EV battery covers minimizes assembly errors and prevents environmental moisture from leaking into critical high-voltage contact areas.
This requires incredibly tight tooling shut-off tolerances to prevent plastic flash from flowing onto the active contact surfaces of copper or aluminum busbars.
Our precise tooling designs utilize spring-loaded core pins and real-time cavity pressure sensors to prevent crushing the metal inserts during mold clamp-up.
Moisture and dust ingress must be prevented to avoid short-circuiting expensive lithium cell modules.
Thus, performing カスタム成形熱可塑性加硫ゴムTPVバッテリーガスケット ensures that our カスタムEV用プラスチックバッテリーハウジング achieve dynamic sealing profiles directly integrated onto the rigid PC/ABS cover.
Achieving this dual-material integration is possible through advanced multi-shot injection molding or custom overmolding processes, completely eliminating the labor-intensive hand-application of adhesive foam strips.
Such multi-material integrations remain a hallmark of automotive-grade manufacturing, providing robust protection against IP67 and IP69K moisture standards.
DfM Analysis & Complete Turnkey Services
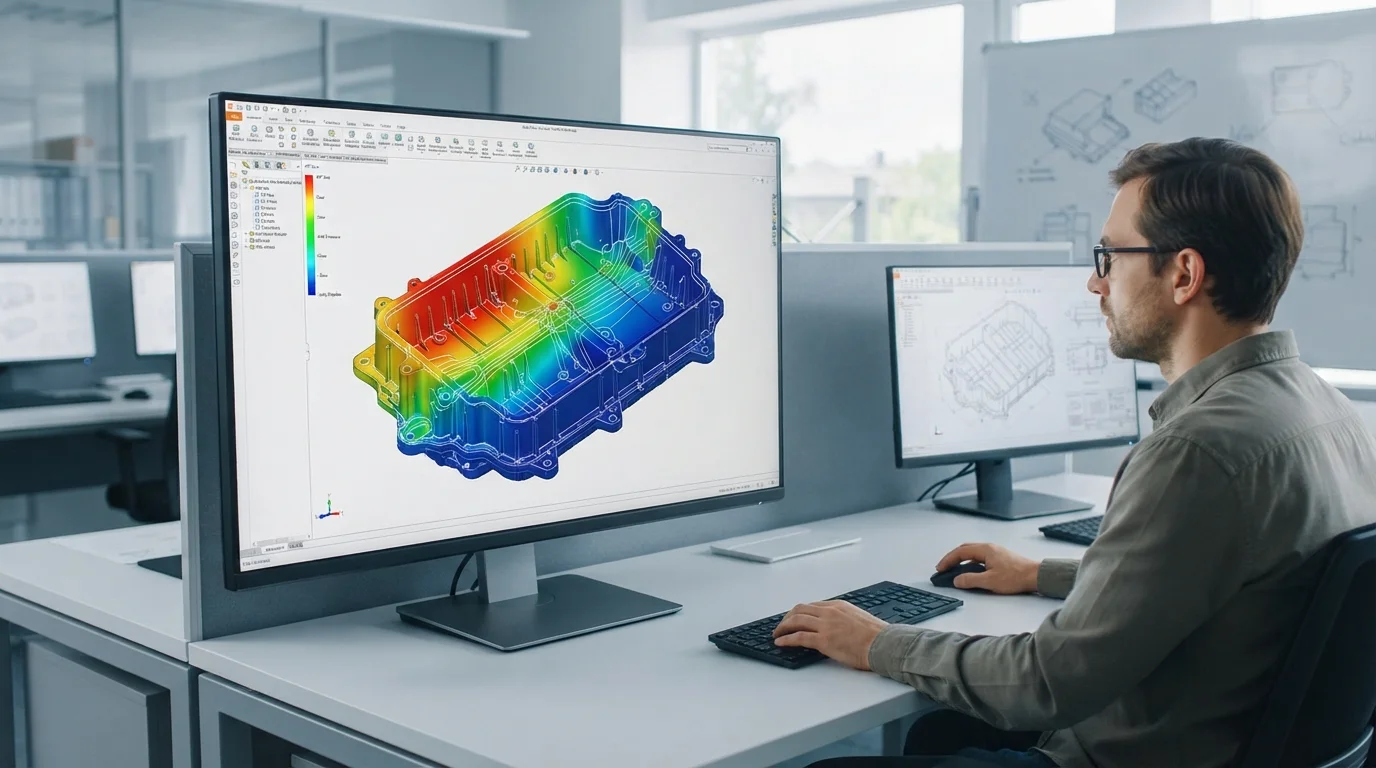
Optimizing structural geometries for カスタムEV用プラスチックバッテリーハウジング prevents defects and lowers production costs.
Draft angles of at least 1.5 to 2 degrees must be incorporated on all vertical ribs and side walls to permit clean ejection without part distortion.
Wall thickness must remain as uniform as possible, ideally ranging from 2.5mm to 3.5mm, to prevent differential shrinkage and sink marks.
Flow simulation analysis prevents problematic knit lines, especially around the molded insert zones where molten plastic splits and recombines around cold metal busbars.
Our end-to-end custom tooling and manufacturing workflow typically follows this path:
- Design evaluation (DfM)—Providing a detailed manufacturability review, assessing draft angles, gate locations, and predicting potential knit lines within 24 hours.
- Tooling fabrication—Milling high-precision mold cavities from hardened H13/S136 steel using our in-house 5-axis high-speed CNC machining centers.
- Trial molding (T0/T1)—Conducting trial runs to optimize injection pressure, melt temperature, and holding times, yielding initial physical samples for dimensional checks.
- Quality verification—Utilizing Zeiss coordinate measuring machines to scan critical part geometries and cell pocket concentricity, compiling precise dimensional reports.
- Final production—Executing low-to-high volume injection molding runs backed by IATF 16949-certified quality control and complete lot traceability.
For design validation, relying on low volume rapid tooling for EV battery prototypes accelerates validation times while limiting initial non-recurring engineering tooling expenses.
Our facility builds rapid mold structures utilizing P20 or Alumec 89 aluminum cores, permitting functional molded prototypes of カスタムEV用プラスチックバッテリーハウジング to be delivered in as fast as 10 to 12 business days.
This bridge-to-production strategy allows automotive engineering teams to perform real-world environmental stress screening, drop testing, and vibration analysis before investing in mass-production, multi-cavity hardened steel tools.
Our team manages the entire project from initial design optimization to post-mold assembly under one roof.
Our in-house 5-axis CNC machining, ultrasonic plastic welding, thermal heat staking, and coordinate measuring machine inspections complete our comprehensive turnkey operations.
Every production lot is fully traceable, and our quality control engineers verify critical-to-quality dimensions on every shipment.
We sign non-disclosure agreements early in the design cycle, safeguarding proprietary intellectual property and ensuring confidential product launches.
よくある質問(FAQ)
How do you manage warpage in large, glass-filled battery trays?
Shrinkage management involves balancing the fiber orientation in glass-filled polyamide materials.
Glass fibers tend to align with the melt flow, causing the material to shrink less along the flow direction than across it.
We use advanced mold-flow software to simulate gate placement, frequently utilizing valve-gated hot runner systems to control the flow front and balance orientation, minimizing structural warpage.
What is the typical mold lifespan for flame-retardant plastics?
Mold lifespans vary depending on the tooling steel and polymer additives.
Flame-retardant agents release corrosive gasses at high temperatures, which degrade soft steels.
By using premium hardened S136 or H13 stainless steels with specialized anti-corrosive coatings, our molds consistently achieve over 500,000 cycles, maintaining tight dimensional tolerances over high-volume production runs.
Can you mold copper or aluminum busbars directly into battery covers?
Insert molding requires precise clamping pressure and strict shut-off tolerances to prevent plastic flash.
Our robotic insert systems place busbars with sub-millimeter precision.
We design custom sealing lands on the mold steel that firmly grip the metallic inserts, ensuring a leak-proof seal and preventing any flash onto the connection terminals.