
تتطلب حزم بطاريات السيارات الكهربائية (EV) إدارة حرارية قوية وعزلًا كهربائيًا وهياكل مقاومة للصدمات.
يمثل الانتقال من العلب المعدنية الثقيلة إلى البلاستيكات الهندسية عالية القوة تطورًا كبيرًا في تصميم حزم السيارات.
يوضح هذا الدليل الفني هندسة القوالب واعتبارات التصميم للتصنيع (DfM) وتقنيات معالجة البوليمرات المتقدمة الضرورية لإنتاج علب موثوقة.
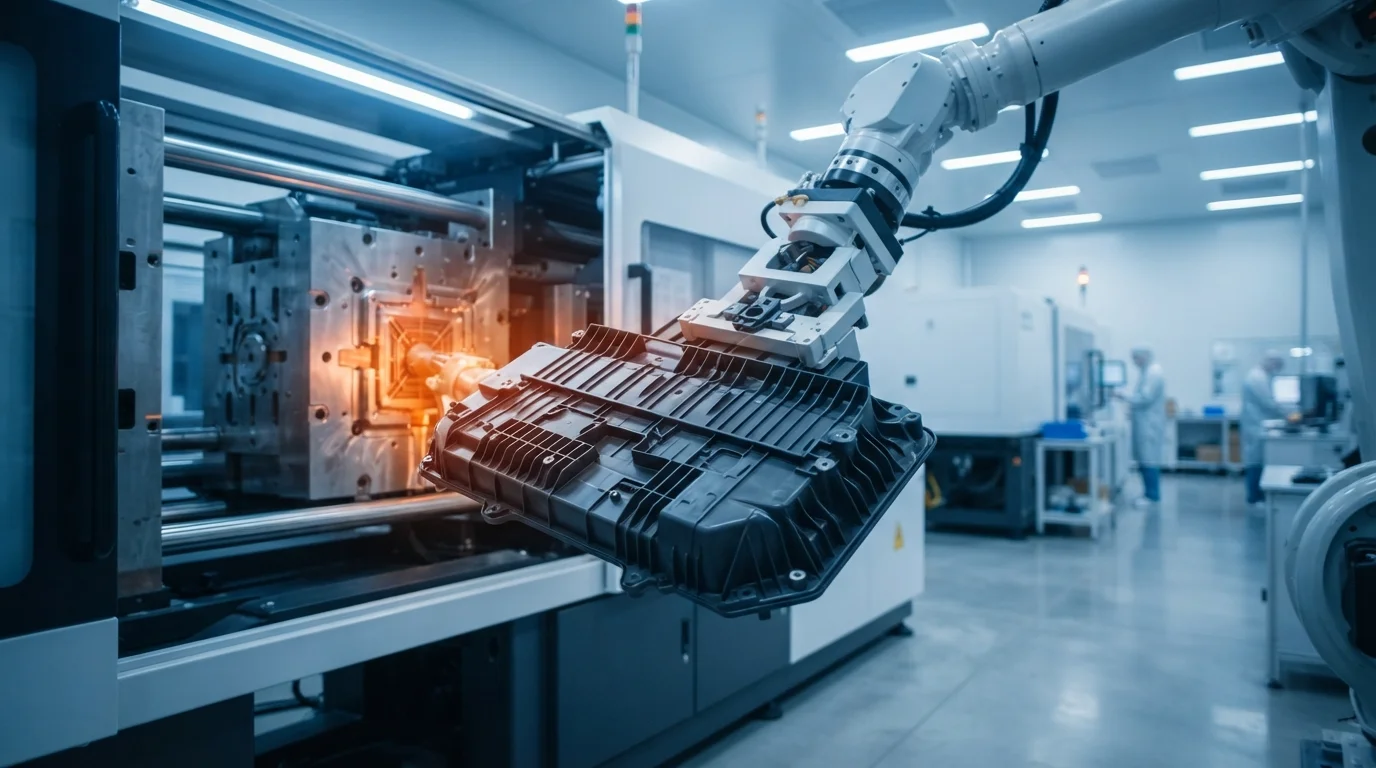
تعمل JUCHENG Injection Molding كمنشأة تصنيع تعاقدي راقية ومخصصة للمهام الخاصة، متخصصة في القوالب المخصصة والقولبة البلاستيكية الدقيقة.
نحن لا نبيع صناديق بطاريات قياسية أو جاهزة بالتجزئة؛ يتم تصميم كل مكون من نماذج CAD ثلاثية الأبعاد المقدمة من العميل لتلبية مواصفات أداء صارمة.
سواء كنت تتنقل في مراحل النماذج الأولية أو تنتقل إلى إنتاج متعدد التجاويف بكميات كبيرة، تقدم منشأتنا دعمًا تصنيعيًا مخصصًا مدعومًا بشهادات IATF 16949 وISO 13485.
جدول المحتويات
لماذا تعتبر القولبة بالحقن المخصصة ضرورية لعلب بطاريات السيارات الكهربائية
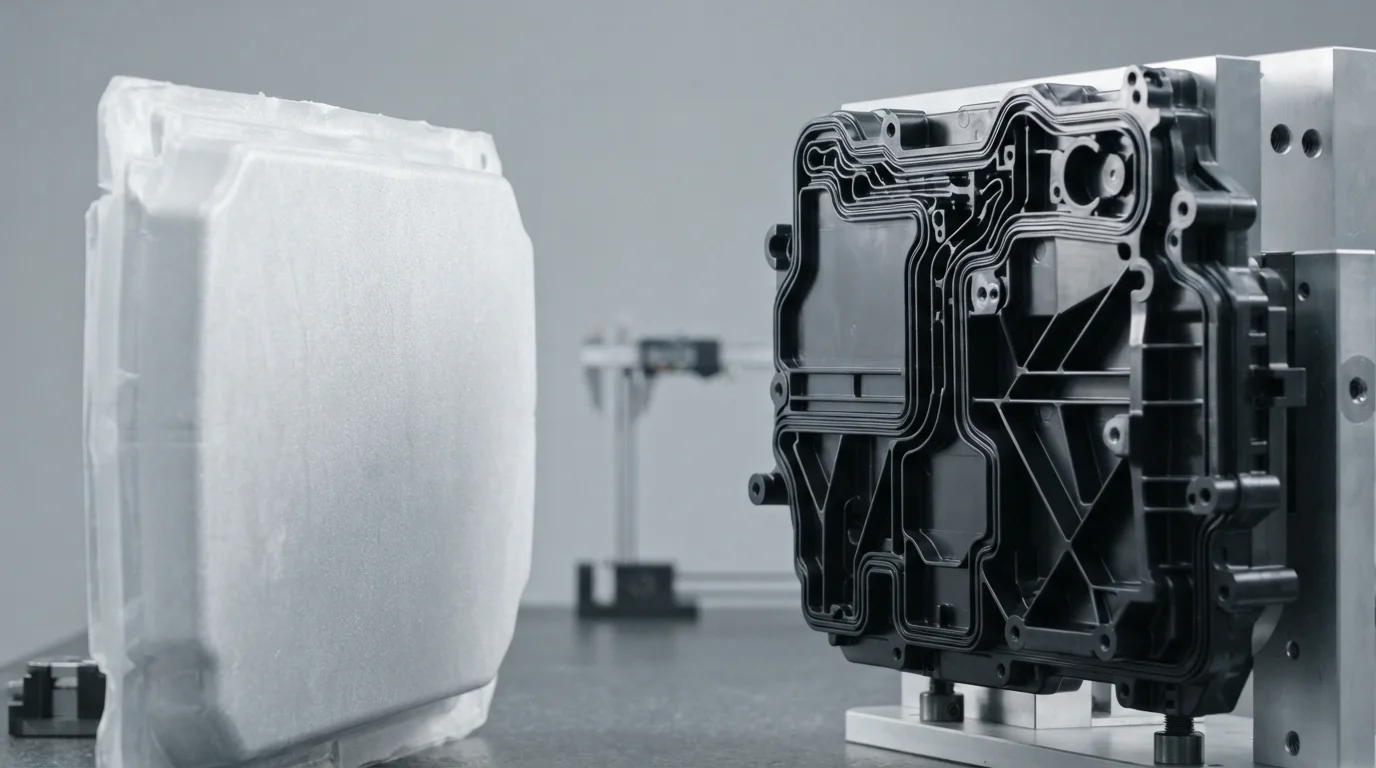
هندسة قوية أغلفة البطاريات البلاستيكية المخصصة للمركبات الكهربائية requires an understanding of structural integration and tight tolerance control.
Traditional metallic casings are heavy and require secondary insulation liners to prevent short circuits.
By utilizing high-performance polymers, engineers can mold complex geometries, internal features, and functional mounts directly into a single unified part.
Consolidating components in this manner reduces bill-of-materials costs, eliminates secondary assembly steps, and shaves critical weight off the vehicle chassis.
Integrating internal components is crucial for protecting individual lithium-ion cells from thermal runaway propagation.
Seamless integration of electric vehicle battery cell holders directly within the structural walls of the main housing prevents vibrational wear on cell terminals.
Furthermore, incorporating thin, high-insulation electric vehicle battery spacers prevents thermal runaway from leaping between pouch or prismatic cell modules.
Such configurations optimize space utilization inside the battery pack, allowing higher energy density while maintaining structural integrity during mechanical impacts.
Compared to alternative processing methods like sheet metal stamping or thermoforming, injection molding provides superior repeatability and dimensional accuracy.
High-pressure injection molding forces molten plastic into precision-machined cavities, producing parts with zero draft variations and highly consolidated molecular structures.
This is especially crucial for molding elastomeric sealing channels and perimeter tongue-and-groove joints that prevent moisture and dust from breaching the battery module.
إن الشراكة مع متخصص تصنيع ذي خبرة تضمن أن الأجزاء المخصصة الخاصة بك تتوافق مع معايير السلامة الصارمة في قطاع السيارات.
معايير المواد ومقاومة اللهب (UL94 V-0)
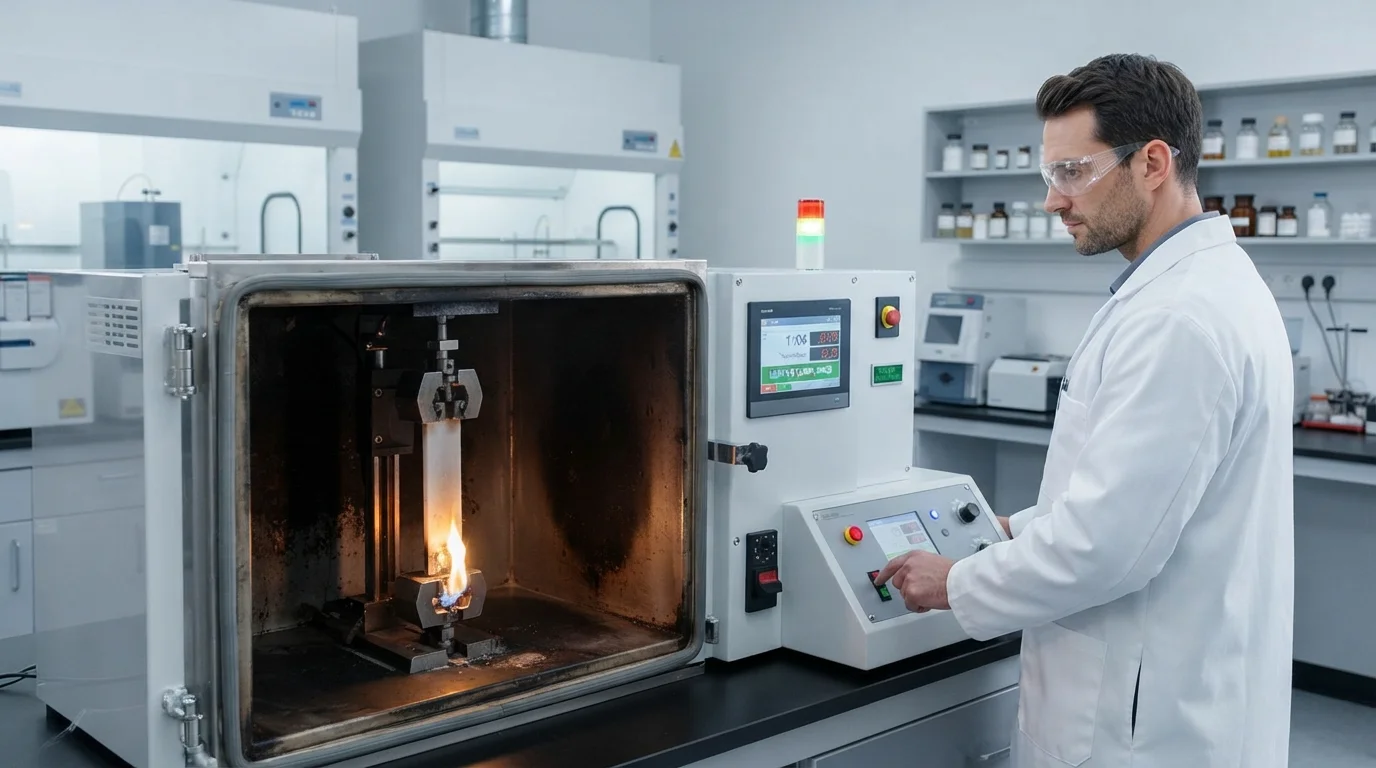
تطوير متخصص أغلفة البطاريات البلاستيكية المخصصة للمركبات الكهربائية يعتمد على اللدائن الحرارية عالية الأداء.
يجب على المهندسين الموازنة بين قوة الصدم ومقاومة المواد الكيميائية لإلكتروليتات البطارية ودرجة حرارة انحراف الحرارة ومقاومة الزحف على المدى الطويل.
وبالتالي، فإن استخدام حقن قوالب Bayblend FR3010 لوحدات بطاريات المركبات الكهربائية يضمن أداءً فائقًا في مقاومة الصدم حتى -30°C مع تحقيق تصنيف قابلية الاشتعال UL94 V-0 عند سماكة 1.5 مم.
توفر هذه الخلطة غير المتبلورة من البولي كربونات وأكريلونيتريل بوتادين ستايرين خصائص معدل انكماش يمكن التنبؤ بها، مما يسهل إنتاج أغطية مسطحة خالية من الالتواء.
تشمل متطلبات أداء المواد الأساسية لأغلفة بطاريات الجهد العالي:
- الاستقرار الحراري—يجب أن تحافظ اللدائن الهندسية على السلامة الهيكلية تحت درجات حرارة تشغيل مستمرة تتجاوز 100°C.
- مثبطات اللهب—يؤدي تحقيق تصنيف UL94 V-0 الصارم إلى منع انتشار الحريق وإطفاء الأجزاء البلاستيكية ذاتيًا في غضون ثوانٍ.
- قوة العزل الكهربائي—تمنع المقاومة الحجمية العالية حدوث القوس الكهربائي بين خلايا البطارية والهيكل الخارجي.
- مقاومة الصدم—Robust physical properties safeguard the delicate lithium cell matrix from debris puncture during dynamic driving.
Similarly, manufacturing flame retardant PC ABS battery enclosures ensures structural rigidity while providing reliable electrical insulation.
When high mechanical rigidity is required to withstand extreme drop tests, glass-fiber reinforced polymers represent the optimal choice.
For instance, choosing إطارات بطارية مصبوبة بالحقن من ليكسان 940A offers exceptional flame retardancy coupled with the dimensional stability required for interlocking prismatic cell matrices.
This polycarbonate resin maintains its physical properties under constant thermal loads, preventing cell migration during rapid charging and discharging cycles.
Safety compliance remains non-negotiable for all high-voltage automotive components.
Therefore, specifying قولبة بالحقن لحامل خلايا بلاستيكي مثبط للهب UL94 V-0 guarantees that the polymer will self-extinguish within 10 seconds of a flame application, preventing catastrophic thermal fire propagation.
Structural trays also demand extreme load-bearing capabilities.
Indeed, handling تصنيع أدراج بطاريات المركبات الكهربائية من البولي أميد المقوى بألياف الزجاج presents challenges with warpage due to the differential shrinkage between the transverse and parallel glass fiber orientations.
Our mold design team overcomes this by optimizing gate locations and using balanced hot runner systems to distribute fiber alignment evenly across the mold cavity.
| درجة المادة | نوع البوليمر | Tensile Strength (MPa) | HDT عند 1.82 ميجا باسكال (°م) | تصنيف القابلية للاشتعال |
|---|---|---|---|---|
| Bayblend FR3010 | PC + ABS Blend | 60 | 110 | UL94 V-0 |
| Lexan 940A | بولي كربونات (PC) | 65 | 125 | UL94 V-0 |
| PA66-GF30 (FR) | Polyamide 66 + 30% GF | 150 | 240 | UL94 V-0 |
| TPV (70A-40D) | مطاط حراري مبلمر | 8 – 15 | N/A (Elastomeric) | UL94 HB / V-0 |
Advanced Tooling Capabilities for Complex Battery Geometry
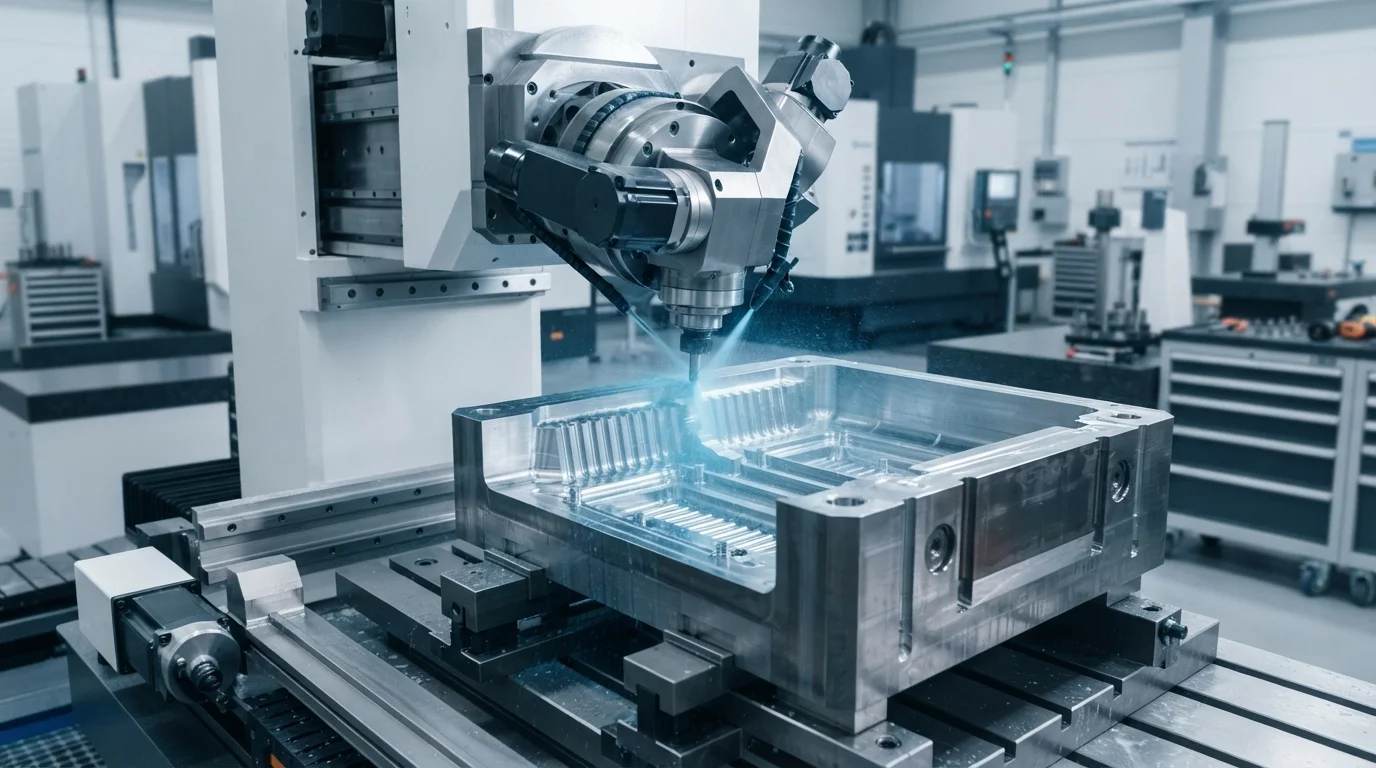
Mold design directly influences the long-term quality, flatness, and structural reliability of custom components.
Our dual-certified facility leverages 25+ in-house 5-axis CNC machines to cut precise mold cores out of hardened H13 or S136 tool steel.
Hardened steels are mandatory for handling highly corrosive, flame-retardant additives and abrasive glass fibers without suffering pitting or rapid dimensional erosion.
During the molding process, optimized conformal cooling channels integrated into the mold steel reduce cycle times by up to 30%, ensuring even heat dissipation and preventing post-mold warpage.
One prominent technique involves overmolding high-voltage conductive elements directly inside the structural shell.
Specifically, employing insert molding busbars in EV battery covers minimizes assembly errors and prevents environmental moisture from leaking into critical high-voltage contact areas.
This requires incredibly tight tooling shut-off tolerances to prevent plastic flash from flowing onto the active contact surfaces of copper or aluminum busbars.
Our precise tooling designs utilize spring-loaded core pins and real-time cavity pressure sensors to prevent crushing the metal inserts during mold clamp-up.
Moisture and dust ingress must be prevented to avoid short-circuiting expensive lithium cell modules.
Thus, performing حشوات بطاريات TPV المطاطية الحراريّة المخصصة يضمن أن أغلفة البطاريات البلاستيكية المخصصة للمركبات الكهربائية achieve dynamic sealing profiles directly integrated onto the rigid PC/ABS cover.
Achieving this dual-material integration is possible through advanced multi-shot injection molding or custom overmolding processes, completely eliminating the labor-intensive hand-application of adhesive foam strips.
Such multi-material integrations remain a hallmark of automotive-grade manufacturing, providing robust protection against IP67 and IP69K moisture standards.
DfM Analysis & Complete Turnkey Services
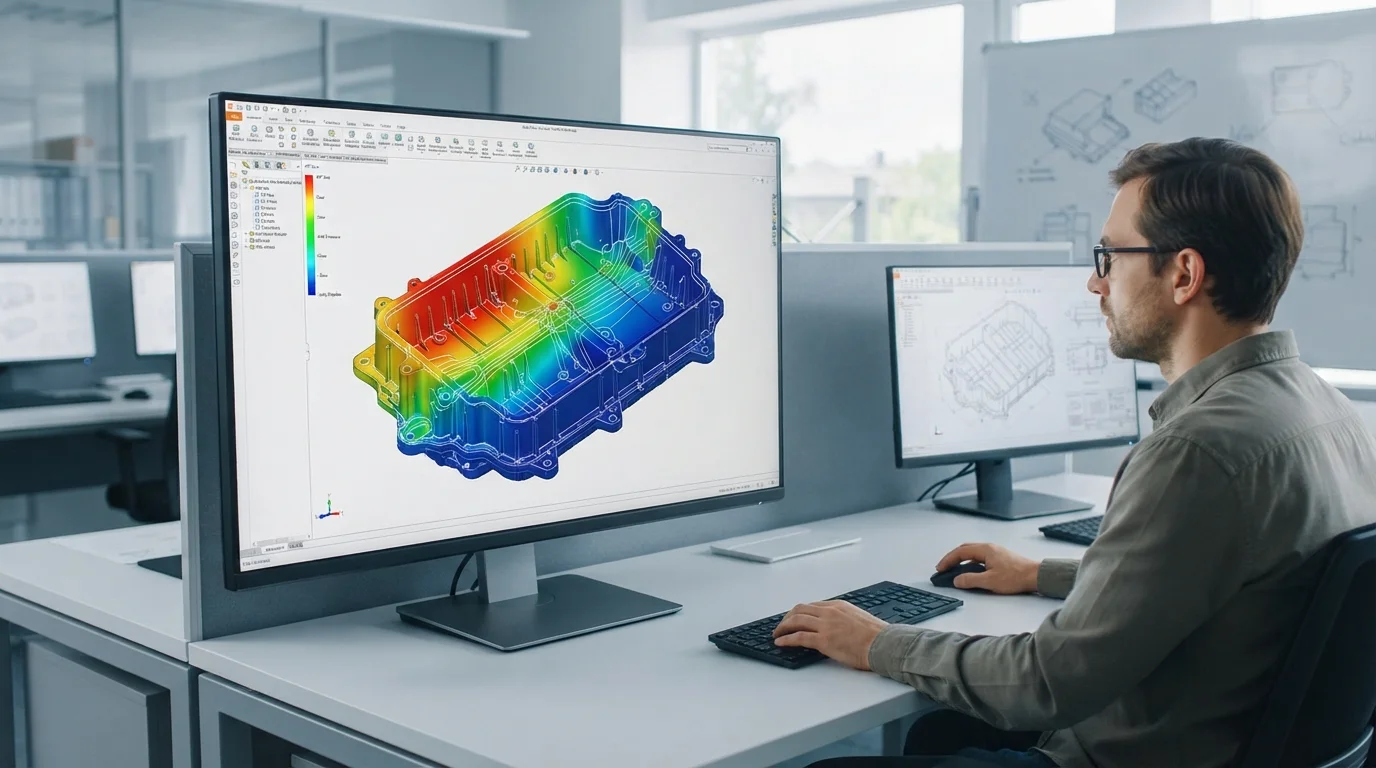
Optimizing structural geometries for أغلفة البطاريات البلاستيكية المخصصة للمركبات الكهربائية prevents defects and lowers production costs.
Draft angles of at least 1.5 to 2 degrees must be incorporated on all vertical ribs and side walls to permit clean ejection without part distortion.
Wall thickness must remain as uniform as possible, ideally ranging from 2.5mm to 3.5mm, to prevent differential shrinkage and sink marks.
Flow simulation analysis prevents problematic knit lines, especially around the molded insert zones where molten plastic splits and recombines around cold metal busbars.
Our end-to-end custom tooling and manufacturing workflow typically follows this path:
- Design evaluation (DfM)—Providing a detailed manufacturability review, assessing draft angles, gate locations, and predicting potential knit lines within 24 hours.
- Tooling fabrication—Milling high-precision mold cavities from hardened H13/S136 steel using our in-house 5-axis high-speed CNC machining centers.
- Trial molding (T0/T1)—Conducting trial runs to optimize injection pressure, melt temperature, and holding times, yielding initial physical samples for dimensional checks.
- Quality verification—Utilizing Zeiss coordinate measuring machines to scan critical part geometries and cell pocket concentricity, compiling precise dimensional reports.
- Final production—Executing low-to-high volume injection molding runs backed by IATF 16949-certified quality control and complete lot traceability.
For design validation, relying on low volume rapid tooling for EV battery prototypes accelerates validation times while limiting initial non-recurring engineering tooling expenses.
Our facility builds rapid mold structures utilizing P20 or Alumec 89 aluminum cores, permitting functional molded prototypes of أغلفة البطاريات البلاستيكية المخصصة للمركبات الكهربائية to be delivered in as fast as 10 to 12 business days.
This bridge-to-production strategy allows automotive engineering teams to perform real-world environmental stress screening, drop testing, and vibration analysis before investing in mass-production, multi-cavity hardened steel tools.
Our team manages the entire project from initial design optimization to post-mold assembly under one roof.
Our in-house 5-axis CNC machining, ultrasonic plastic welding, thermal heat staking, and coordinate measuring machine inspections complete our comprehensive turnkey operations.
Every production lot is fully traceable, and our quality control engineers verify critical-to-quality dimensions on every shipment.
We sign non-disclosure agreements early in the design cycle, safeguarding proprietary intellectual property and ensuring confidential product launches.
الأسئلة الشائعة (FAQ)
How do you manage warpage in large, glass-filled battery trays?
Shrinkage management involves balancing the fiber orientation in glass-filled polyamide materials.
Glass fibers tend to align with the melt flow, causing the material to shrink less along the flow direction than across it.
We use advanced mold-flow software to simulate gate placement, frequently utilizing valve-gated hot runner systems to control the flow front and balance orientation, minimizing structural warpage.
What is the typical mold lifespan for flame-retardant plastics?
Mold lifespans vary depending on the tooling steel and polymer additives.
Flame-retardant agents release corrosive gasses at high temperatures, which degrade soft steels.
By using premium hardened S136 or H13 stainless steels with specialized anti-corrosive coatings, our molds consistently achieve over 500,000 cycles, maintaining tight dimensional tolerances over high-volume production runs.
Can you mold copper or aluminum busbars directly into battery covers?
Insert molding requires precise clamping pressure and strict shut-off tolerances to prevent plastic flash.
Our robotic insert systems place busbars with sub-millimeter precision.
We design custom sealing lands on the mold steel that firmly grip the metallic inserts, ensuring a leak-proof seal and preventing any flash onto the connection terminals.