
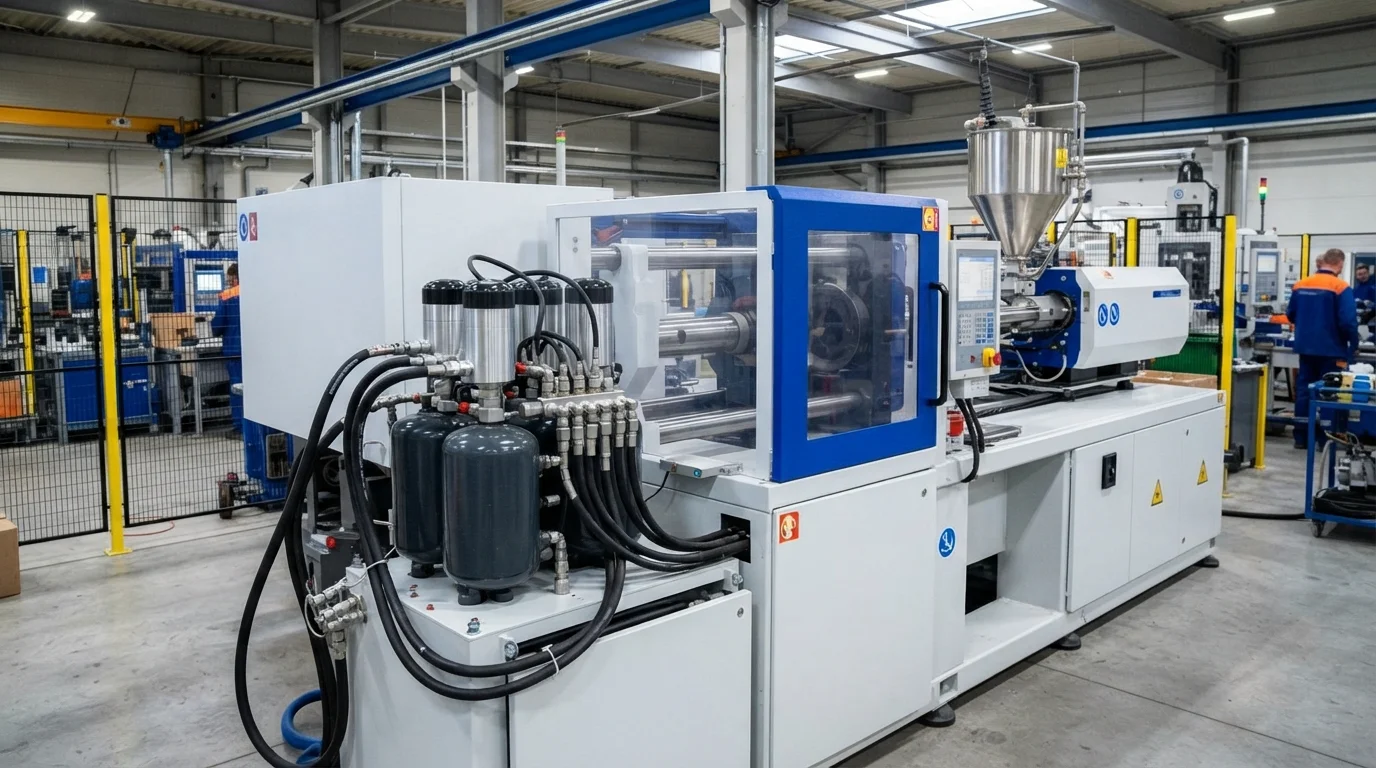
대량 생산되는 박육 플라스틱 부품을 제조하려면 용융물이 응고되기 전에 금형 캐비티를 충전하기 위해 높은 사출 속도가 필요합니다. 기존 사출 기계는 0.8mm 미만의 벽 두께를 가진 긴 유동 경로를 충전하는 데 필요한 즉각적인 유압 응답이 부족합니다. 고속 사출 성형 을 지정하면 유압 질소 어큐뮬레이터를 사용하여 사출 스크류를 구동함으로써 이러한 유동 제한을 해결합니다. JUCHENG은 특수 고속 생산 셀을 운영하여 박육 포장재, 의료 진단 컵, EV 배터리 스페이서를 생산합니다.
목차
어큐뮬레이터 보조 사출 프레스 및 고속 사출 속도
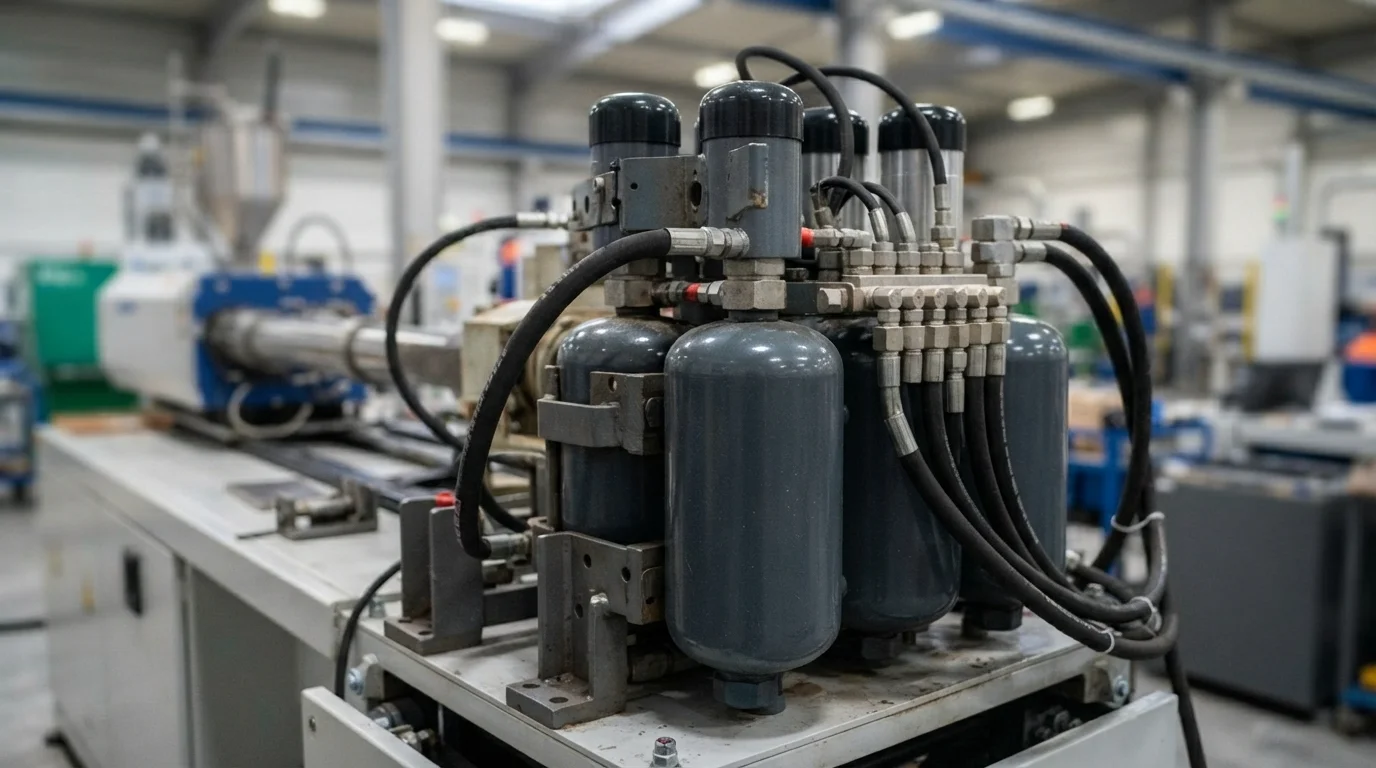
박육 형상에서 캐비티를 완전히 충전하려면 최대 1,000mm/초의 사출 속도가 필요합니다. 사출 기계에 어큐뮬레이터 보조 사출 프레스 를 장착하면 충전 단계에서 즉각적인 유압 유체 용량이 공급됩니다. 질소 어큐뮬레이터는 수 밀리초 내에 저장된 압력을 방출하여 사출 스크류를 즉시 최고 속도로 가속합니다. 초고속 충전은 차가운 캐비티 표면을 따라 폴리머 용융물 전단부가 조기에 응고되는 것을 방지합니다. 폐쇄 루프 압력 변환기는 매 사이클마다 용융물 유변학을 모니터링하여 충전 속도에서 보압으로의 즉각적인 전환을 보장합니다.
고속 프레스 작동 표준은 다음과 같습니다:
- 질소 어큐뮬레이터 방전—저장된 유압 오일 용량을 방출하여 극도의 초기 가속으로 사출 스크류를 구동합니다.
- 폐쇄 루프 응답 제어—Monitoring cavity pressure transducers prevents overpacking and flashing along mold parting lines.
- 높은 형체력 안정성—Holding mold core plates shut under intense peak injection pressures prevents parting line flash.
- Fast-acting hydraulic valves—Executing sub-millisecond valve shifts optimizes velocity-to-pressure transfer during filling.
Thin-Wall Packaging & EV Battery Insulation Components (≤0.8 mm)
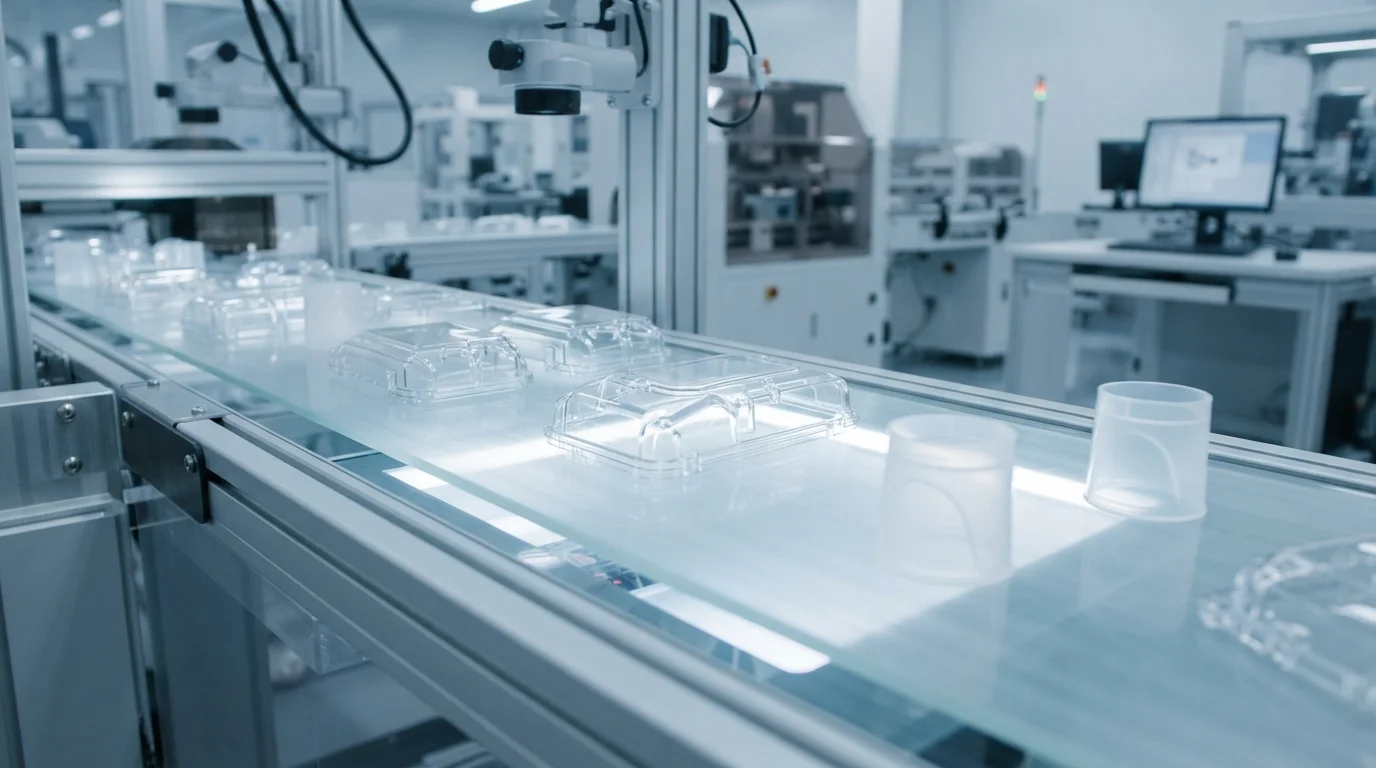
Thin-walled components featured in EV battery spacers and consumer packaging demand high Melt Flow Index (MFI) resins. Processing thermoplastics like high-flow 폴리카보네이트(PC), LCP, PA66, 및 폴리프로필렌(PP) requires precise temperature control. High injection speeds generate frictional shear heat within narrow runner gates, reducing resin viscosity dynamically. Lower melt viscosity permits plastic to travel across high flow-length-to-thickness (L/T) ratios exceeding 200:1. Vacuum-assisted cavity evacuation systems draw air out of the mold before injection, preventing micro-bubbles and diesel burns.
| 폴리머 수지 등급 | MFI 범위(g/10min) | Wall Thickness (mm) | Filling Speed (mm/sec) | Primary High-Speed Application |
|---|---|---|---|---|
| PP (Borealis RF365MO) | 35 – 70 | 0.40 – 0.80 mm | 600 – 900 mm/sec | 박막 포장 및 용기 |
| 고유동 PC (Makrolon 2407) | 25 – 55 | 0.60 – 1.00 mm | 500 – 800 mm/sec | 전자 제품 커버 및 디스플레이 프레임 |
| PA66-GF30 (Zytel 70G33L) | 20 – 40 | 0.80 – 1.20 mm | 400 – 700 mm/sec | EV 배터리 모듈 절연 플레이트 |
고캐비테이션 금형 냉각 및 핫 러너 균형 유동
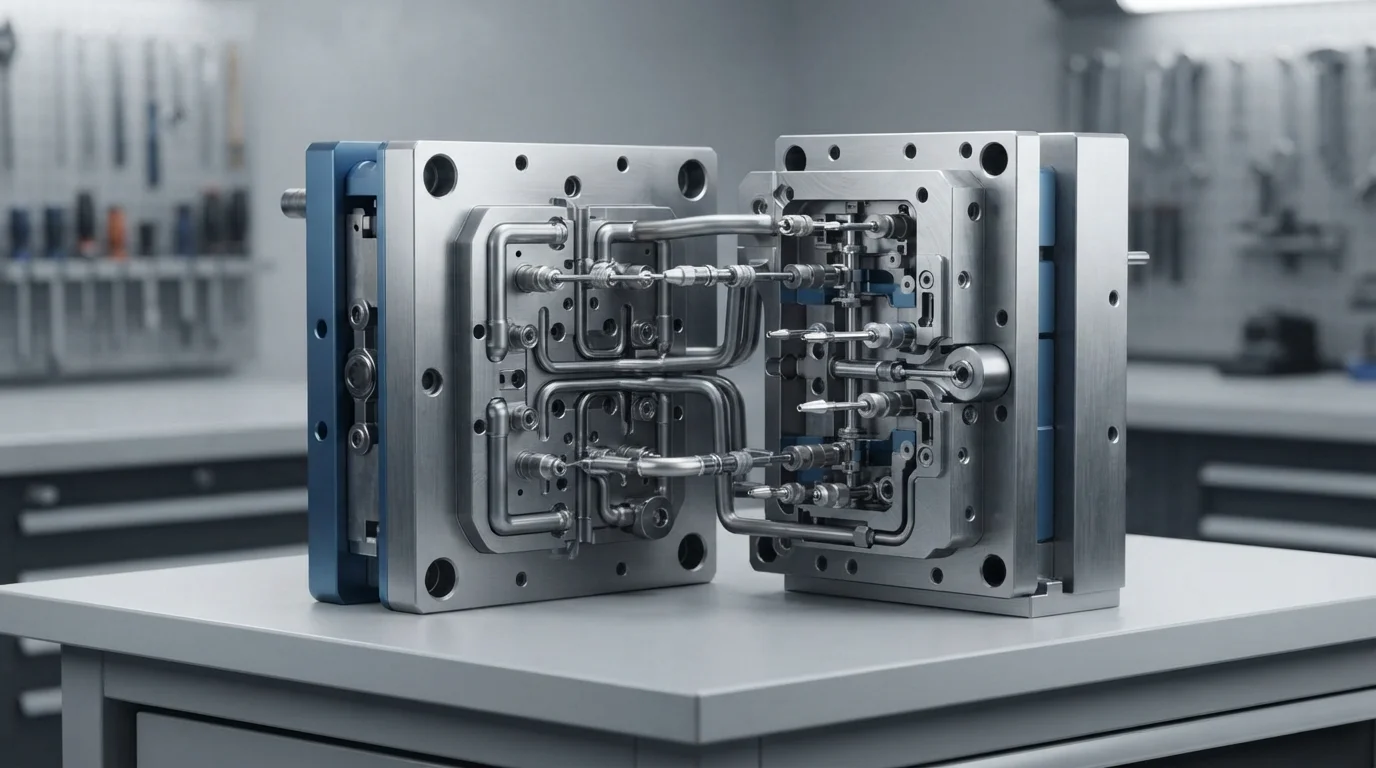
생산량 극대화는 멀티 캐비티 금형과 최적화된 열 관리에 달려 있습니다. 통합 핫 러너 균형 유동 manifolds ensures equal melt distribution to every cavity, maintaining uniform part weight. High-cavitation molds require balanced cooling networks to extract heat rapidly from thin polymer walls. Configuring conformal cooling channels close to cavity faces reduces cooling times to under 3 seconds per shot. Executing scientific molding methodology through 디커플링 성형 isolates filling speed from packing pressure, maintaining CpK > 1.67 across long production runs.
자주 묻는 질문 (FAQ)
Why is an accumulator needed for high speed injection molding?
Hydraulic accumulators store pressurized nitrogen gas to deliver instant hydraulic oil volume during injection. This instant pressure boost accelerates the screw three times faster than standard hydraulic pumps, filling thin wall cavities before the melt freezes.
What is a typical cycle time for high speed thin-wall molding?
Cycle times for thin-wall packaging and electronic covers typically range from 2 to 6 seconds. High-speed injection, fast cooling water circuits, and automated robotic part extraction minimize cycle duration.
How do you prevent diesel burn marks during ultra-fast injection?
Preventing diesel burns requires integrating precision micro-venting slots measuring 0.015 mm to 0.02 mm along parting lines and using vacuum cavity evacuation. Drawing air out of the tool before injection prevents compressed gas from igniting.