
PA-BASF Ultramid A3WC8
열적 또는 화학적 안정성을 저하시키지 않으면서 하중 지지 구조 메커니즘에서 무거운 다이캐스트 아연 및 항공우주 등급 알루미늄 합금을 대체하기 위해, BASF의 Ultramid A3WC8은 40 wt.% 단탄소섬유 강화, 열안정화 폴리아미드 66(PA66-CF40) 매트릭스를 활용합니다. 밀도 1.28 g/cm³와 융점 262°C를 자랑하는 이 고성능 복합재는 23,500 MPa의 뛰어난 인장 탄성률과 고유한 정전기 방출(ESD) 특성을 제공합니다. IATF 16949 및 ISO 9001 인증 체계에서 운영되는 Jucheng Precision은 Ultramid A3WC8 성형을 전문으로 합니다. 5축 CNC 가공 S136 스테인리스 스틸 툴링의 지원을 받아 이방성 수축 변수(0.1%-0.4%)를 제어하여 Zeiss CMM으로 검증된 평평하고 구조적으로 결함 없는 부품을 제공합니다.
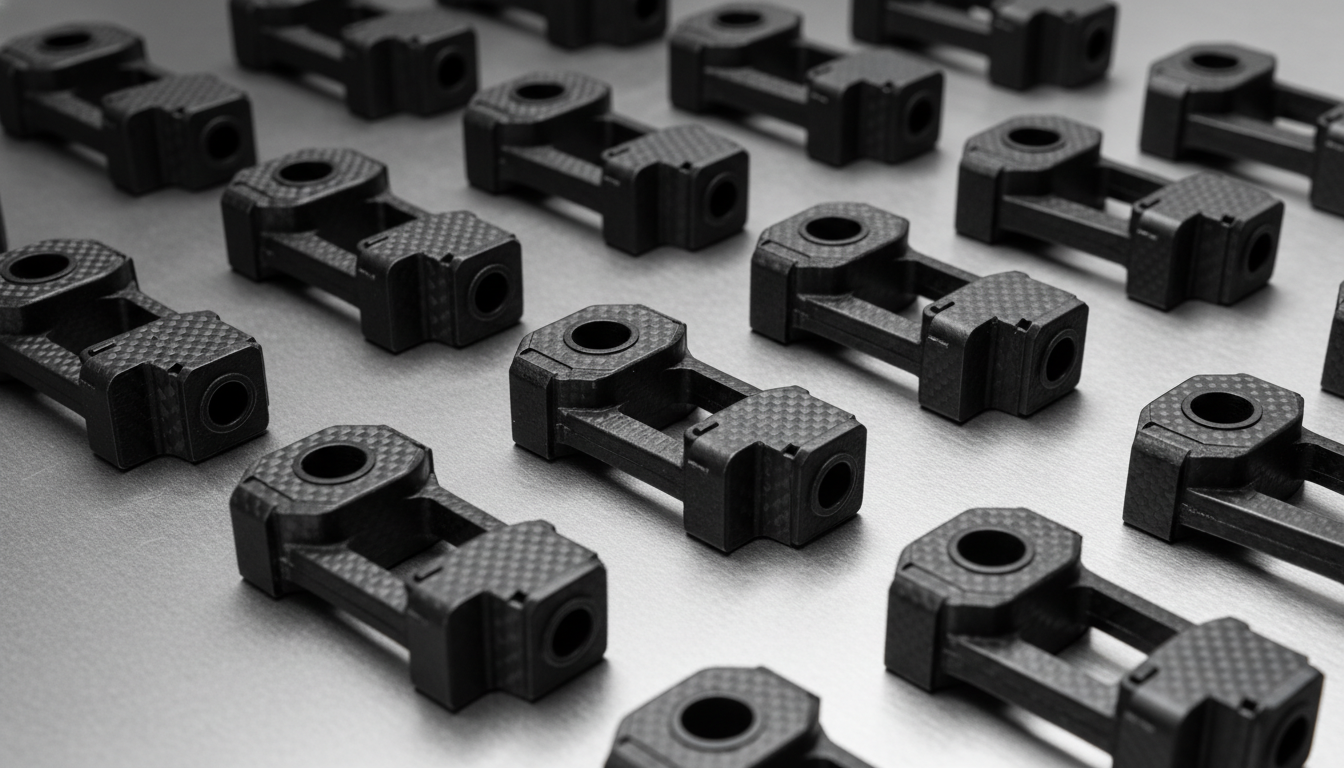
Ultramid A3WC8 40% Carbon-Fiber Structural Mechanics
Ultramid® A3WC8 is a 40 wt. % short carbon fiber reinforced, heat stabilized, high flow PA66 injection molding grade engineered by BASF, certified to deliver unmatched mechanical stiffness and electrostatic dissipation (ESD) under ISO/ASTM standards:
| 엔지니어링 파라미터 | 일반 값 (DAM / ISO) | 금속 대체 이점 |
|---|---|---|
| 구조적 강성 | Tensile Modulus 23.5 GPa (23,500 MPa) | 구조용 금속에 비해 엄청난 중량 절감을 가능하게 하는, 예외적으로 낮은 밀도(1.28 g/cm³)에서 금속과 맞먹는 놀라운 계수를 제공합니다. |
| 파단 시 인장 강도 | 230 MPa (ISO 527-1,2) | 엄청난 구조적 하중 지지 능력을 제공하여 동적 아연, 황동 및 알루미늄 브래킷을 성공적으로 대체합니다. |
| 전기 전도성 | 표면 저항 10^2 – 10^6 Ohm/sq | 본질적으로 전도성이 있어 민감한 전자 보빈에 우수한 정전기 방전(ESD) 및 EMI 차폐 보호를 제공합니다. |
Process & Dynamic Configurations for High-Flow Ultramid A3WC8
With its high mechanical stiffness and carbon fiber reinforcement, Ultramid A3WC8 supports precise, unyielding structural molds:
| 성형 기술 등급 | 공정 호환성 및 운영 세부 사항 |
|---|---|
| Weight-Critical Aerospace Mounts | Excellent. The primary process for Ultramid A3WC8. Engineered for high-stiffness aircraft brackets, structural engine mounts, and avionic cable clamps. |
| High-Viscosity Structural Robotics | 우수함. 낮은 밀도와 극한의 비강성( specific modulus )이 결합되어 경량 로봇 암의 빠르고 높은 수율의 제조를 지원합니다. |
| Dynamic ESD Connectors | 양호함. 고유의 탄소 섬유 전도성 매트릭스는 고정밀 부품에 안정적인 정전기 방전(ESD) 및 EMI 차폐를 제공합니다. |
PA-BASF Ultramid A3WC8 Tooling & Carbon Fiber Processing Guide
Molding an ultra-high performance carbon-fiber reinforced polyamide like Ultramid A3WC8 requires strict moisture control and optimized gating to prevent abrasive tool wear and warpage:
분말 야금 경화 공구강
40% short carbon fibers act as an aggressive grinding agent under high injection pressures and melt viscosity. Jucheng’s tooling division prevents gate and cavity erosion by using premium CPM powder metallurgy tool steels or hardened H13/S136 steel (HRC 54–56) with PVD ceramic coatings.
이방성 수축 및 휨 관리
Ultramid A3WC8 shrinks exceptionally low along the flow (typically 0.10%) but higher perpendicular to the flow (0.40%). We conduct detailed Moldflow analysis during DFM to locate gates, ensuring uniform fiber orientation to prevent structural warping.
가압 오일 금형 온도 제어
당사는 가압 온수 히터를 사용하여 금형 온도를 80°C–120°C(176°F ~ 248°F)로 유지합니다. 높은 금형 온도는 표면 광택을 극대화하고 웰드 라인을 줄이며 표면 탄소 섬유가 떠오르는 것을 방지하여 매끄럽고 섬유가 없는 마감을 보장합니다.
건조제 건조 프로토콜(가수분해 방지)
PA66 is highly sensitive to moisture at high melt temperatures. Wet molding results in rapid hydrolytic chain cleavage, causing severe splay, gas bubbles, and a major drop in impact strength. We desiccant dry Ultramid A3WC8 resin at 80°C–100°C (176°F–212°F) for 4–6 hours, keeping moisture below 0.10% (ideally <0.08%).
Key Application Fields for PA-BASF Ultramid A3WC8
- 항공우주 구조 피팅 및 방위 산업: 초경량 드론 구조 암, 항공기 브래킷 마운트, 무기 케이싱 브래킷, 다이내믹 슬라이드 가이드, 광학 센서 베젤.
- 정밀 동적 산업 기계: 중부하 유성 기어, 헬리컬 기어 세트, 자동 윤활 슬라이딩 부싱, 고압 펌프 임펠러, 압축기 씰.
- 의료 기기 및 수술 시스템(ISO 13485): 방사선 투과성 수술 타겟팅 프레임, 비자성 실험실 카세트, 환자 맞춤형 정형외과 기구, 수술 로봇 관절.
속성
| 밀도 | 1.28 g/cm³ |
| 용융 온도 | 262 °C |
| 인장 탄성률(DAM) | 23,500 MPa |
| 인장 응력 (파단 시, DAM) | 230 MPa |
| 인장 신율 (파단 시, DAM) | 1.5 % |
| 굴곡 강도 (DAM) | 325 MPa |
| 굴곡 탄성률 (DAM) | 21,500 MPa |
| 샤르피 노치 충격 강도 (23°C) | 8.5 kJ/m² |
| 수분 흡수율 (평형, 50% RH) | 1.5 % |
| 열변형 온도 (HDT @ 1.80 MPa, DAM) | 255 °C |
| 표면 저항 | 1.0E+02 - 1.0E+06 Ohm/sq |
| 선형 몰드 수축률 (흐름 방향) | 0.1 % |
| 선형 몰드 수축률 (가로 방향) | 0.4 % |
| 최대 부품 크기 | 1000 x 800 mm |
| 최소 부품 크기 | 1 x 1 mm |