
A family mold and a multi-cavity mold solve different production problems. A family tool makes different components together; a multi-cavity tool repeats the same component across several cavities. Choose by the output mix your product actually needs, then confirm that the mold can meet each part’s process and quality requirements. The lowest cavity count or the most parts per cycle is not, by itself, the best economic answer.
The difference in one decision
A family mold contains cavities for two or more different parts, often components used in one assembly. A multi-cavity mold contains multiple cavities for the same part, producing a larger quantity of a common component per cycle. The distinction changes how output is balanced, inspected, scheduled, and maintained.
If the order needs matching components in a fixed ratio and the parts can share a stable molding window, a family mold may simplify coordination. If demand is concentrated on one part and the priority is repeatable output at volume, a multi-cavity layout may be the clearer starting point. Either concept still needs engineering review of fill, pack, cooling, ejection, and measurement.
Compare output, balance, and control

| Decision factor | Family mold | Multi-cavity mold |
|---|---|---|
| What each cycle produces | Different components, typically in a fixed set ratio | Repeated copies of one component |
| Primary balance challenge | Different cavity geometries and process needs | Consistency among nominally identical cavities |
| Demand fit | Works best when parts are consumed in a coordinated mix | Fits demand concentrated on the same part |
| Quality review | Each component needs its own acceptance and inspection plan | Part-to-part variation among cavities needs monitoring |
| Change impact | One component revision may affect the shared tool or validation route | A common part change can affect all repeated cavities |
The comparison is conceptual, not a guarantee of cost or cycle-time advantage. A family mold may require more balancing attention because parts differ. A multi-cavity tool can require careful cavity-to-cavity consistency and a robust sampling plan. The actual result depends on part design, resin, tool layout, machine, quality requirements, and order pattern.
When different parts should share a tool
Consider a family tool when components are regularly used together and the demand ratio makes its fixed output useful. The parts should be reviewed for compatible materials, wall sections, likely gates, cooling needs, and release behavior. A bracket and a cover can belong to one assembly yet still need different fill or cooling conditions; part relationship alone does not prove mold compatibility.
Think through the result after molding as well. Can each part be separated, identified, inspected, and packaged without losing traceability? What happens if one component fails inspection while the rest of the set is acceptable? If production continues to make every cavity together, the quality and inventory plan must handle that consequence.
Review family injection mold solutions for the broader tooling concept. Keep separate tooling on the table if part revisions, materials, or production demand are not aligned.
When repeated cavities make more sense
A multi-cavity mold is a natural candidate when the program needs many copies of the same part and the design can be replicated consistently. The design review then focuses on matching cavity geometry and flow paths, balancing the runner, controlling cooling variation, and confirming that each cavity makes acceptable parts over the intended run.
Higher cavity count also changes inspection planning. Rather than treating the shot as one undifferentiated group, maintain a way to associate observed variation with cavity position when troubleshooting. Sampling frequency and traceability should be selected from the part’s risk and quality plan; no single sampling rule fits every product.
Explore multi-cavity injection mold design when the program’s output is repeated copies of one component. More cavities are useful only if the process can fill, cool, eject, and verify the complete tool consistently.
A buyer’s selection checklist
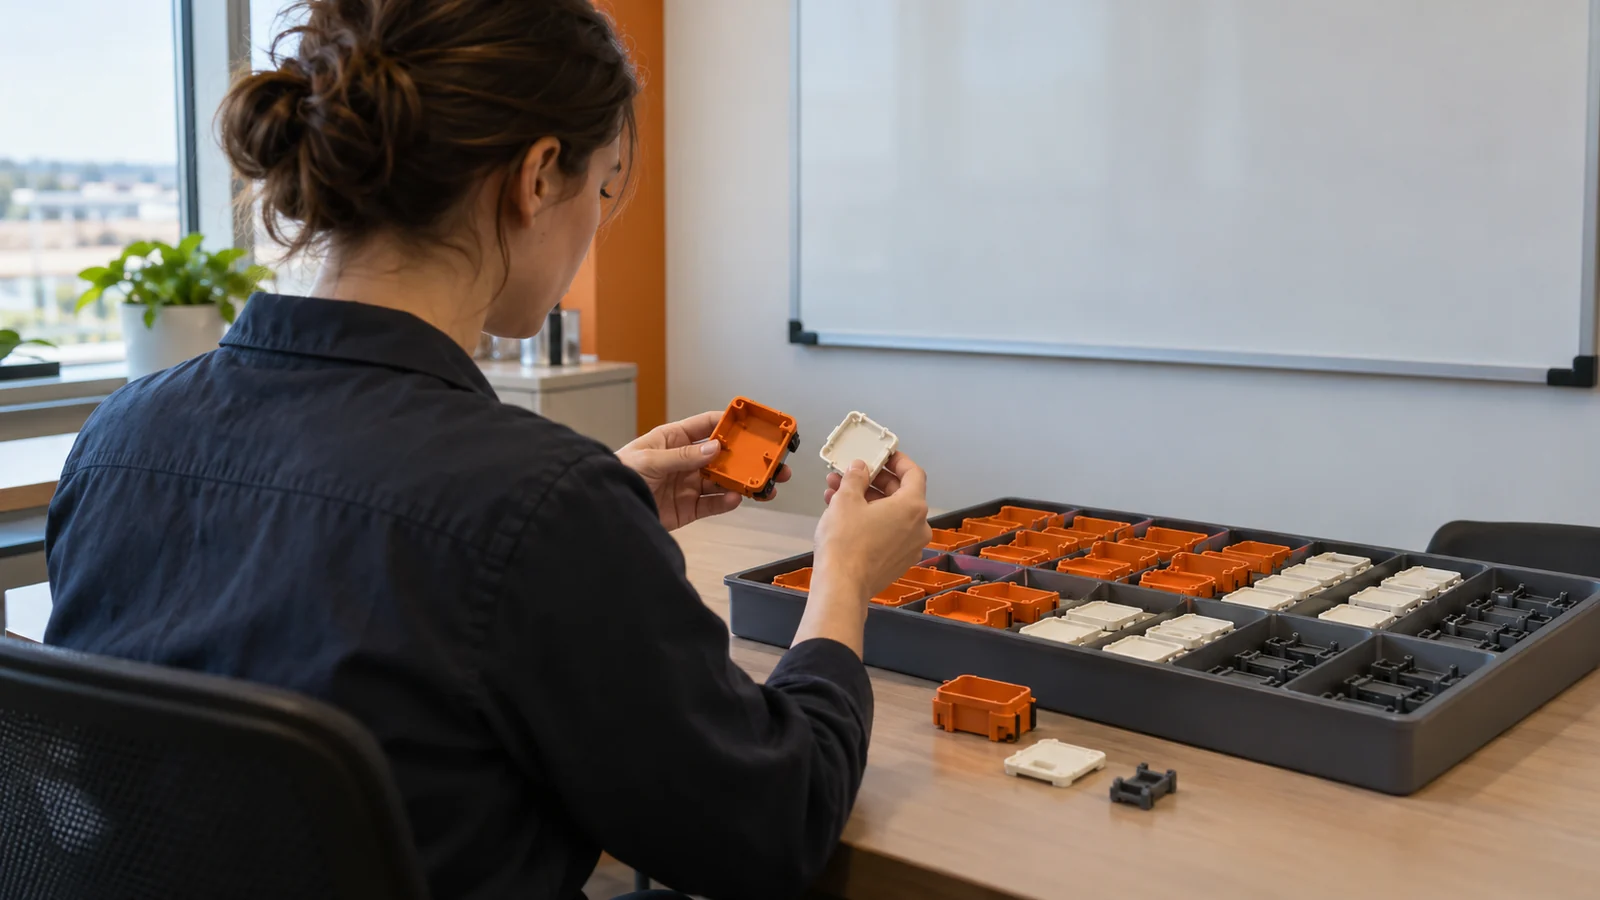
- List every part needed per finished assembly and forecast demand by component.
- Identify resin grade, color, appearance zones, critical dimensions, and inspection method for each part.
- Compare the family output ratio with real consumption and packaging requirements.
- Ask how fill balance, cooling, ejection, and cavity-level quality will be validated.
- Compare lifecycle cost, maintenance isolation, future revisions, and inventory exposure—not just quoted tool price.
When the answers point in different directions, request a design review using the actual CAD and demand mix. The right mold concept should match the product’s production logic, not just maximize the number of cavities on a drawing.
FAQ
Does a family mold have multiple cavities?
Yes. The term describes different parts in the cavities, not the absence of multiple cavities. A multi-cavity mold usually refers to repeated cavities for the same part.
Which mold type has better part-to-part consistency?
Neither name guarantees consistency. A multi-cavity tool must control variation among repeated cavities; a family tool must control each different component against its own specifications.
Can I choose based only on annual volume?
No. Volume matters, but so do the ratio of components, material compatibility, inspection needs, tool maintenance, and the process window required by each part.