
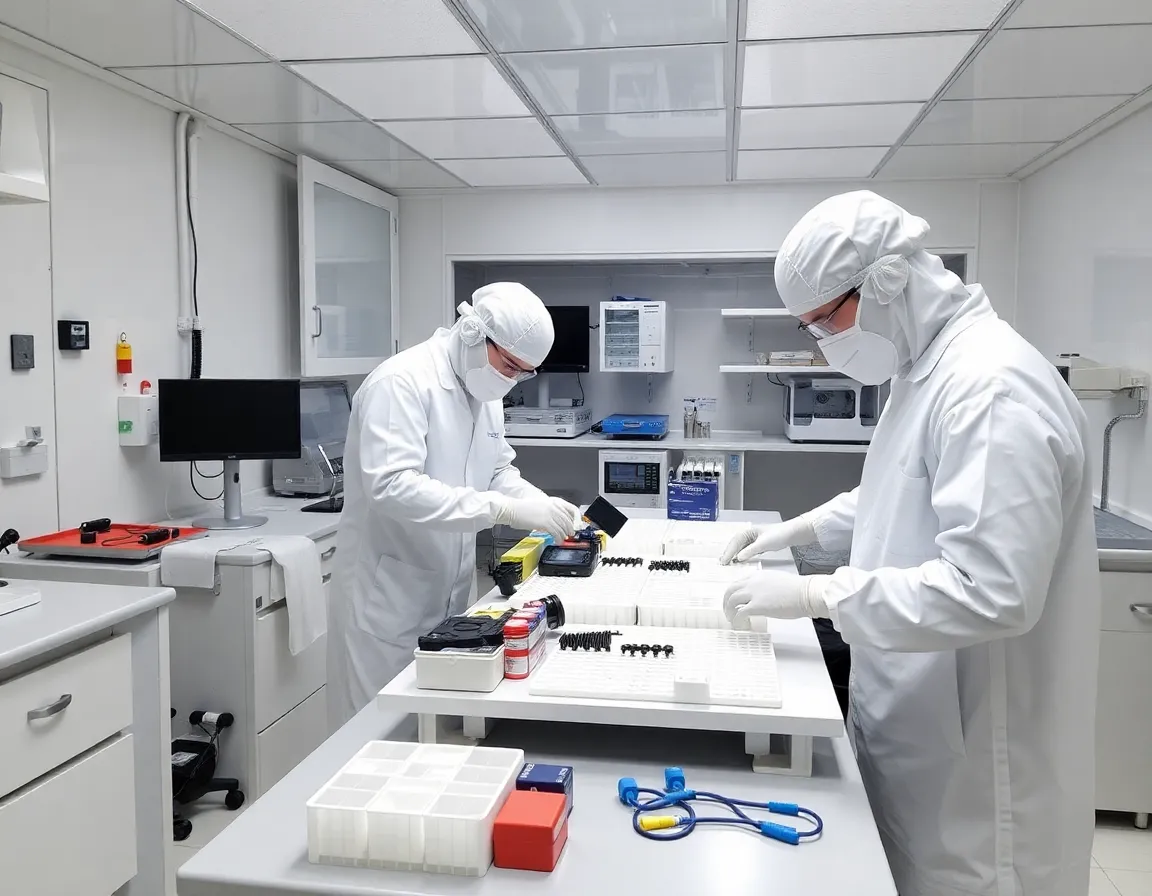
Understanding High Purity Plastic Molding: A Precision Discipline
High purity plastic molding is a specialized manufacturing process that goes far beyond conventional injection molding. It is the art and science of producing plastic components with exceptionally low levels of contamination, particulates, ionic residues, and organic volatiles. In industries such as semiconductor fabrication, medical device manufacturing, pharmaceutical processing, and biotechnology, even a single microscopic particle can render an entire batch of product unusable or compromise a life-critical procedure. This process demands not only advanced machinery but a holistic approach to cleanroom protocols, material science, and process validation. The difference between a standard molded part and a high purity part is measured in parts per billion, and achieving that level of precision requires mastering seven critical secrets that separate world-class facilities from average ones.
Unlike standard molding where the primary focus is on dimensional tolerance and cycle time, high purity molding prioritizes chemical inertness, surface integrity, and the absence of extractables. The polymers used—such as PEEK, PTFE, PFA, and ultrapure polypropylene—must be specially formulated without plasticizers, stabilizers, or fillers that could leach out. The molding environment itself must be a controlled cleanroom, typically rated ISO Class 7 or better, with constant monitoring of airborne particles. This is not merely a manufacturing technique; it is a comprehensive quality philosophy that touches every aspect of production, from resin handling to final packaging.
The Seven Critical Accuracy Secrets
Mastering high purity plastic molding requires a deep understanding of seven distinct yet interconnected factors. Each secret addresses a specific point of failure that could introduce contamination or compromise accuracy. When all seven are executed flawlessly, the result is a component that meets the most stringent purity standards in the world.
Secret 1: Resin Drying and Handling Protocols
The first secret lies in the preparation of the raw material. Many engineering polymers are hygroscopic, meaning they absorb moisture from the air. In standard molding, this moisture causes cosmetic defects like splay or silver streaks. In high purity molding, absorbed moisture can cause hydrolytic degradation of the polymer chain, releasing volatile organic compounds (VOCs) that contaminate the part. The secret is to use dedicated, sealed drying hoppers with desiccant dryers that maintain a dew point of -40°C or lower. Critically, the resin must be handled in an inert nitrogen atmosphere to prevent oxidation. The transfer from the drying hopper to the molding machine must be done via sealed, vacuum-conveyed lines that are purged with nitrogen, ensuring that the resin never contacts ambient air. This prevents both moisture uptake and the introduction of airborne particulates.
Secret 2: Screw and Barrel Design for Shear Control
The plasticizing unit of the injection molding machine is a major source of contamination if not properly engineered. Standard screws are designed for high throughput, but they create high shear forces that can degrade the polymer, producing low-molecular-weight fragments and carbonized particles. The secret here is a low-compression-ratio screw with a gentle, gradual transition zone. This design minimizes shear heating and mechanical stress on the polymer chains. Additionally, the screw and barrel must be made from corrosion-resistant, wear-resistant alloys such as bimetallic composites or ceramic-coated steel. This prevents metal ions from abrading off the screw surface and entering the melt. The barrel should also have a specially designed venting section to allow any residual gases or moisture vapor to escape without creating pressure spikes that cause degradation.
Secret 3: Precision Temperature Control in the Mold
Temperature uniformity is the third critical secret. In high purity molding, the mold temperature must be controlled within ±1°C across the entire cavity surface. This is achieved using des canaux de refroidissement conformes that follow the exact contour of the part geometry, rather than simple straight-drilled lines. The cooling medium is typically deionized water or a specialized heat-transfer fluid that leaves no residue. The mold itself must be made of stainless steel (e.g., 17-4 PH or S136) that is electro-polished to a mirror finish. This mirror finish is essential because any microscopic scratch or pit in the mold surface becomes a trap for polymer residue, which then degrades and releases contaminants in subsequent cycles. Furthermore, the mold must be equipped with a heated sprue bushing and a hot runner system that has no dead zones where material can stagnate and degrade.
Secret 4: Controlled Decompression and Venting
Trapped air and gases are the enemies of purity. If air is compressed inside the cavity, it undergoes adiabatic heating, which can scorch the polymer and create carbonized particles. The secret is a two-fold approach. First, the mold must have micro-venting—extremely shallow vent channels (0.01 to 0.02 mm deep) located at the end of the fill path. These vents allow air to escape but are too small for molten polymer to flash into. Second, the injection process must use a controlled decompression (suck-back) step. After the screw stops, it retracts slightly to reduce the pressure in the nozzle, preventing drool and stringing. This decompression also creates a slight vacuum that helps pull any residual volatile gases back into the barrel for removal, rather than letting them get trapped in the part.
Secret 5: Post-Molding Cleanroom Handling
The molding process does not end when the part is ejected. In fact, the moment of ejection is the highest-risk time for contamination. The part is still hot and static-charged, making it a magnet for airborne particles. The secret is to have the molding machine integrated directly into a cleanroom, with the mold opening inside the clean zone. Robotic arms made of non-shedding materials (e.g., ceramic or coated aluminum) must remove the part without touching the critical surfaces. The parts then fall into sealed, antistatic containers that are immediately purged with nitrogen. No human hands ever contact the molded part. Additionally, the entire post-molding area must have laminar airflow (HEPA-filtered) that flows from the mold outward, preventing any external contamination from entering the open cavity.
Secret 6: Real-Time Process Monitoring and Data Logging
Consistency is impossible without measurement. The sixth secret is the implementation of capteurs dans le moule (pressure and temperature transducers) that monitor every cycle in real time. These sensors feed data into a closed-loop control system that automatically adjusts injection speed, packing pressure, and cooling time to maintain perfect repeatability. But the deeper secret is the data logging itself. Every cycle produces a digital fingerprint—a trace of pressure, temperature, and screw position. This data is stored in a secure database for each serialized part. If a downstream quality check reveals a contamination issue, engineers can trace the exact cycle parameters that produced that part and identify the anomaly. This level of traceability is not just good practice; it is a regulatory requirement in medical and pharmaceutical applications.
Secret 7: Validation and Statistical Process Control (SPC)
The final secret transcends the machine and enters the realm of methodology. High purity molding cannot be achieved by setting parameters once and hoping for the best. It requires a rigorous validation protocol that includes IQ (Installation Qualification), OQ (Operational Qualification), and PQ (Performance Qualification). During PQ, the process must demonstrate a Cpk (Process Capability Index) of at least 1.67, meaning that the process variation is less than 20% of the tolerance range. But the true secret is ongoing SPC. Every batch of parts is tested for particulate levels using liquid particle counters, and for ionic residues using ion chromatography. The results are plotted on control charts. If a trend toward contamination appears before a failure occurs, the process is stopped and corrected. This proactive, data-driven approach ensures that the process never drifts into a non-conforming state.
Key Benefits of High Purity Molding
The benefits of mastering these seven secrets are profound and measurable. First and foremost is product reliability. In semiconductor manufacturing, a single particle from a plastic component can cause a short circuit in a microchip, costing millions in lost production. High purity parts eliminate this risk. In medical devices, such as implantable pumps or dialysis filters, the absence of extractables prevents adverse immune reactions in patients. Second, high purity molding significantly reduces downstream cleaning costs. Many conventional parts require rigorous washing and sterilization before use. High purity parts are ready for use immediately, saving time and resources. Third, the precision temperature control and low-shear processing result in superior mechanical properties—parts have higher tensile strength and better chemical resistance because the polymer chains are not degraded. Fourth, the comprehensive data logging provides full regulatory compliance, making it easier to obtain FDA or CE approvals.
Critical Applications Requiring High Purity
The applications of high purity plastic molding are as demanding as they are diverse. In the semiconductor industry, components such as wafer carriers, chemical delivery fittings, and CMP (chemical mechanical planarization) rings are molded from ultrapure PEEK or PFA to withstand aggressive chemicals without leaching metal ions. In biopharmaceutical manufacturing, single-use bioreactor bags require ports and connectors molded from medical-grade polymers that can withstand gamma sterilization without degrading. In analytical instrumentation, components like chromatography column fittings and mass spectrometry interfaces must have zero background contamination to ensure accurate detection of trace analytes. Another growing application is in hydrogen fuel cell technology, where seals and manifolds must be pure enough to not poison the catalyst. Finally, in aerospace, high purity plastic valves and bearings are used in oxygen systems where any hydrocarbon contamination could cause catastrophic combustion.
Best Practices for Implementing High Purity Molding
For companies looking to transition from standard to high purity molding, several best practices can smooth the path. First, invest in cleanroom infrastructure first, not last. Many facilities try to retrofit cleanrooms around existing machines, which creates airflow dead zones. A purpose-built cleanroom with a raised floor for under-floor return airflow is ideal. Second, partner with a resin supplier that specializes in ultrapure grades and can provide certificates of analysis for each batch. Never assume that standard grade resin is pure enough. Third, train personnel rigorously. Even in an automated line, human intervention for maintenance and troubleshooting is inevitable. Every technician must understand that their skin cells, hair, and breath are contamination sources. Fourth, establish a preventive maintenance schedule that includes weekly particle testing of the molding machine's water lines and air lines. Finally, start with a pilot run of 100 parts and test them extensively before committing to full production. This pilot run will reveal hidden contamination sources that were not apparent during setup.
Conclusion: The Future of High Purity Molding
As technology pushes toward smaller geometries in electronics and more potent biologics in medicine, the demand for high purity plastic molding will only intensify. The seven secrets outlined here are not optional extras; they are mandatory disciplines that define the field. From the microscopic control of resin handling to the macroscopic oversight of statistical process control, each secret contributes to a system that is greater than the sum of its parts. The facilities that embrace these secrets will produce components that enable the next generation of innovation. Those that ignore them will find themselves locked out of the most advanced and lucrative markets. High purity molding is not just a manufacturing process—it is a commitment to perfection, measured in the absence of what we cannot see but what we know would harm us.