
Sản xuất các bộ phận phần cứng công thái học đòi hỏi phải kết hợp các chất đàn hồi mềm chạm vào trên các khung cấu trúc cứng. Lắp ráp cơ khí truyền thống sử dụng ốc vít hoặc keo thủ công làm tăng chi phí nhân công và tạo ra các điểm hỏng tiềm ẩn dưới tải trọng mỏi theo chu kỳ. Chỉ định ép phủ khuôn tùy chỉnh tích hợp các chất đàn hồi mềm trực tiếp lên nền nhựa cứng hoặc chèn kim loại trong quá trình xử lý. JUCHENG hoạt động như một nhà sản xuất hợp đồng tích hợp theo chiều dọc cung cấp các cụm ép phủ chính xác được xây dựng trực tiếp từ các tệp CAD do khách hàng cung cấp.
Mục lục
Lựa chọn nền và chất đàn hồi ép phủ (TPE, TPU, TPV)
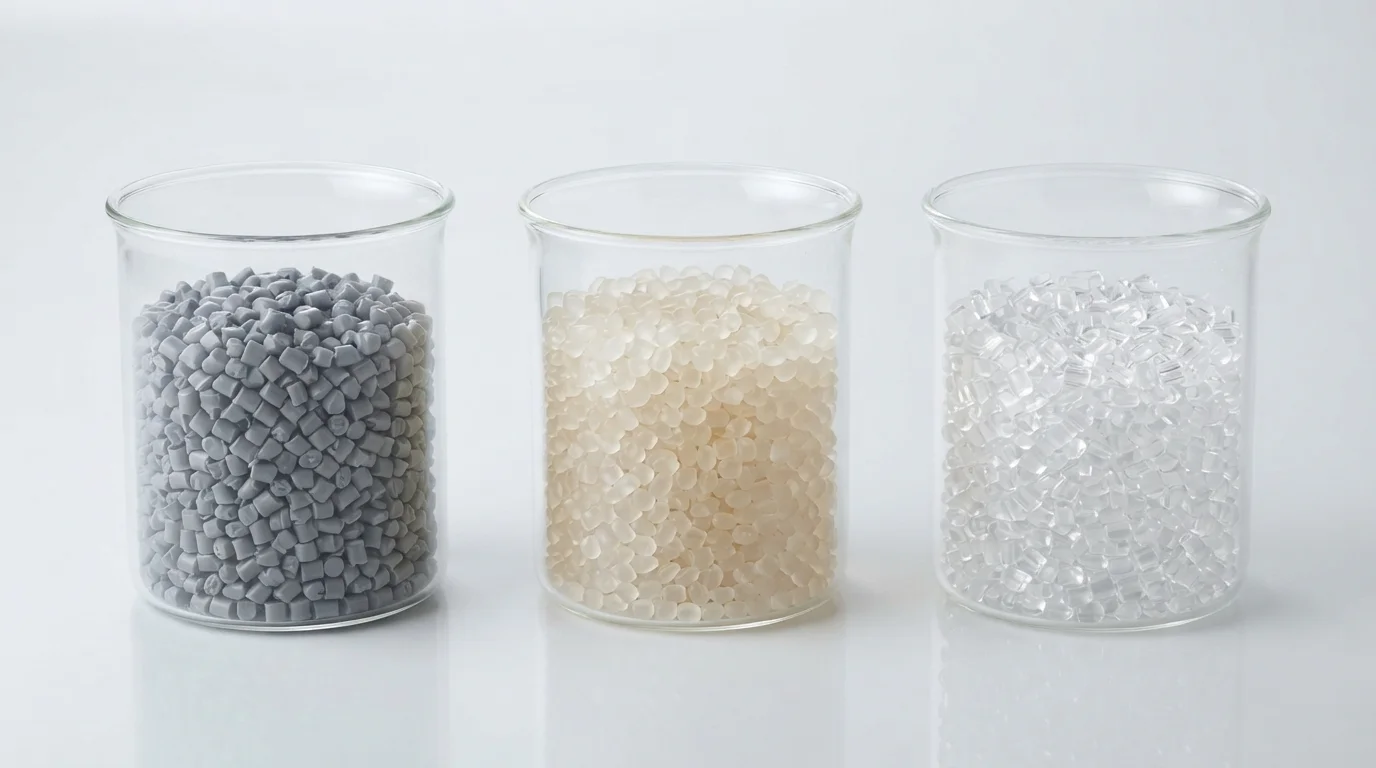
Việc lựa chọn các kết hợp nền và chất đàn hồi tương thích quyết định độ bền liên kết hóa học và hiệu suất cơ học của cụm lắp ráp. Nền cứng thường bao gồm các loại nhựa kỹ thuật như ABS, polycarbonate (PC), PA6/PA66, hoặc hợp kim PC/ABS . Việc khớp nhiệt độ biến dạng nhiệt của nền với nhựa ép phủ ngăn ngừa nóng chảy hoặc biến dạng nhiệt trong lần phun thứ hai. Các lớp đàn hồi ép phủ sử dụng các cấp độ hiệu suất cao bao gồm Santoprene TPV, Kraiburg TPE, và Desmopan TPU để đạt được các cấu hình độ cứng Shore tùy chỉnh.
| Cấp độ đàn hồi | Độ cứng Shore | Chất nền tương thích | Loại liên kết | Ứng dụng chính |
|---|---|---|---|---|
| Kraiburg TPE | 30A – 90A | ABS, PC, PC/ABS | Liên kết hóa học | Tay cầm mềm tiện dụng |
| Desmopan TPU | 60A – 70D | PC, PA6/PA66 | Khuếch tán cường độ cao | Tay cầm công nghiệp chống mài mòn |
| Santoprene TPV | 50A – 50D | PP, PA66-GF | Hóa học + Cơ học | IP67 weather-resistant seals |
Mold Design Techniques to Prevent Flash and Peel-Off
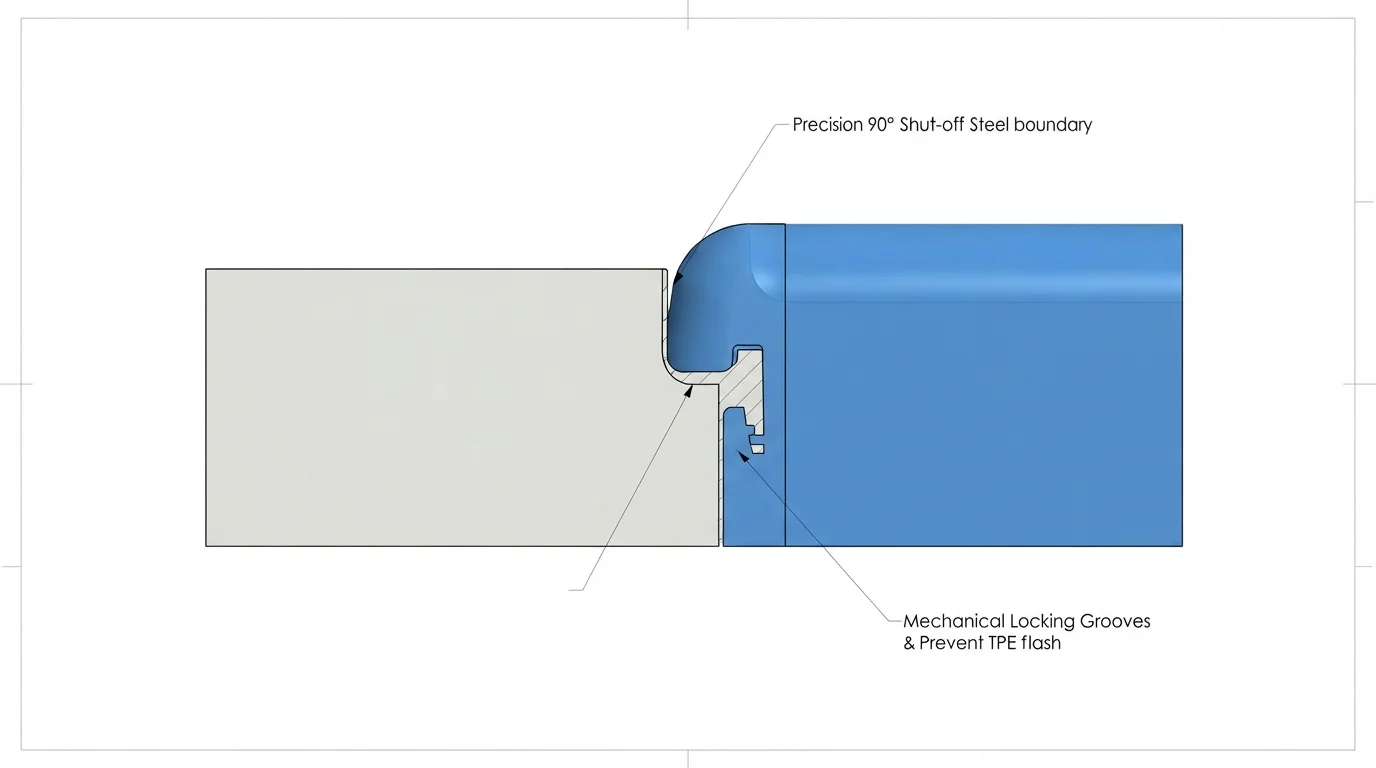
Tooling geometry directly controls the flash-free encapsulation and edge peel resistance of overmolded elastomers. Low-viscosity soft resins flow easily under injection pressure, creating cosmetic flash if mold shut-offs are improperly fitted. Machining durable tool cavities utilizing 25 sets of 5-axis CNC machining centers ensures shut-off steel tolerances under ±0.01 mm, preventing soft rubber leakage. Incorporating mechanical locking features along the border of the elastomeric boundary provides secondary physical retention.
Critical mold design steps for reliable overmolding execution include:
- Shut-off land tolerance—Designing shut-off steel with tolerances under 0.01 mm prevents elastomeric flash on cosmetic surfaces.
- Perimeter mechanical grooves—Incorporating 90-degree mechanical locking channels along the border prevents edge peeling under dynamic shear.
- Substrate preheating—Maintaining substrate cavity temperatures at 70°C to 90°C during overmolding promotes molecular interdiffusion.
- Gate position optimization—Locating fan or tab gates on thick substrate sections distributes fill pressure evenly without washing out thin walls.
Turnkey Medical & Industrial Handheld Overmolded Enclosures
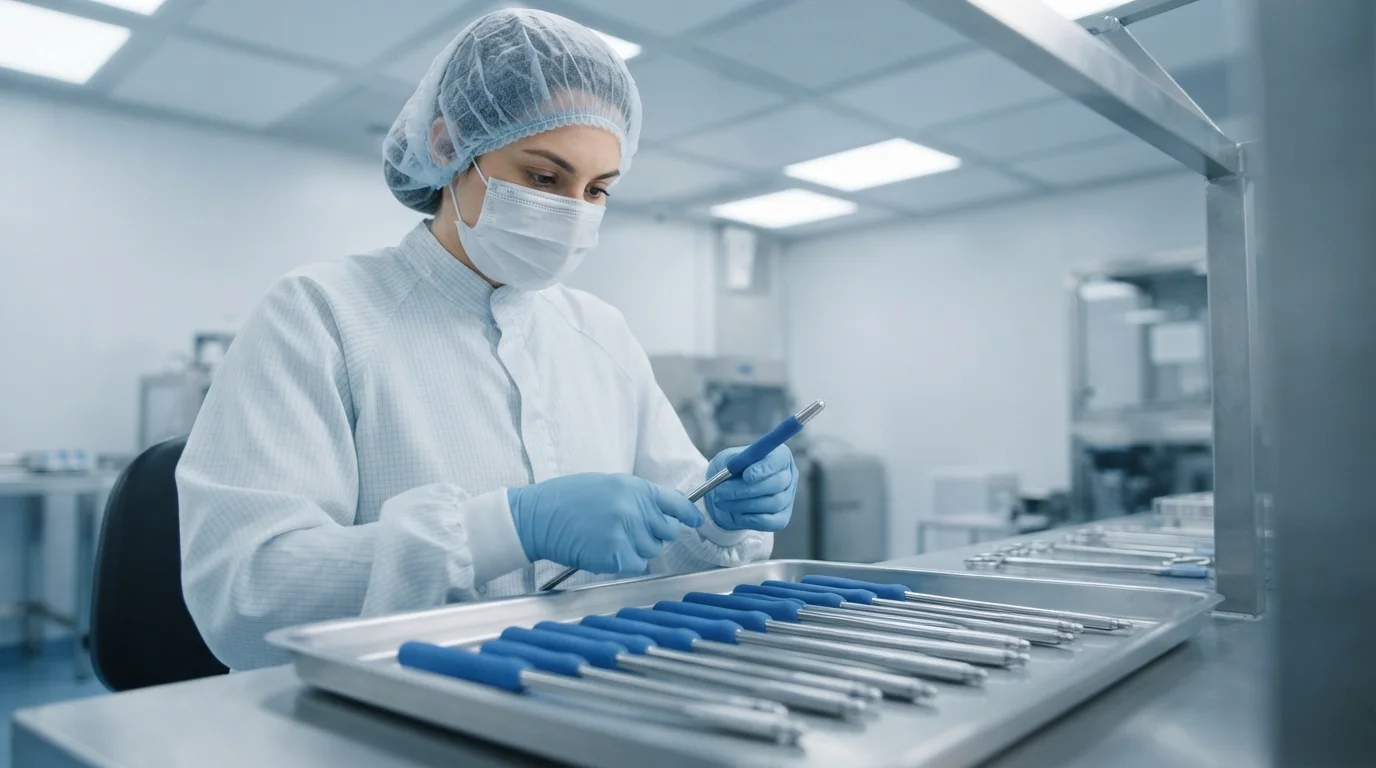
Regulated industries require certified manufacturing conditions to prevent contamination and guarantee component compliance. Operating an ISO Class 8 cleanroom molding department under ISO 13485 certification protects sterile medical devices during overmolding and automated drop-packaging. Medical applications utilize biocompatible elastomers meeting USP Class VI and ISO 10993 criteria for surgical tool handles and fluidic diagnostic housings.
Target industry overmolding solutions include:
- Medical surgical tools—ISO Class 8 cleanroom overmolding using USP Class VI TPE for slip-resistant sterilizable grips.
- Automotive key fobs and door handles—IATF 16949 certified TPU overmolding for scratch resistance and tactile comfort.
- Industrial diagnostic enclosures—Santoprene TPV overmolding over rigid PC/ABS for IP67 fluid sealing and drop shock absorption.
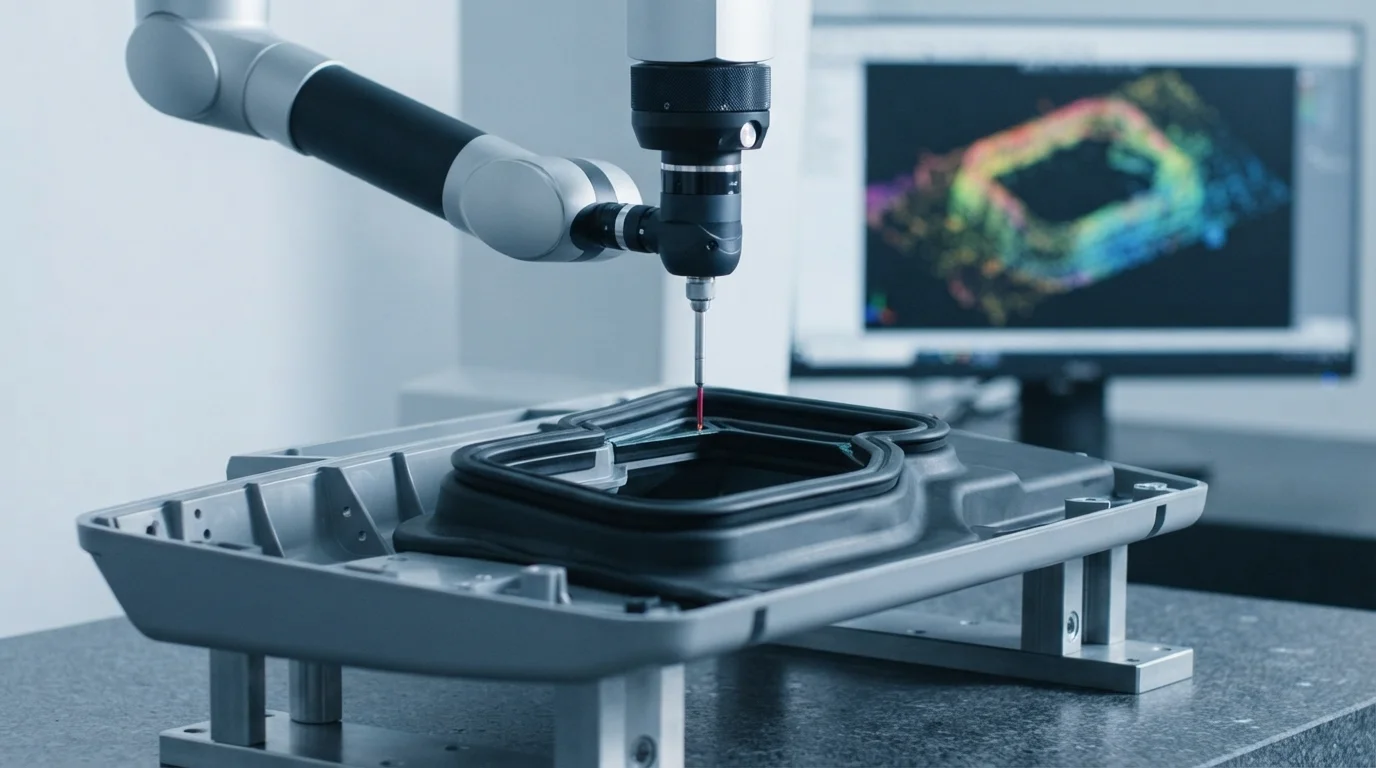
Automotive programs receive complete PPAP Level 3 documentation packages under IATF 16949 quality standards. Every production lot includes Failure Mode and Effects Analysis (FMEA), process control plans, and raw material Certificate of Analysis (COA) verification. Metrology laboratories utilize automated Zeiss CMM machines with scanning precision of ±0.003 mm to verify dimensional tolerances.
Scaling Prototyping to High-Volume Production
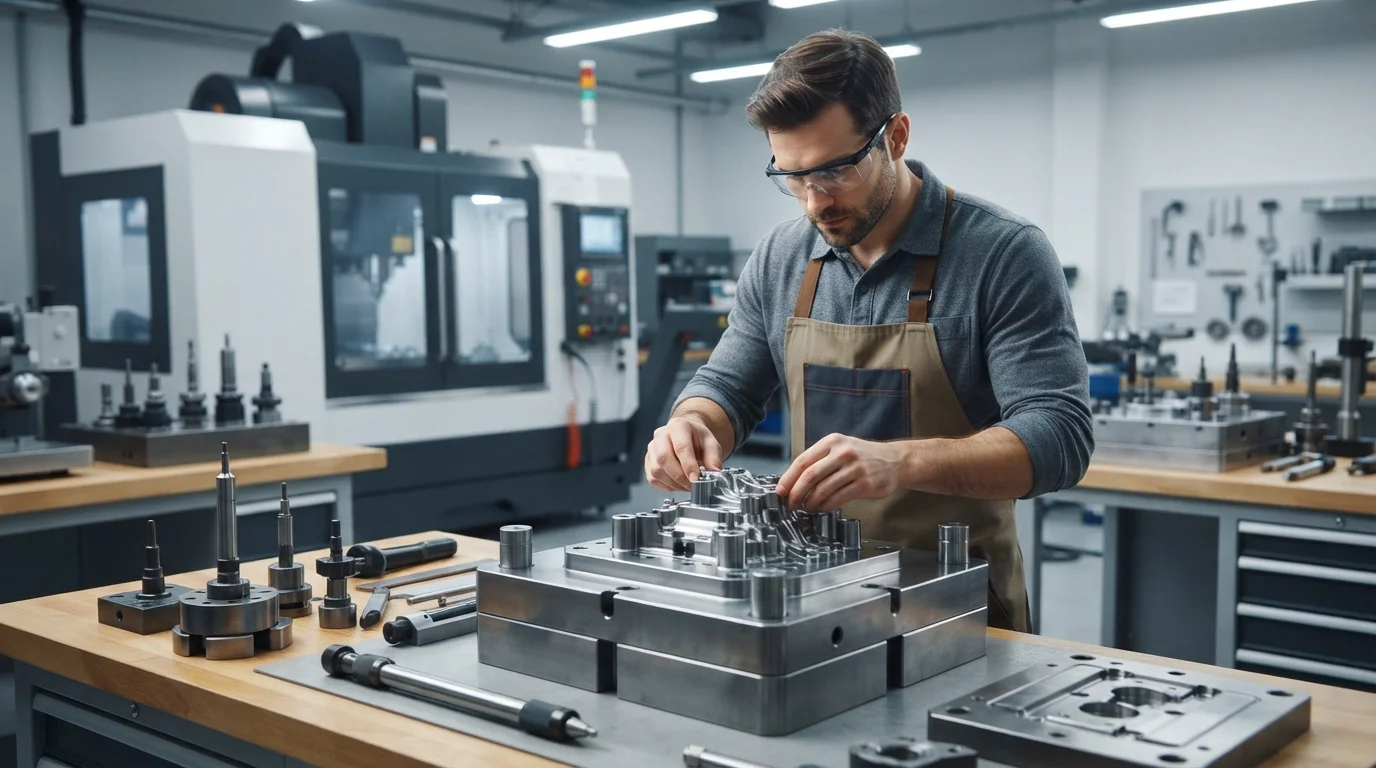
Scaling overmolding injection molding projects from initial engineering concepts to continuous high-volume production requires flexible tooling strategies. In-house tool rooms cut aluminum or pre-hardened soft steel rapid molds to deliver T1 prototype samples in as fast as 7 to 10 business days. Rapid bridge tooling permits physical drop testing and ergonomic evaluations before investing in production-grade steel tools.
Mass production utilizes fully hardened S136 stainless steel or H13 tool steel cores heat-treated to HRC 48-52. Building SPI Class 101 molds guarantees tool performance for over 1,000,000 production cycles across 35+ automated presses ranging from 15T to 3000T. Executing Decoupled Molding principles maintains process stability, achieving CpK & PpK > 1.67 on critical sealing boundaries.
Các câu hỏi thường gặp (FAQ)
How do you prevent TPE flash on overmolded parts?
Preventing flash requires maintaining shut-off steel tolerances tighter than 0.01 mm and optimizing injection holding pressure. Our tooling engineers design spring-loaded floating shut-offs that clamp firmly against the substrate during injection.
What is the difference between overmolding and two shot injection molding?
Overmolding is a two-step process where the substrate is molded first and transferred to a second mold cavity for elastomer injection. Two shot molding completes both injections inside a single machine cycle using a specialized rotary platen tool.
Which elastomer provides the best chemical adhesion to glass-filled Nylon?
Adhesion-modified TPE grades or Santoprene TPV compounds formulated specifically for polar substrates deliver the highest bond strength to glass-filled PA66. Incorporating perimeter mechanical dovetails further enhances structural peel resistance.