
Elevating plastic hardware aesthetics, tactile ergonomics, and electromagnetic performance requires comprehensive post-molding decoration and cavity surface conditioning. Standard raw molded plastic parts frequently display flow lines, parting line seams, or ejection pin marks that compromise visual quality. Applying specialized mold textures, diamond mirror polishes, conductive coatings, or multi-color pad printing transforms bare polymer parts into market-ready retail components. This technical guide reviews SPI polishing standards, VDI texturing, secondary printing methods, and EMI/RFI shielding technologies.
جدول المحتويات
SPI Mold Polishing (A-1 Mirror Finish) & VDI / Mold-Tech Texturing
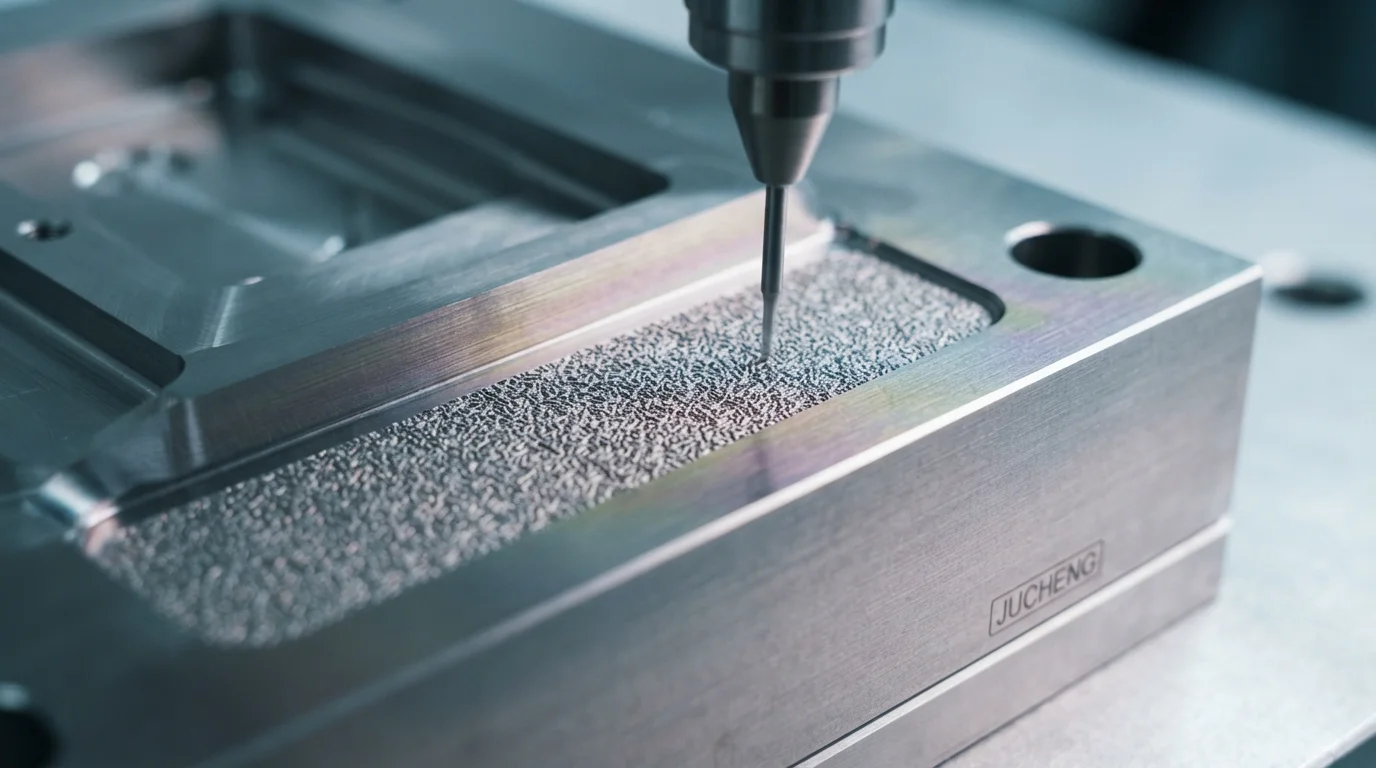
Specifying professional injection molding surface finishing begins during mold cavity toolmaking. Cavity surface preparation follows international Society of the Plastics Industry (SPI) polishing standards. Achieving an SPI A-1 mirror finish requires progressive hand-polishing using diamond paste compounds on hardened الفولاذ المقاوم للصدأ S136, eliminating micro-scratches for optical lenses and high-gloss بولي كربونات (PC) covers. Applying VDI 3400 texturing أو Mold-Tech chemical etching imparts controlled matte, leather, or geometric textures directly onto mold cavity faces. Chemical texturing masks flow lines and sink mark shadows while enhancing tactile grip on consumer electronic housings.
Mold cavity surface finishing standards include:
- SPI A-1 diamond polishing—Lapping hardened steel with 3-micron diamond paste creates a high-gloss optical mirror surface.
- VDI 3400 spark erosion texturing—Electrical discharge machining produces controlled matte micro-textures ranging from VDI 12 to VDI 36.
- Mold-Tech chemical etching—Acid etching creates complex leather, woodgrain, or geometric patterns directly on cavity steel.
- Draft angle compensation—Increasing vertical draft by 1° for every 0.025 mm of texture depth ensures clean part ejection without scuffing.
Secondary Ops: Pad Printing, Silk Screening, Laser Engraving & Painting
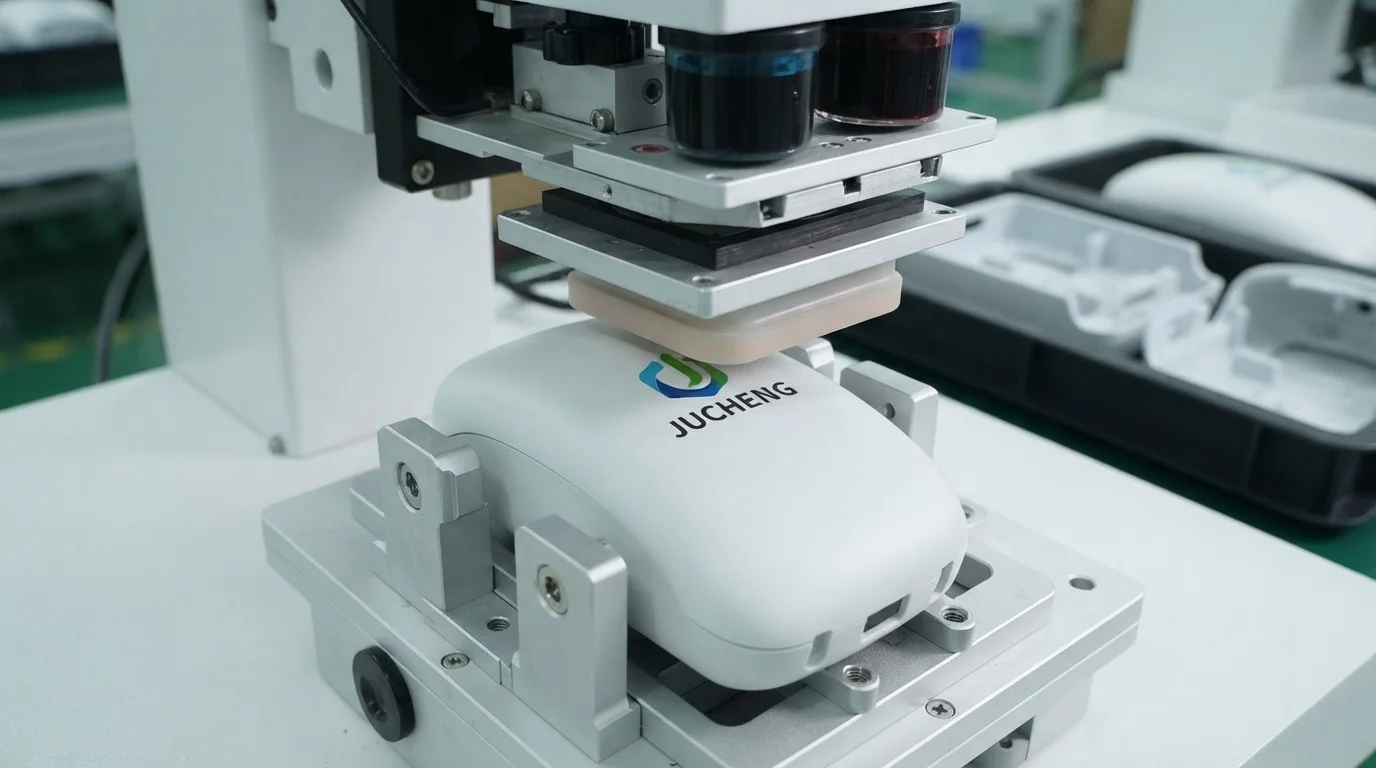
Secondary post-molding operations add functional symbols, branding logos, and protective coatings to molded ABS أو PC/ABS parts. Utilizing multi-color pad printing ينقل حبر وسادة السيليكون إلى الأسطح ثلاثية الأبعاد المعقدة والمنسوجة بسلاسة. يزيل النقش بالليزر الطلاءات السطحية على أزرار الإضاءة الخلفية، مما ينشئ رموزًا دقيقة تنقل الضوء. يعمل الطلاء السائل الآلي والطلاءات الصلبة بالأشعة فوق البنفسجية على تحسين مقاومة الخدش والمناعة الكيميائية في الزخارف الداخلية للسيارات.
طلاءات التدريع الموصلة للتوافق الكهرومغناطيسي/تداخل الترددات الراديوية للأغلفة الإلكترونية
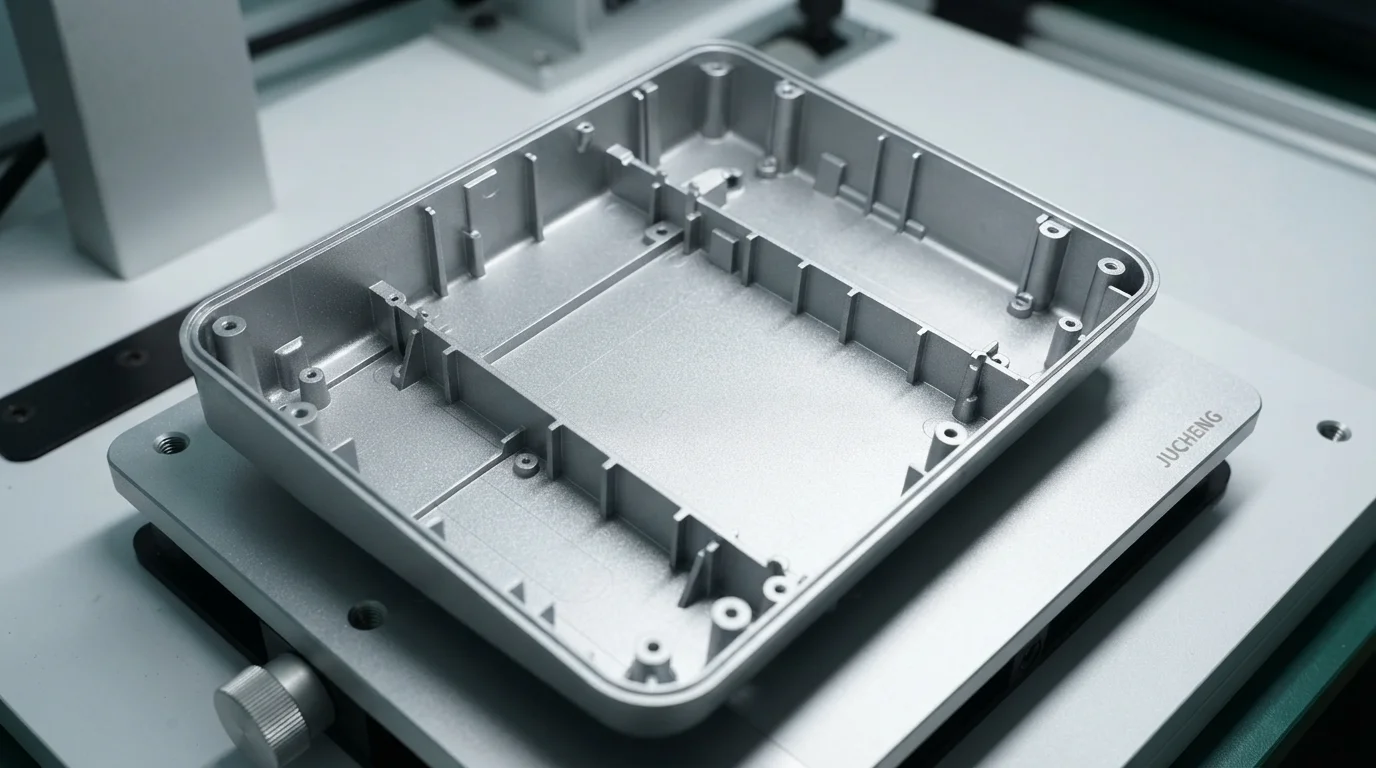
تتطلب الأغلفة الإلكترونية التي تحتوي على لوحات دوائر حساسة الحماية من التداخل الكهرومغناطيسي. إن تطبيق طلاءات التدريع EMI/RFI داخل الأغلفة البلاستيكية يمنع إشارات الترددات الراديوية الشاردة من تعطيل الإلكترونيات الداخلية. يستخدم الطلاء بالرش المتخصص تركيبات طلاء موصلة من النيكل أو النحاس أو الفضة لتشكيل حاجز تأريض مستمر. تحقيق مقاومة سطحية منخفضة أقل من 0.1 أوم/مربع يلبي لوائح التوافق الكهرومغناطيسي العالمية FCC وCE للأجهزة الطبية والفضائية.
| طريقة التشطيب السطحي | الخشونة / السماكة | الركيزة المتوافقة | الفائدة الجمالية / الوظيفية الأساسية |
|---|---|---|---|
| تلميع الماس SPI A-1 | Ra < 0.012 ميكرومتر | PC، PMMA، الراتنجات البصرية | شفافية عالية اللمعان للعدسات البصرية وموجهات الضوء |
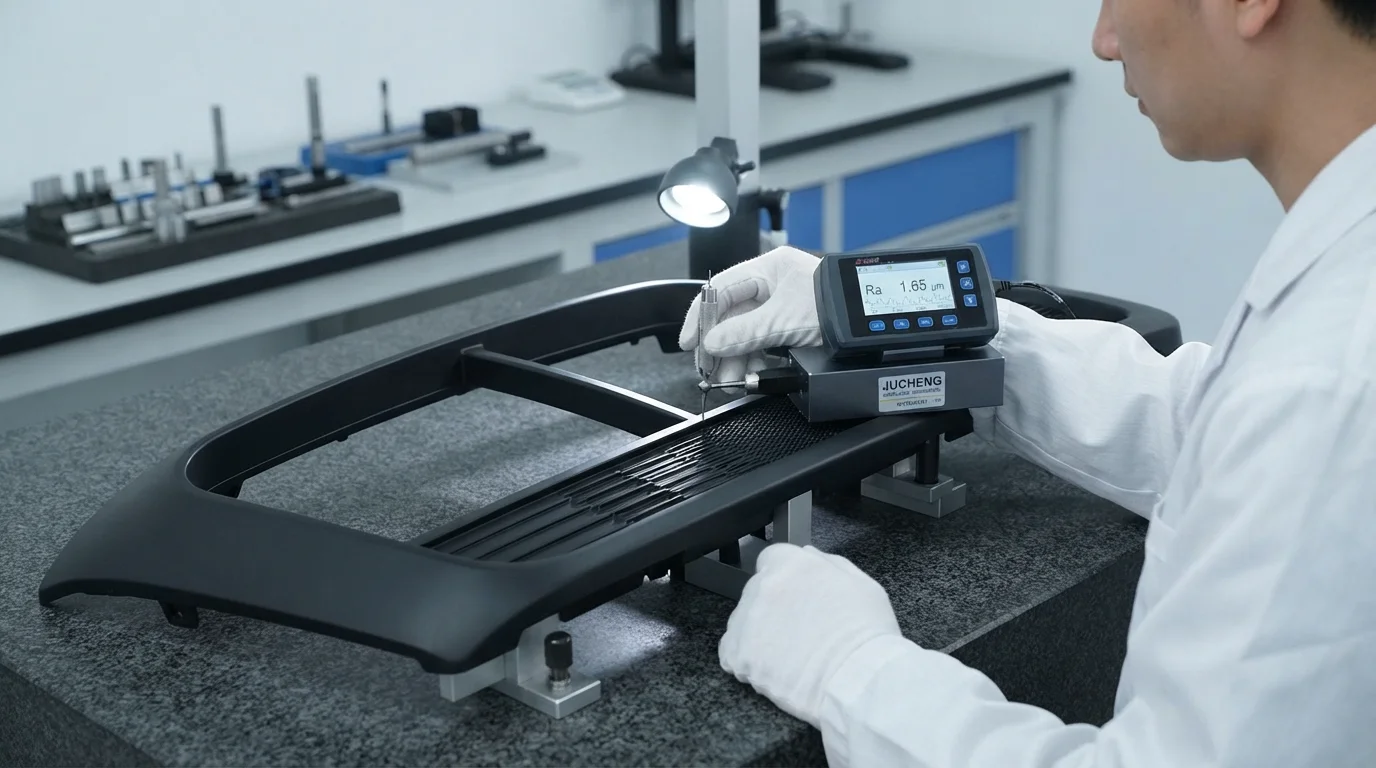
| نسيج الشرر VDI 24 | Ra = 1.6 ميكرومتر | ABS, PC/ABS, PP, PA66 | Matte tactile finish masking sink marks & scratches |
| Conductive Nickel Coating | 25 – 50 μm dry film | ABS, PC/ABS, PBT | EMI/RFI shielding (< 0.1 Ω/sq) for electronic housings |
الأسئلة الشائعة (FAQs)
What is the difference between SPI A-1 and VDI 24 surface finishes?
SPI A-1 represents an optical diamond mirror finish polished to a smooth surface roughness Ra under 0.012 microns, ideal for transparent lenses. VDI 24 is a matte spark-erosion texture produced by electrical discharge machining, offering a medium tactile grip that masks cosmetic sink marks and scratch defects on opaque enclosures.
Why do textured mold cavities require larger draft angles than polished cavities?
Textured cavity walls feature microscopic peaks and valleys that mechanically grip the shrinking plastic during cooling. Insufficient draft angles cause the plastic skin to drag against the textured steel during ejection, creating unsightly scuff marks. Adding 1° of draft for every 0.025 mm of texture depth ensures smooth release without damaging the pattern.
How do conductive spray coatings provide EMI shielding in plastic housings?
Conductive spray coatings contain microscopic nickel, copper, or silver flakes suspended in a liquid binder. When sprayed onto the internal surfaces of a plastic enclosure, the metal particles form a continuous conductive grid. This metallic layer reflects and absorbs electromagnetic radiation, preventing high-frequency noise from interfering with delicate electronic components.